







Fast Shipping
Carrier information

20k products
Payment methods

24/7 Support
Unlimited help desk

2-day Delivery
Track or off orders
Customized tool head and vacuum zoning — every corrugated sample table is configured per buyer’s flute type, ply count and sheet size rather than sold as a fixed package, validated on the actual board stock before shipment.
Technical Specifications
| Parameter | Value |
|---|---|
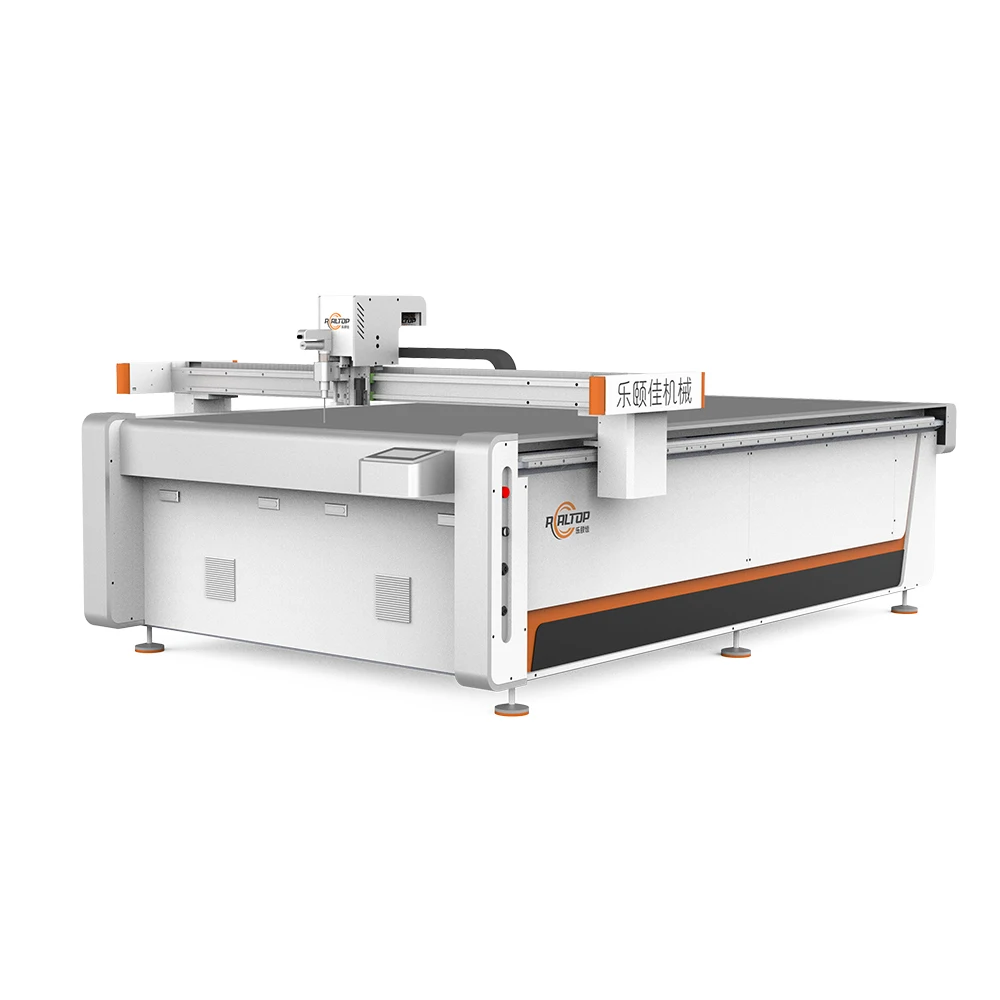
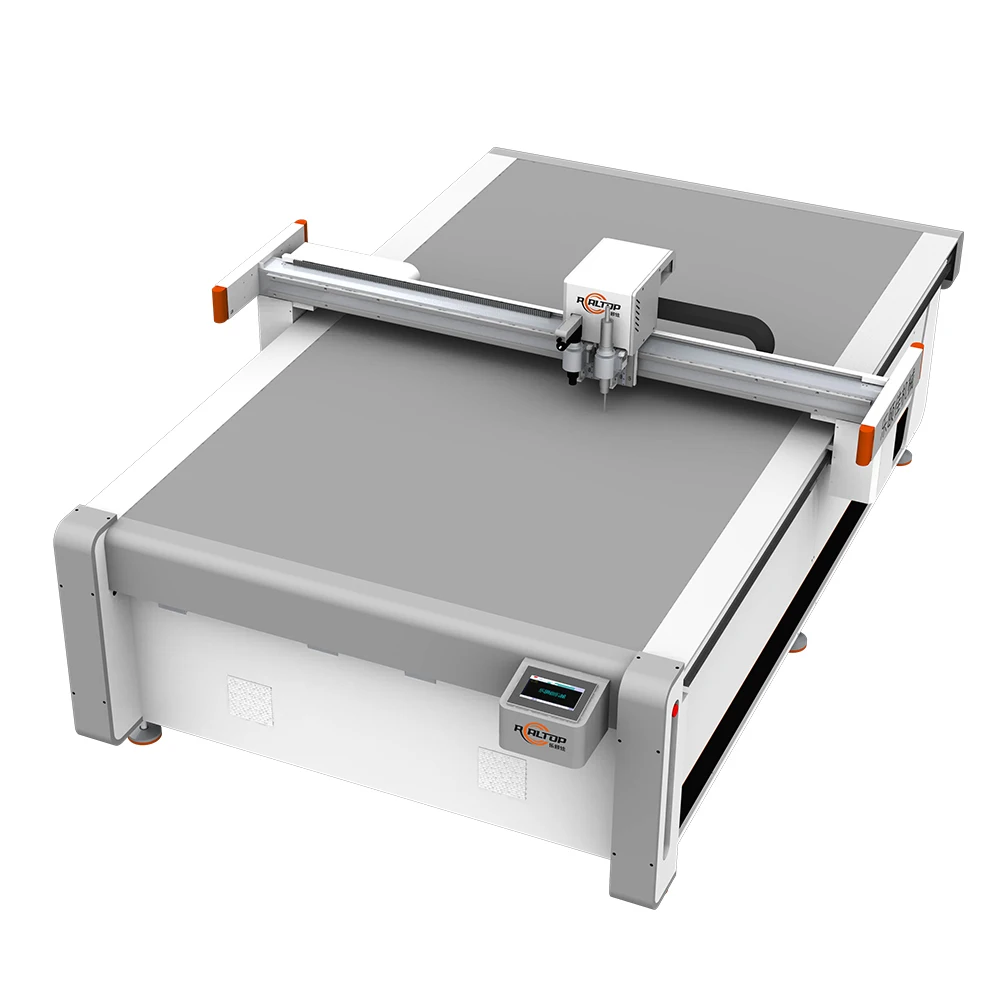
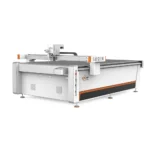
| Product Type | CNC Oscillating Knife Cutting Table |
| Working Area | 1600×2500 mm |
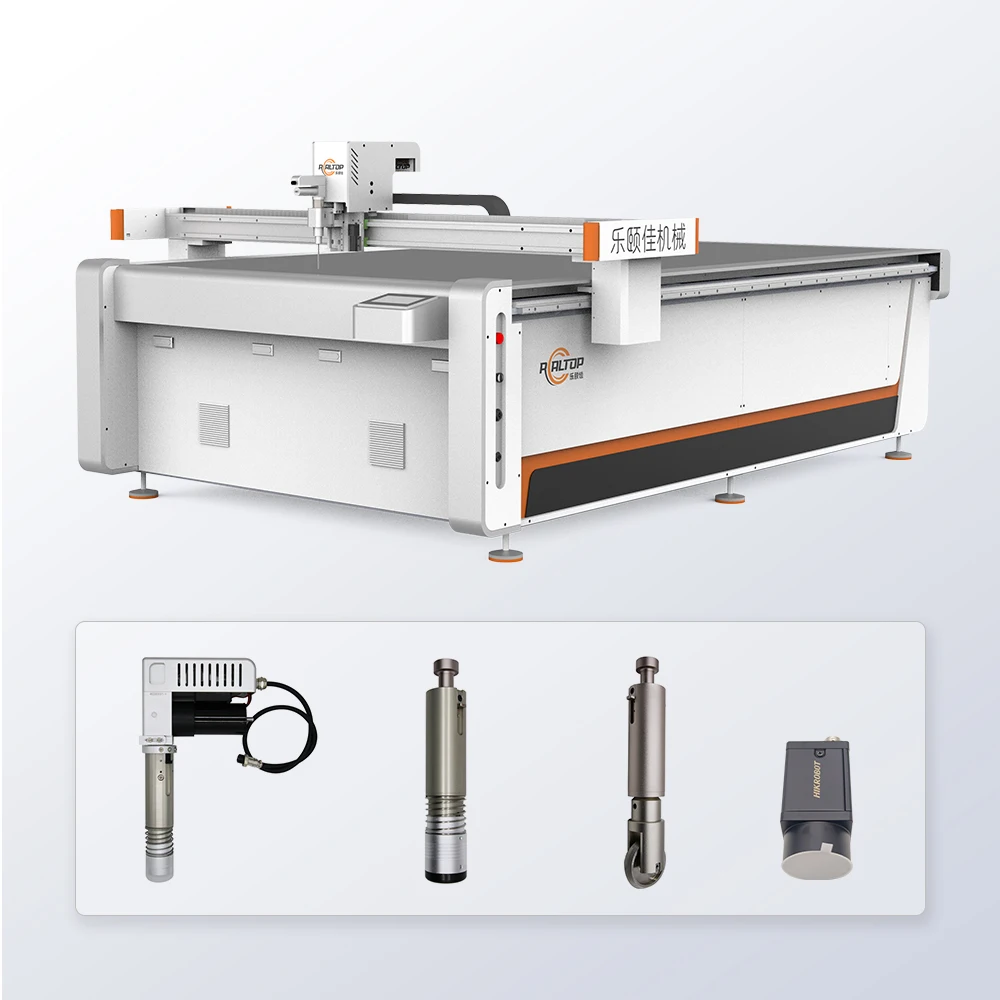
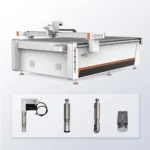
| Tool Head Options | Oscillating knife, Driven rotary knife, Creasing wheel, Kiss cutting tool, Pneumatic knife, Milling tool, V groove knife, CCD camera |
| Cutting Speed Range | 0–1500 mm/s (basis to be confirmed by material and flute type) |
| Cutting Thickness Capacity | Up to 40 mm (basis not stated in source — confirm by board grade and flute configuration) |
| Cutting Accuracy | ±0.1 mm |
| Vacuum Pump Power | 9 kW |
| Vacuum Table Surface | Aluminum bellows, full surface adsorption |
| Control System | PLC control panel with optional display languages |
| Supported File Formats | PLT, DXF, AI, PDF |
| Dedicated Software | Packaging box structure design software |
| Servo Drive Options | Panasonic, Delta, Dorna (source value — verify against manufacturer catalog) |
| Machine Dimensions (L×W×H) | 3300×2100×1350 mm |
| Machine Frame | Heavy-duty frame with precision-ground surface |
| Safety Devices | Infrared sensor device and emergency stop |
| Voltage Options | 110V / 220V / 380V (frequency to be confirmed per market) |
| Language Options | English, Russian, Italian, Chinese; special languages customizable |
| Certification | CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Corrugated board sample making | E-flute, B-flute, BC-flute corrugated cardboard for short-run prototypes without die-cut moulds |
| Carton box structure design | Greyboard, cardstock, art paper and specialty paper packaging formats |
| Protective packaging inserts | EVA foam, EPE foam, PU foam, Coroplast cushioning components |
| Gaskets and liners | Rubber mats, velvet, fleece fabric and non-woven fabric |
| Thin plastic and synthetic samples | PVC sheet, PET sheet, leather and synthetic leather packaging components |
| Composite and adhesive materials | Adhesive-backed boards and composite packaging layers |
Why Flute Thickness Matters More Than Working Area
A CNC oscillating knife cutting table for packaging sample making selected on bed size alone often fails at the first BC-flute or five-ply board run — the real constraint is the tool head and vacuum zoning matched to the actual corrugated stock.
Tool head selection and vacuum hold-down must be confirmed on the buyer’s board before commitment, not after delivery.
[NEED_CITE:] I have watched sample cutting tables that performed cleanly on standard three-layer E-flute struggle badly when the buyer switched to five-ply double-wall for heavy-duty shipping cartons. The oscillating knife pressure and cutting speed had to be re-tuned across the board, and the first month of production ran through hundreds of wasted sheets before stable parameters were found. A specification conversation that starts with working area and skips flute type almost always ends with a machine that cannot handle the real material mix in the shop [NEED_CITE: corrugated flute classification and thickness standards].
Matching the Knife to the Board, Not the Other Way Around
Corrugated cardboard is not a single material — E-flute at roughly 1.5 mm, B-flute around 3 mm, and BC-flute above 7 mm each demand a different tool head response. This CNC oscillating knife cutting table for packaging sample making carries multiple heads on the same gantry: oscillating knife for through-cuts, creasing wheel for fold lines, kiss cutting tool for adhesive layers and V groove knife for thicker boards. The configuration is specified per the buyer’s material list so the machine does not force one cutting method across incompatible stocks.
Vacuum Zoning That Holds Small Sample Parts Flat
Carton sample parts are often small and light, which means a single-zone vacuum table will lose grip at the edges during high-speed cutting. The aluminum bellows vacuum surface on this table delivers full-area adsorption rather than relying on a single central zone. For short-run packaging samples where each cut piece may differ in outline and weight, this hold-down consistency prevents lift and keeps the cutting path accurate across the entire sheet, whether the operator is running a large tray format or a small retail insert [NEED_CITE: vacuum table zoning requirements for small CNC cutting workpieces].
Reading the Specs That Actually Affect Output
The 9 kW vacuum pump paired with the aluminum bellows table is the specification that directly determines whether small corrugated sample parts stay flat during the cut — undersized vacuum on light board stock is the most common cause of ragged edges on carton prototypes. Cutting accuracy of ±0.1 mm matters most when the packaging designer expects fold lines and cut lines to register precisely against a printed layout. The PLC control panel with dedicated packaging box structure design software handles the nesting and tool path logic, and the supported PLT, DXF, AI and PDF imports need to be confirmed against the buyer’s existing design workflow before the order is placed. Language options including English, Russian, Italian and Chinese — with custom languages available — remove the operator training friction that frequently delays commissioning on export machines.
The Cost of Skipping the Sample Cut
A buyer who commits to a corrugated sample table without first running their own board through the machine typically discovers the mismatch during the first production week. Wrong creasing wheel pressure crushes the flute instead of folding it. Insufficient vacuum on small parts causes the knife to drag the sheet across the table. CCD contour recognition that works on the supplier’s test card fails to track the buyer’s own printed registration marks at production speed [NEED_CITE: CCD contour recognition performance variables on printed corrugated surfaces]. These issues are all solvable, but solving them after the machine is installed on the buyer’s floor costs far more in wasted material and downtime than a sample cutting report completed at the factory before shipment.
What Separates This Build From a Generic Cutting Table
In-house design covering knife cutting technology means the tool head configuration is selected for the buyer’s packaging material rather than pulled from a fixed catalog page. The sample cutting report on the buyer’s own corrugated stock — with flute type, ply count and thickness documented — is completed before the machine leaves the factory, not after it arrives. Software compatibility is confirmed against the buyer’s existing packaging box design files and nesting workflow so there are no surprises at first power-on. Voltage, plug type and control language are locked in during the specification stage and verified on the electrical schematic before shipment. The heavy-duty frame with precision-ground surface is built to hold alignment under continuous cutting cycles, not just at the initial commissioning [NEED_CITE: frame rigidity and long-term cutting accuracy on CNC tables].
Documentation & Verification
- Machine specification sheet listing every tool head, vacuum zone and servo option selected for your order
- Electrical schematic and voltage confirmation matched to your facility supply before dispatch
- Sample cutting report on your corrugated board stock with flute type and thickness documented
- Software licence and file format compatibility note for your packaging design workflow
- Factory test record captured before shipment with cutting parameters logged per material
Installation, Commissioning & Support
- Floor space requirement based on 3300×2100×1350 mm machine footprint with clearance for material loading
- Dedicated power circuit matching confirmed voltage option (110V, 220V or 380V) and local frequency
- Full assembly on arrival from shipped modules with vacuum table and gantry alignment check
- First-run parameter tuning on your corrugated flute types and board thickness range
- Operator training on PLC control panel with selected display language and packaging software
- Spare parts list covering oscillating knife blades, creasing wheels and vacuum table seals
What We Need to Specify Your Table Correctly
Send the corrugated board samples you actually run — flute type, ply count, thickness and any printed registration marks — so the tool head and vacuum zoning can be set before the build starts. Confirm your facility voltage and frequency, your preferred control language, and the packaging design software and file formats you currently use so the import workflow is validated before shipment.
Frequently Asked Questions
Q: How do I match the tool head to my corrugated flute type and board thickness?
A: Each flute type and ply count responds differently to knife pressure and speed. The oscillating knife handles through-cuts on most corrugated stocks, while the creasing wheel is specified separately for fold lines. The correct combination is determined by running your actual board on the machine and documenting the parameters before the order is finalized.
Q: Will the vacuum table hold small carton sample parts flat during cutting?
A: The aluminum bellows vacuum surface provides full-area adsorption rather than a single central zone, which is what keeps small and light corrugated pieces from lifting during the cut. Vacuum zoning is configured based on the smallest part in your sample mix so hold-down is consistent across the entire sheet.
Q: Can the CCD camera track printed registration marks on my corrugated samples at production speed?
A: CCD contour recognition performance depends on the print contrast, mark size and board surface of your specific stock. The camera is tested against your actual printed corrugated sheets during the sample cutting stage to confirm tracking accuracy before the machine configuration is locked in.
Q: Is the packaging design software compatible with my existing file formats?
A: The dedicated software accepts PLT, DXF, AI and PDF imports. If your current workflow uses a different format or nesting system, compatibility is confirmed during the specification stage so there are no file import issues when the machine is commissioned on your floor.
Q: How are voltage, plug type and control language confirmed before the machine ships?
A: Voltage and frequency are matched to your facility supply and recorded on the electrical schematic. Control language is selected from available options or customized. Both are verified against the specification sheet before production begins so the machine arrives ready for your electrical system and operators.


商品评价
Clear filtersThere are no reviews yet.