





Fast Shipping
Carrier information

20k products
Payment methods

24/7 Support
Unlimited help desk

2-day Delivery
Track or off orders
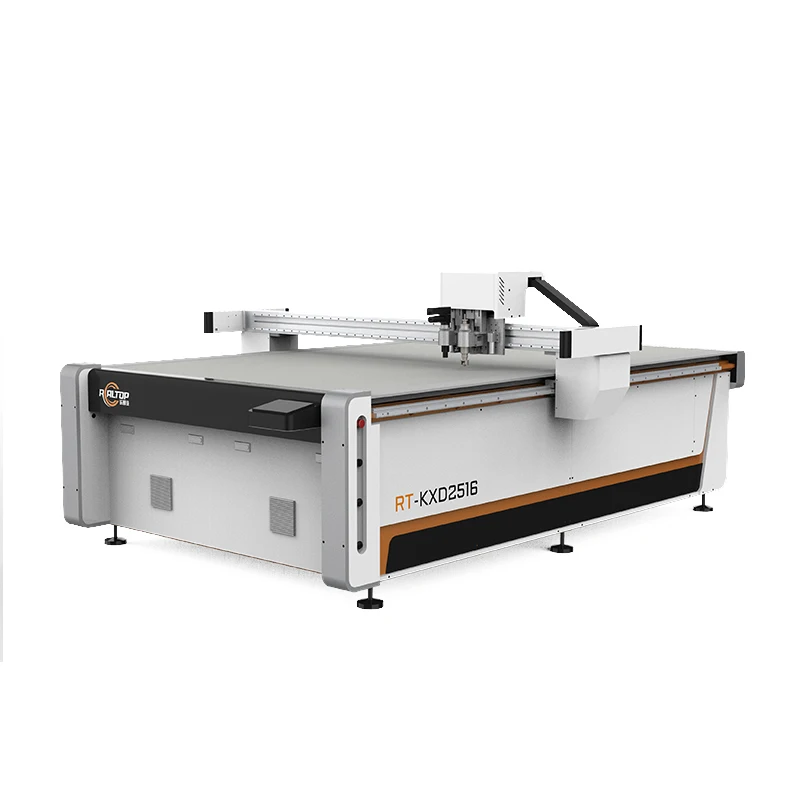
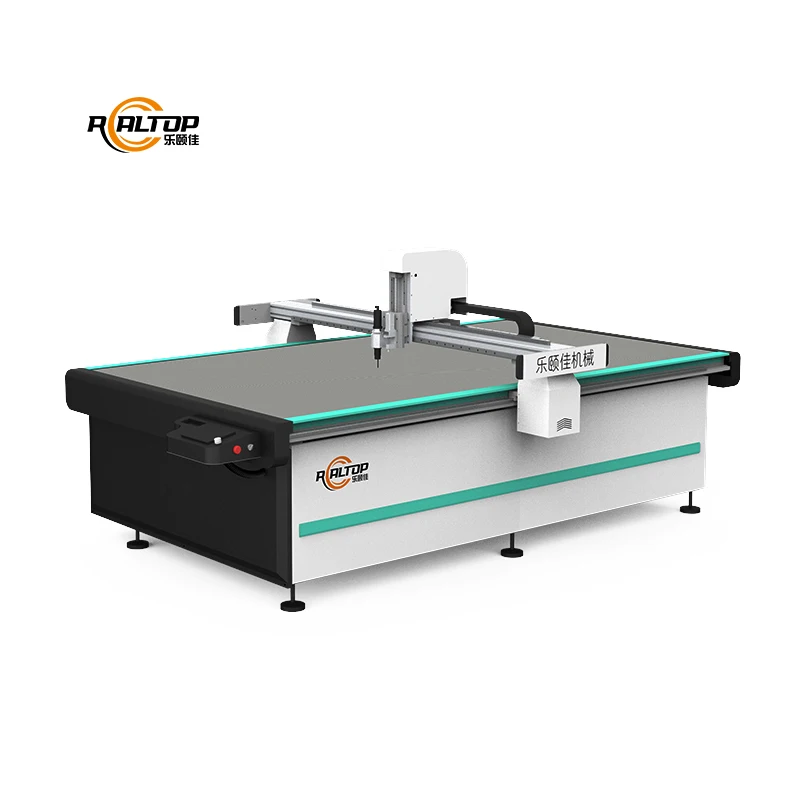
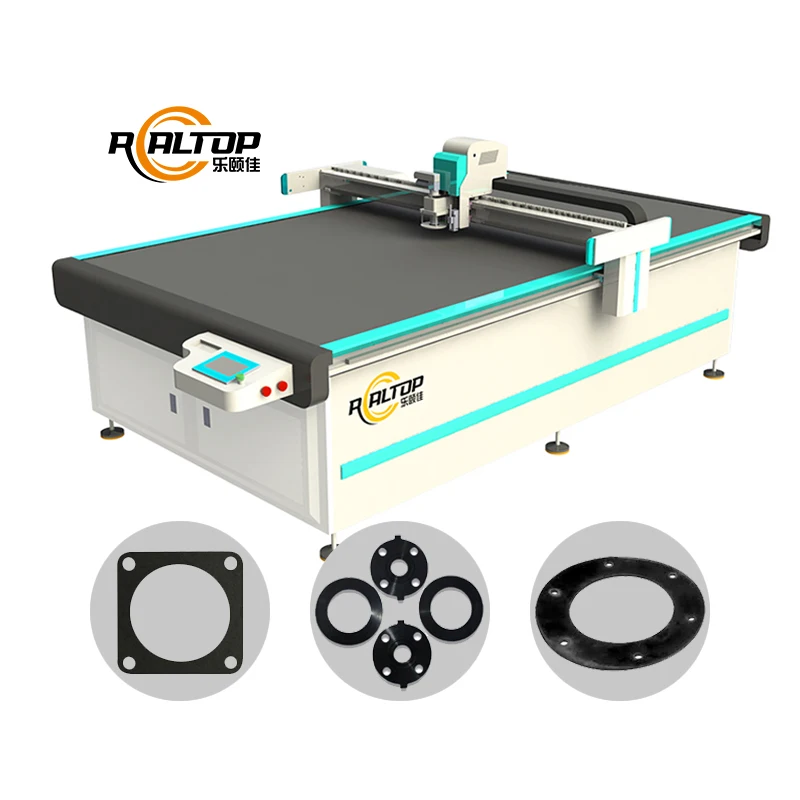
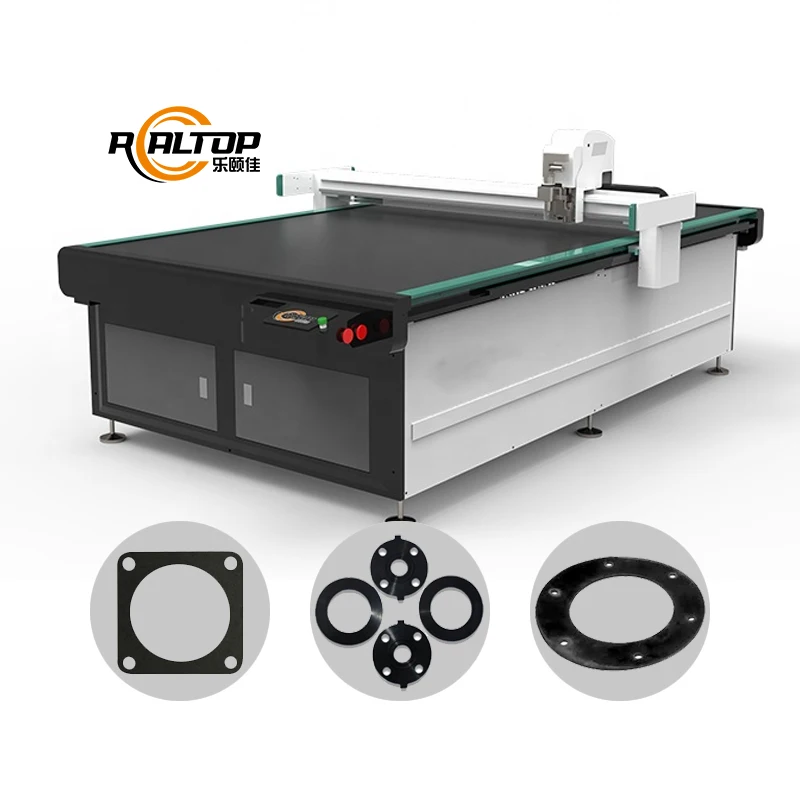
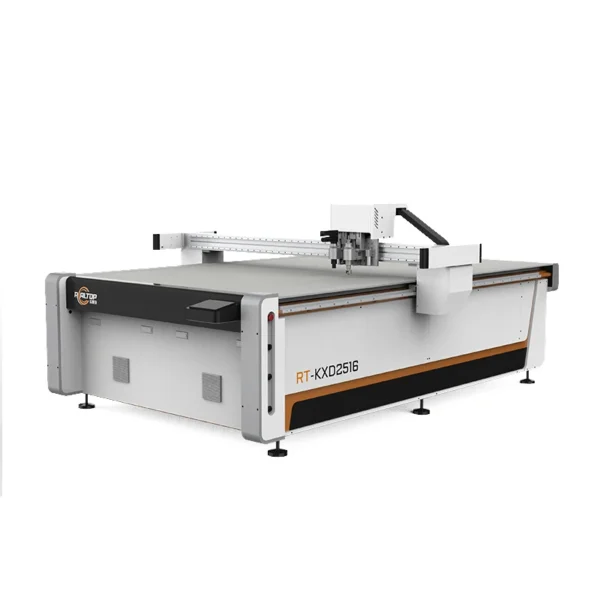
Knife over laser when the edge must stay clean — the RT-D2516/RT-S2516 oscillating knife cutting table is configured per composite thickness and part geometry, so gasket and foam producers avoid the burn marks a CO2 beam would leave on heat-sensitive laminates.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | CNC Oscillating Knife Cutting Machine |
| Model | RT-D2516/RT-S2516 |
| Working Area | 1600 × 2500 mm |
| Overall Dimensions | 3450 × 2300 × 1250 mm |
| Rated Power | 9 kW |
| Cutting Thickness | ≤100 mm (varies with material density) |
| Translational Velocity | 800–2000 mm/s |
| Cutting Speed | 200–800 mm/s (basis not stated in source — confirm material type / thickness) |
| Repeated Accuracy | ≤0.1 mm |
| Transmission System | Digital servo motor, linear guide, synchronous belt, ball screw |
| Servo Motor Brand | Delta (Panasonic available as option) |
| Linear Rail | Taiwan Hiwin |
| Vacuum Pump | 7.5 kW, integrated aviation aluminum shell with built-in silencer sponge |
| Table Type | Flat working table (magnesium-aluminum alloy with fluorocarbon PVDF coating, anodic oxidation and hard oxidation) |
| Multifunctional Tool Head | Swiss imported knife; options include oscillating knife, pneumatic knife, high-power vibrating knife, circular knife, V-cutting knife, drag knife, creasing wheel, dotted line knife, punching, brush |
| Visual Positioning | Small CCD camera mark point positioning, panoramic camera recognition, projection positioning |
| Safety Device | Infrared sensors, anti-collision, emergency stop |
| Voltage | 380V ±10% |
| Instruction System | HP-GL compatible format |
Application Suitability
| Application | Material or Output |
|---|---|
| Industrial gasket fabrication | Composite fiber sheets, cork-rubber laminates, PTFE and graphite gasket stock |
| Automotive interior trimming | Sponge composite leather, PVC soft trim, acoustic insulation foam |
| Footwear and leather goods | Natural and synthetic leather layers, multi-ply flexible uppers |
| Packaging and sample making | Corrugated board, folding carton stock, foam inserts |
| Signage and soft material display | Vinyl, flexible banner, soft glass, silicone sheets |
Why "Up to 100 mm Thick" Can Still Mean Ragged Edges
Cutting depth is only meaningful when matched to the correct tool head and material density. A CNC oscillating knife cutting machine may list a maximum thickness, but slicing 30 mm acoustic foam requires a different blade frequency and stroke than creasing 2 mm carton board. I once watched a buyer in the Gulf receive a cutter configured for leather, then try to run 15 mm EVA foam — the oscillating knife crushed the cells instead of shearing them, leaving a ragged edge that failed the automotive OEM’s visual inspection. [NEED_CITE: material-specific knife cutting parameters for composite foams]
Tool Head Selection by Material, Not by Catalog Page
The RT-D2516/RT-S2516 offers oscillating knife, pneumatic knife, drag knife, creasing wheel and punching heads within a single multifunctional carriage. Each serves a different composite behavior: oscillating for dense gasket stock where clean shearing matters, pneumatic for thick foam where downward force must exceed the material’s compression resistance, and drag knife for thin vinyl where a passive trailing blade follows the contour without lifting. Specifying by working area alone and leaving the tool head as a default is where most edge-quality failures originate.
Vacuum Zoning That Actually Holds Small Parts Flat
The magnesium-aluminum table uses multiple vacuum zones so that a 50 mm gasket blank does not lift off the surface mid-cut while a 2 m² leather hide next to it stays pinned. The fluorocarbon PVDF coating resists adhesive residue from double-sided backing tapes common in composite lamination, and the hard oxidation layer prevents the knife from scoring grooves into the table over months of production. When zones are not matched to the smallest expected part, the suction distributes across unused areas and the hold-down force drops below what the cutting head’s lateral drag demands. [NEED_CITE: vacuum hold-down force requirements for oscillating knife cutting]
Reading the Specs That Actually Move the Needle
Repeated accuracy of ≤0.1 mm matters in gasket work because a bolt-hole pattern that drifts 0.3 mm across a 1600 mm cut length will not align at assembly. The Hiwin linear rail and ball screw transmission provide that repeatability across the full 1600 × 2500 mm bed, whereas belt-only drives on machines of this size tend to accumulate backlash after a few thousand hours. The 7.5 kW vacuum pump with an integrated silencer sponge keeps noise below what would otherwise require a separate pump room — a detail that matters when the machine sits inside a garment or footwear workshop rather than an isolated fabrication bay. Servo motor choice between Delta and Panasonic typically comes down to local service availability; a Panasonic servo is easier to replace in Southeast Asia, while Delta parts are stocked more widely in the Middle East.
The Hidden Cost of Skipping the Sample Cut
A buyer who signs off on a quotation without running their own material through the machine will discover three problems only after the crate is opened: the oscillating knife frequency may be too low for their specific foam density, the CCD camera may fail to read their printer’s registration mark color at production speed, and the nesting software may not import the DXF layer structure their design team already uses. Every one of these is fixable before shipment — but each one adds weeks when caught after delivery. [NEED_CITE: pre-shipment sample cutting verification for CNC knife cutters]
Why Buyers Specify Here Instead of a Trading Company
In-house knife and table design means the tool head configuration is not a catalog pick but an engineered match to the buyer’s material stack. Voltage is confirmed in writing before production starts — I have seen a 380V machine arrive at a 415V site and sit idle for a month while a transformer crossed the ocean. Software compatibility is checked against the buyer’s existing nesting workflow so that HP-GL files import without manual layer re-mapping. Factory testing runs the buyer’s actual sample material, not a generic demo sheet, so cutting speed and edge quality are documented before the machine is crated. CCD camera model and vacuum zone count are listed on the configuration sheet the buyer signs, not left to the assembler’s discretion.
Documentation & Verification
- Machine specification sheet listing confirmed tool head, vacuum zone count and CCD camera model
- Electrical schematic with voltage and frequency matched to buyer’s site supply
- Sample cutting report on buyer’s own composite material showing edge quality and achieved speed
- Software licence note with HP-GL import compatibility and nesting file format confirmation
- Factory test record with dimensional check on buyer’s sample part before crating
- Operation and maintenance manual in the buyer’s specified control language
Installation, Commissioning & Support
- Flat concrete floor required; 3450 × 2300 mm footprint plus operator clearance on three sides
- Dedicated 380V ±10% three-phase circuit with minimum 15 A breaker for the 9 kW rated draw
- Machine ships as single skid; vacuum pump is pre-mounted, only power and extraction connections on site
- First-run commissioning includes vacuum zone mapping and CCD mark recognition calibration on buyer’s material
- Spare oscillating knife blades, drag knife tips and vacuum seals shipped in the initial kit
What to Include in Your Inquiry
Send the material type, maximum thickness and the smallest part dimension in your nesting layout. Confirm your workshop’s voltage and frequency — written, not assumed from the country name. If you already run nesting software, attach a sample file so we can verify layer import before quotation.
Frequently Asked Questions
Q: Which tool head should I choose for composite gasket material versus EVA foam?
A: Oscillating knife suits dense gasket stock where a clean shear is required; pneumatic knife handles thick, compressible foam by adding downward force to prevent cell crushing. Both can be mounted on the same multifunctional head of the RT-D2516/RT-S2516, allowing one machine to cover both material families without a separate purchase.
Q: Will the CCD camera reliably track my printed marks at full cutting speed?
A: Tracking reliability depends on mark contrast, size and color — not just camera resolution. The panoramic and small CCD options on this machine handle most standard registration marks, but we confirm performance by running your printed sheet during the sample cut before shipment, adjusting exposure and mark format if needed.
Q: Is the vacuum table zoning adequate for very small gasket blanks?
A: The table is divided into multiple independently controlled zones. For parts as small as 50 mm, only the zone directly beneath the blank is activated, concentrating suction where it is needed. Zone layout is confirmed during the sample cut to match your specific nesting pattern.
Q: Can my existing nesting software output files this machine will accept directly?
A: The control system accepts HP-GL compatible formats and common DXF layers. We test your actual nesting file during pre-shipment verification and document any required layer or setting adjustments in the software compatibility note, so your design workflow continues uninterrupted.
Q: How is the correct voltage confirmed before the machine leaves the factory?
A: We require a written voltage and frequency declaration signed by the buyer — not a country lookup. The electrical schematic is then produced to match, and the matching is recorded on the machine specification sheet and the factory test record before crating.


商品评价
Clear filtersThere are no reviews yet.