

Fast Shipping
Carrier information

20k products
Payment methods

24/7 Support
Unlimited help desk

2-day Delivery
Track or off orders
Matched Tooling to Material — The RT-D2516/RT-S2516 configuration is locked only after your actual board stock, thickness and cut profile have been sampled on the factory floor.
Technical Specifications
| Parameter | Value |
|---|---|
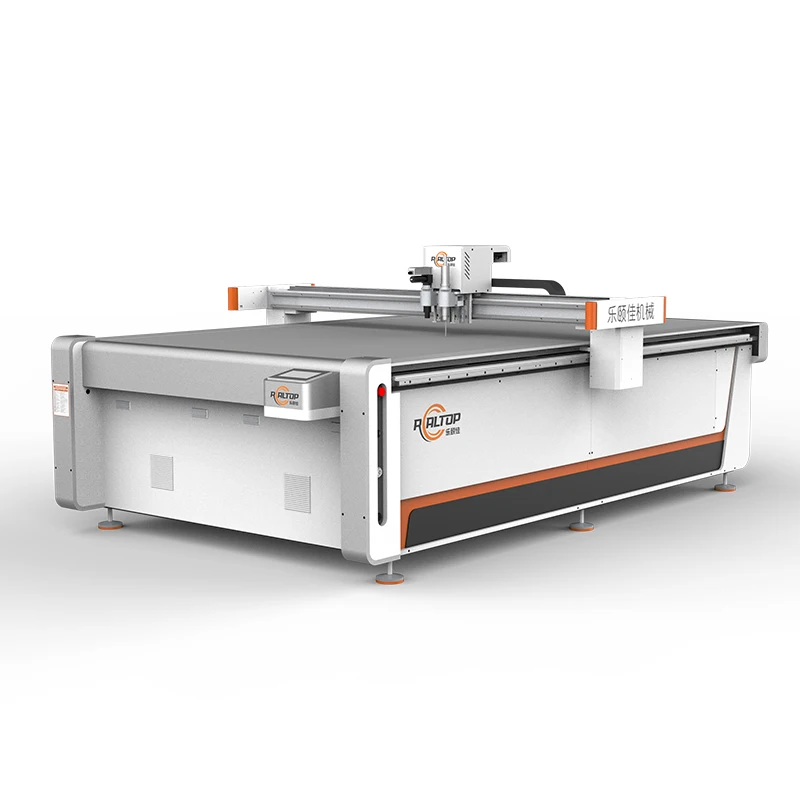
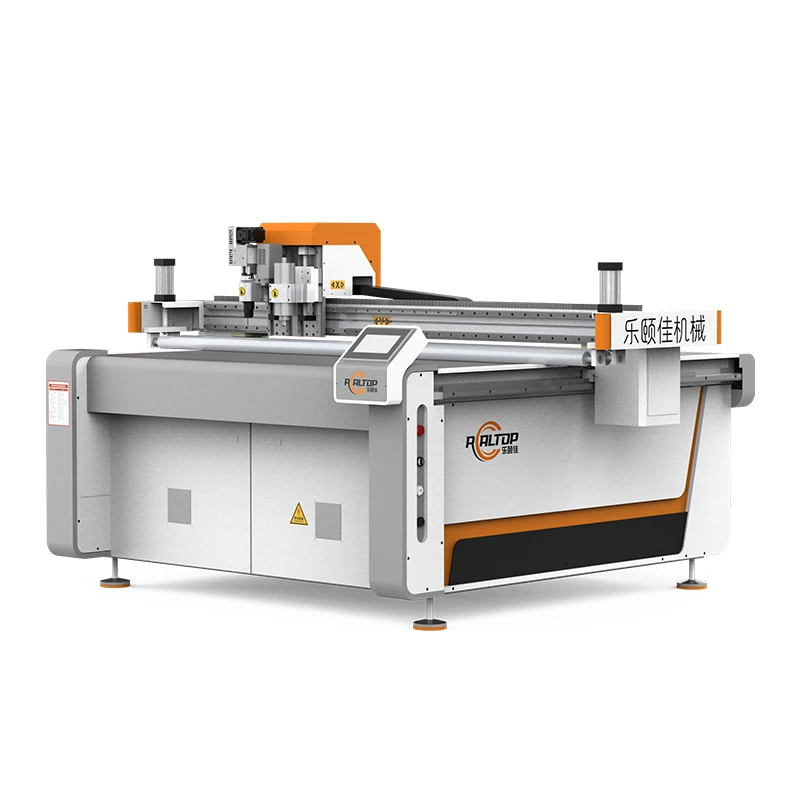
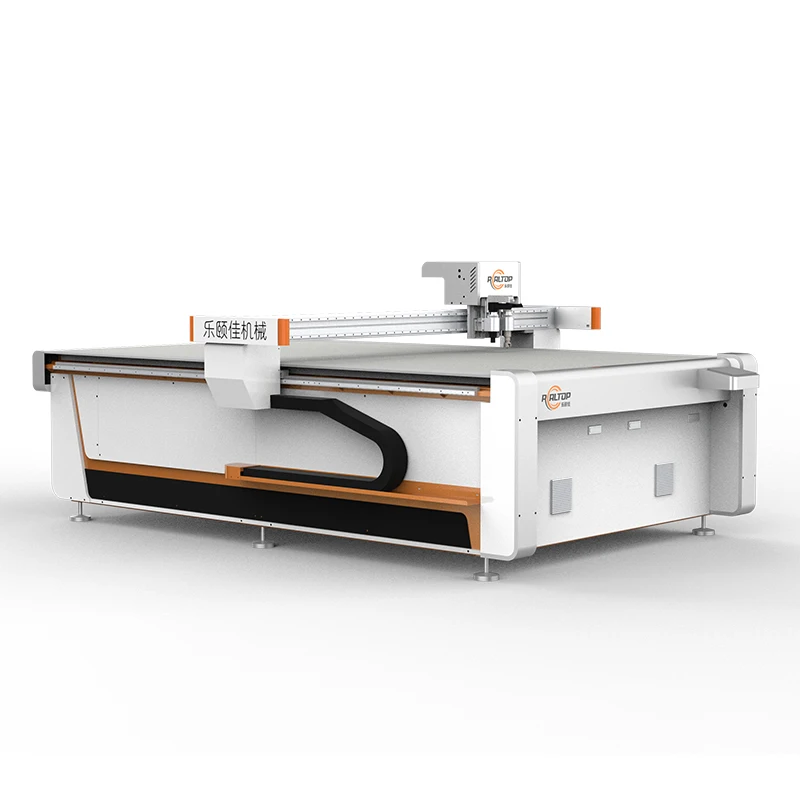
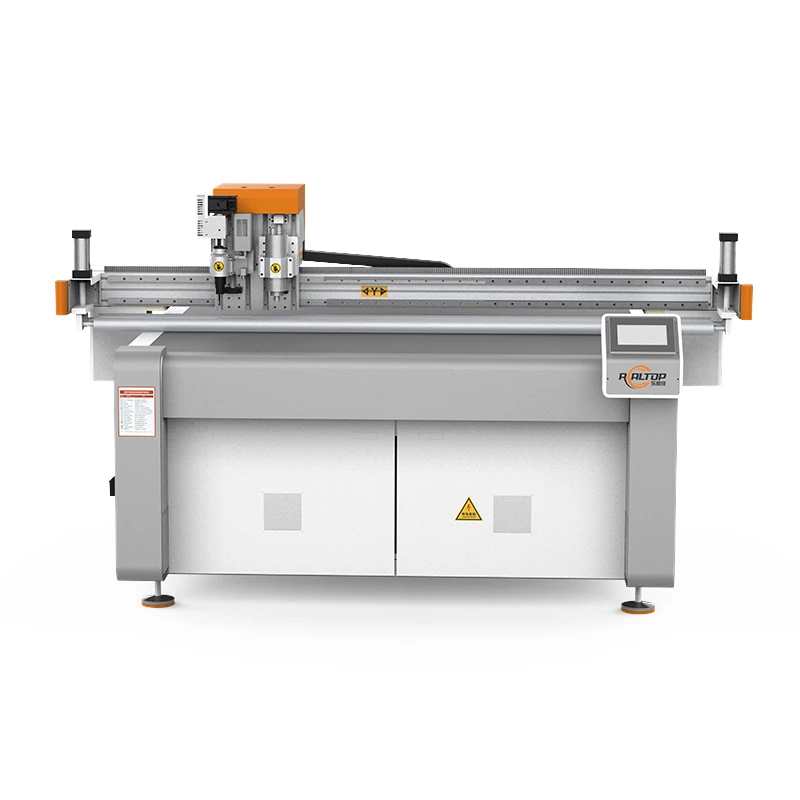
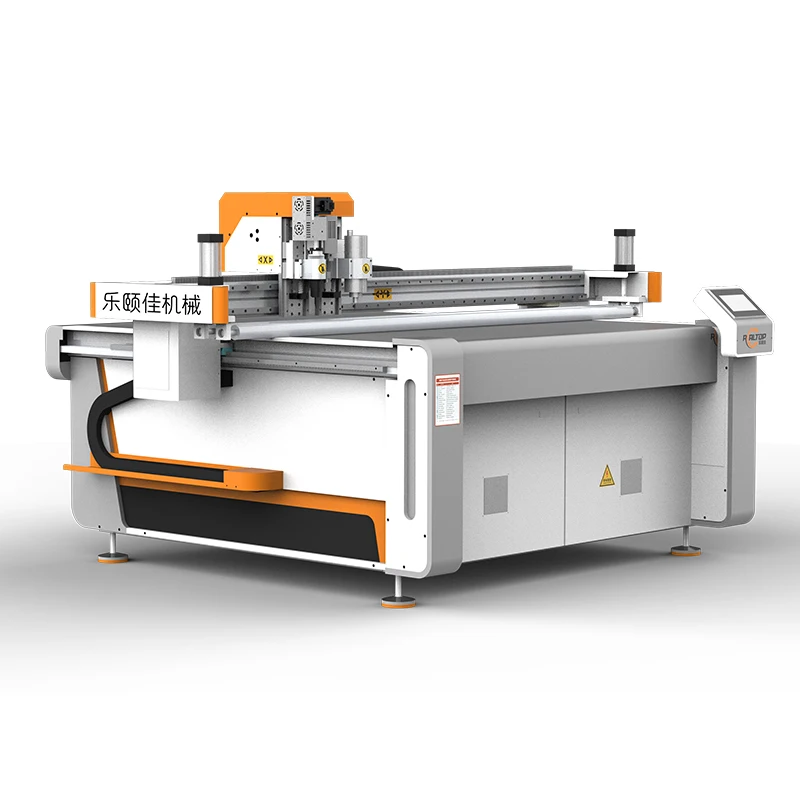
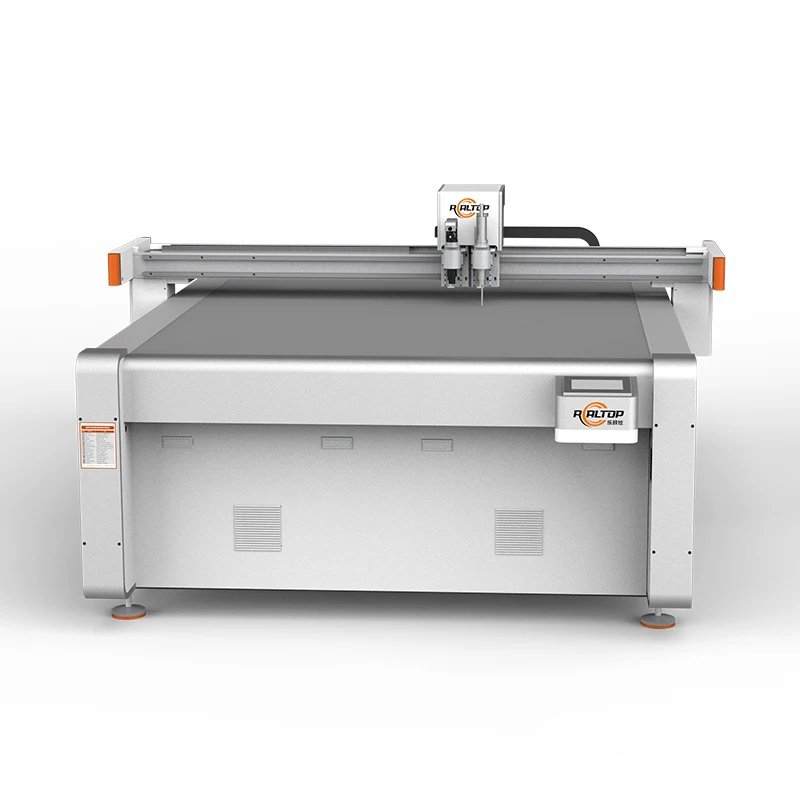
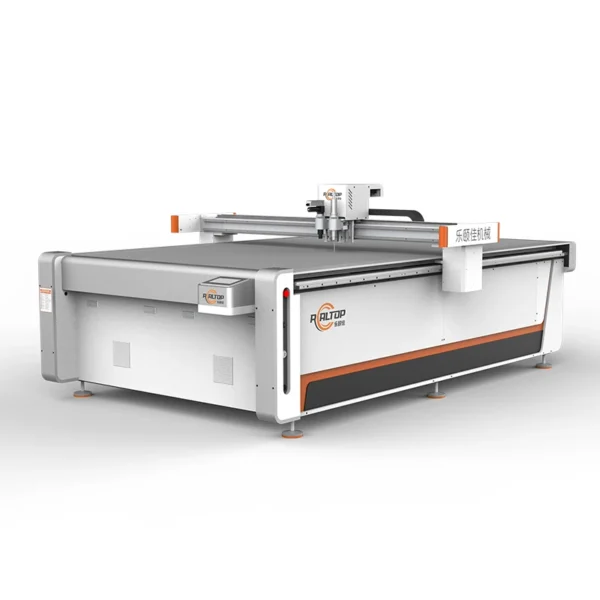
| Product Type | CNC Oscillating Knife Cutting Machine |
| Model | RT-D2516/RT-S2516 |
| Working Area | 1600 × 2500 mm |
| Overall Dimensions | 3450 × 2300 × 1250 mm |
| Rated Power | 9 kW |
| Voltage | 380 V ±10 % (frequency to be confirmed by destination market) |
| Control System | CNC, HP-GL compatible format |
| Tool Head Type | Swiss imported oscillating knife (full cut, half cut, cursor location) |
| Translational Velocity | 800 – 2000 mm/s |
| Cutting Speed | 200 – 800 mm/s (basis not stated in source — confirm material and thickness) |
| Cutting Thickness | Up to 100 mm depending on material density (basis to be confirmed on sample) |
| Repeated Accuracy | ≤ 0.1 mm |
| Transmission System | Digital servo motor, linear guide, synchronous belt, ball screw |
| Servo Motor & Driver | Taiwan Delta |
| Guide Rail | Taiwan Hiwin |
| Vacuum Table | Aluminum alloy honeycomb structure, 7.5 kW vacuum pump |
| Conveyor Belt | Germany imported auto-feeding belt |
| Safety Device | Infrared sensors, emergency stop |
| Software | Professional carton nesting, multiple file import, custom language |
| Language Options | English, Russian, Italian, Chinese, special languages customizable |
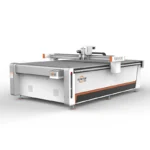
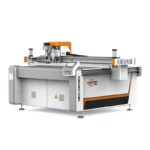
| Assembly State | Fully assembled flatbed cutting table |
| Certification | CE declaration where applicable |
Application Suitability
| Application | Material or Output |
|---|---|
| Packaging carton and cardboard sample making | Corrugated board, greyboard, folding carton stock, white card |
| Express paper box and gift box packaging | E-flute, B-flute, coated and uncoated paperboard |
| Sticker and label contour cutting | Self-adhesive vinyl, PVC sticker sheets, label rolls |
| Advertising signage and billboard production | PVC foam board, KT board, corrugated plastic, printed vinyl |
| Flexible material cutting for garment and leather goods | Leather, sponge composite leather, silicon, rubber sheets |
| Foam and gasket fabrication | EVA foam, closed-cell sponge, rubber gasket stock |
Why "Up to 100 mm" Means Nothing Until Your Stock Is on the Table
Cutting depth is verified per material, not quoted as a headline number.
I have watched buyers sign off on a machine after watching it slice cleanly through a standard PVC display board, only to find the same head struggling through EVA packaging inserts at their own shop. The density, rebound and tear behaviour of foamed stock change everything — blade angle, oscillation frequency, pass count and vacuum hold-down all shift. That is why the stated CNC Oscillating Knife Cutting Machine specifications only become meaningful once your exact board type, flute profile or foam density has been test-cut and the report signed off [NEED_CITE: material density and rebound effect on oscillating knife penetration].
Oscillating Knife Behaviour Across Packaging Stocks
The Swiss imported oscillating head on this CNC Oscillating Knife Cutting Machine delivers full cut, half cut and cursor location from a single tool station. On dense greyboard the blade must penetrate cleanly without dragging fibres, while on E-flute corrugated the priority is crushing the flute edge as little as possible so the fold line stays sharp. Switching between these jobs means adjusting stroke length and frequency through the CNC control rather than changing tooling, which keeps changeover fast for mixed short-run sample work.
Vacuum Zoning and Small Die-Cut Parts
The aluminum alloy honeycomb table coupled with a 7.5 kW pump gives uniform suction across the 1600 × 2500 mm surface. For packaging sample makers cutting intricate inlays or small window-patch apertures, the zoning layout must hold parts down even after the knife has released them. If the zone grid is too coarse, lightweight sticker stock or thin PVC lifts at the trailing edge and the cut path drifts [NEED_CITE: vacuum zoning pitch requirements for small die-cut components].
Reading the Drive Train Against Repeatability Claims
Taiwan Delta servo motors running on Taiwan Hiwin linear guides are specified to hold ≤ 0.1 mm repeat accuracy. On packaging sample work that matters most when a crease line must land exactly on a pre-printed fold mark, or when a half-cut kiss score has to leave just enough liner intact for the label to peel cleanly. The ball screw and synchronous belt combination keeps backlash predictable over long cutting cycles, so the hundredth box blank matches the first.
What Happens When the Wrong Head Meets the Wrong Board
A drag knife on corrugated board leaves a ragged edge and tears the top liner; an oscillating head on thin self-adhesive vinyl can chatter and leave micro-tears that show up under lamination. Selecting the tool station is a material decision, not a price decision, and getting it wrong means re-running jobs, wasting stock and losing client confidence on delivery day [NEED_CITE: tool head and material mismatch consequences in digital finishing].
Why Buyers Source This Configuration Here
In-house design covers both knife and laser cutting, so the cutting method is chosen to suit the stock rather than forcing every job through one technology. The tool head and table layout are specified against your actual production volume and board range, not sold as a default package. CCD camera positioning, software file compatibility, voltage and language are confirmed on paper before the build starts. Your own material is sample-cut and the report shared before you commit, so edge quality and cycle behaviour are documented, not promised.
Documentation & Verification
- Electrical schematic confirming 380 V ±10 % and destination frequency before build
- Tool head and vacuum zone configuration list matched to your board range
- Sample cutting report on your corrugated, greyboard or foam stock with edge photos
- Software licence note listing supported file formats and nesting compatibility
- Spare parts list covering blades, creasing wheels and conveyor belt sections
- Packing photographs showing table level and protective crating before dispatch
Installation, Commissioning & Support
- 3450 × 2300 mm footprint requires level concrete floor with clearance for conveyor feed
- Dedicated 380 V circuit sized for 9 kW rated load plus vacuum pump inrush current
- Fully assembled flatbed arrives bolted to crate; table re-levelled on site before power-up
- First-run parameter tuning performed on your actual board stock and thickness range
- Operator training covers HP-GL file import, tool offset setting and vacuum zone selection
- Wear parts kit includes oscillating blades, creasing wheels and belt tensioning tools
What to Send With Your Enquiry
Share the exact board grades, flute profiles or foam densities you run, along with sheet size and typical nest layout. Tell us your workshop voltage and frequency, preferred control language, and whether your existing design files come from ArtiosCAD, AutoCAD or another source. If your jobs include printed contour work, send a sample sheet so camera tracking can be validated at your target feed rate before the machine is configured.
Frequently Asked Questions
Q: How is cutting thickness verified for my specific material and what is the maximum the RT-D2516/RT-S2516 can handle?
A: Maximum penetration is quoted at 100 mm, but real depth depends on material density and rebound. Before order we cut your actual board or foam sample, measure edge quality and pass count, and record the result in a signed sample report so you know the machine handles your stock.
Q: Which tool head configuration matches my board stock and cut profile?
A: Corrugated and greyboard sample work typically uses the oscillating knife for through cuts and a creasing wheel for fold lines. Thin vinyl and sticker contour jobs may need a drag knife or kiss-cut setting. We recommend the tool station mix after reviewing your cut files and running sample pieces.
Q: What voltage, frequency and control language options are confirmed before shipment?
A: The standard electrical supply is 380 V ±10 %, but frequency and plug type depend on your local grid. Control language is selectable from English, Russian, Italian, Chinese or a custom option. All three are locked on the electrical schematic before the build begins.
Q: Can the vacuum table zoning be configured for small die-cut parts without material lift?
A: The honeycomb table with its 7.5 kW pump is divided into selectable zones. We map the zone layout against your smallest part footprint so suction holds edges down even after the knife releases the cut, preventing drift on lightweight sticker and thin PVC stocks.
Q: How is the CCD camera contour recognition validated at my production speed with my printed marks?
A: We run your printed sheet through the camera system at the intended feed rate, checking mark detection, offset calculation and path correction across the full 1600 × 2500 mm bed. Results are documented in the sample cutting report so you see registration accuracy before committing to the build.


商品评价
Clear filtersThere are no reviews yet.