



Fast Shipping
Carrier information

20k products
Payment methods

24/7 Support
Unlimited help desk

2-day Delivery
Track or off orders
Technical Specifications
| Parameter | Value |
|---|---|
| Model | RT-D2516/RT-S2516 |
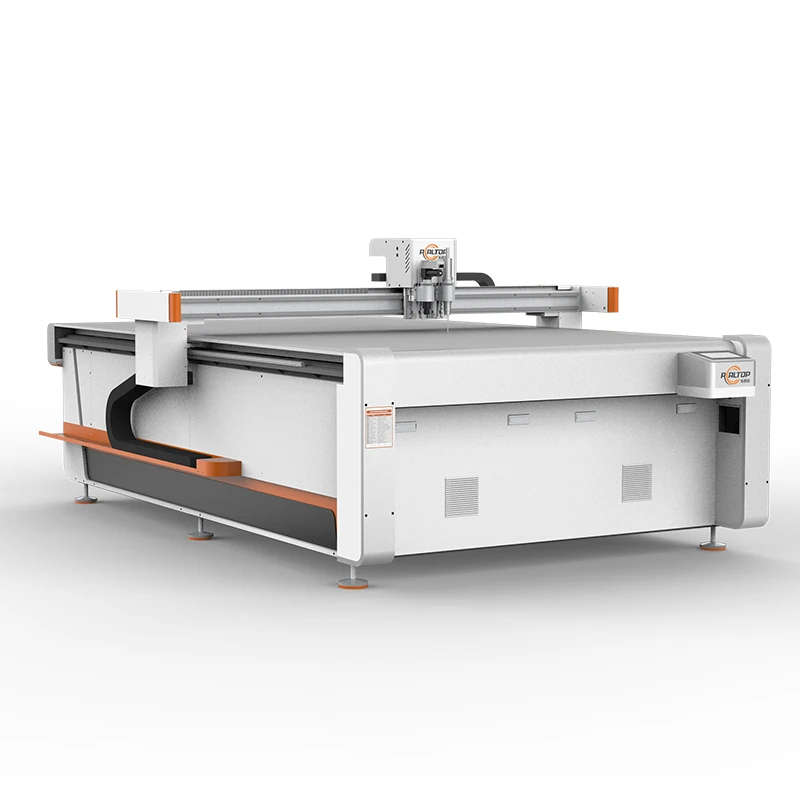
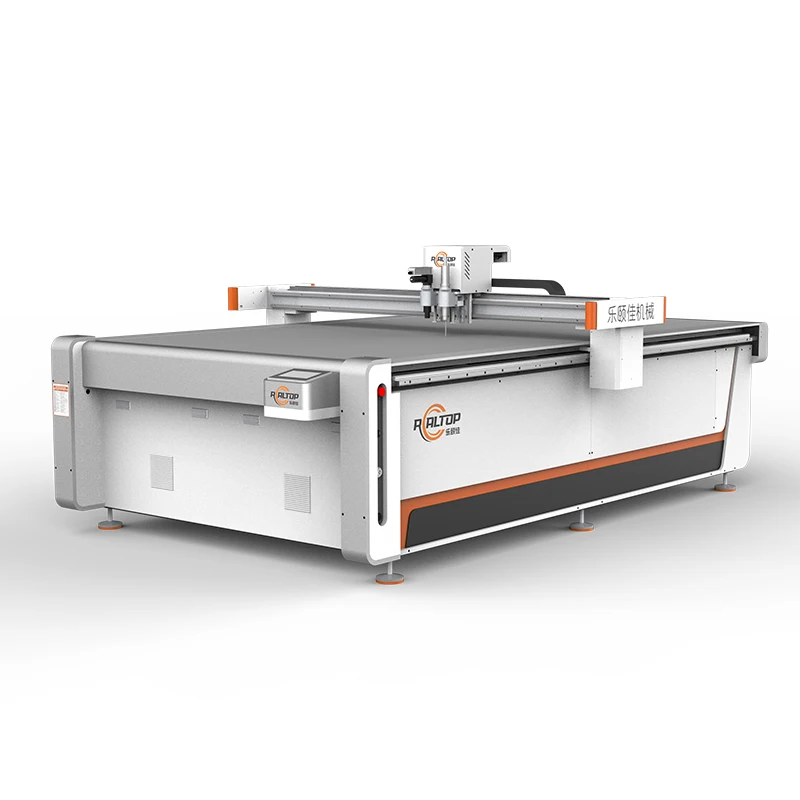
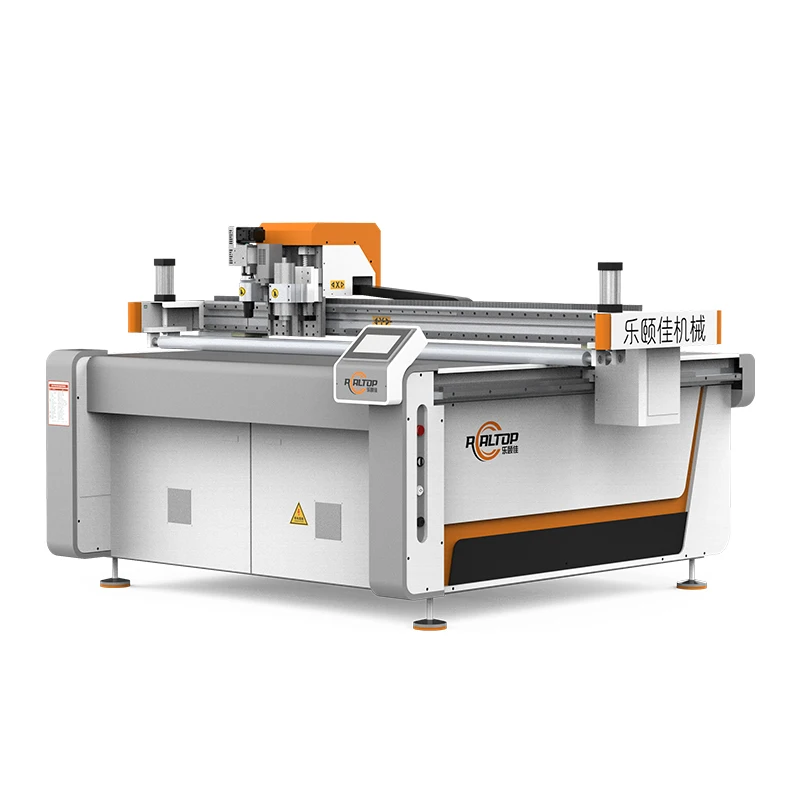
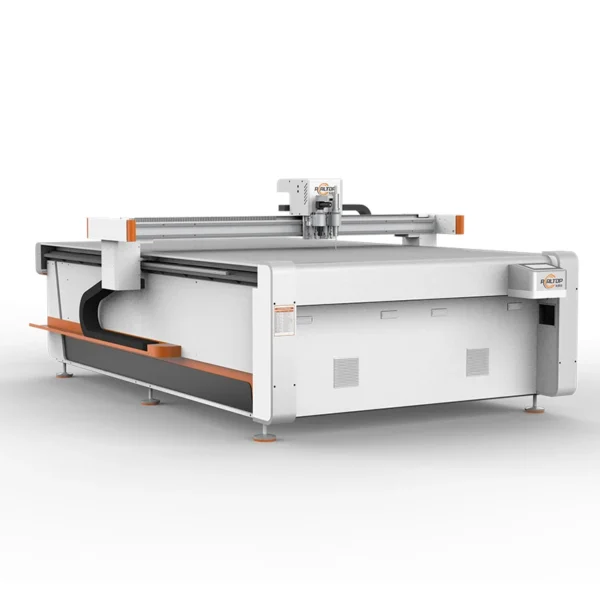
| Product Type | CNC Oscillating Knife Cutting Machine |
| Working Area | 1600×2500mm |
| Overall Dimensions (L×W×H) | 3450×2300×1250mm |
| Rated Power | 9kW |
| Voltage | 380V±10% |
| Fixed Model | Flat working table / Auto feeding table |
| Multifunctional Head | Swiss imported knife (vibration full cutting, vibration half cutting, cursor location function) |
| Translational Velocity | 800-2000mm/s |
| Cutting Speed | 200-800mm/s (according to different cutting materials) |
| Repeated Accuracy | ≤0.1mm |
| Vacuum Pump | 7.5kW |
| Vacuum Table | Magnesium-aluminum alloy, fluorocarbon PVDF powder spraying, anodic oxidation |
| Transmission System | Digital servo motor, linear guide, synchronous belt, ball screw |
| Safety Device | Infrared sensors |
| Instruction System | HP-GL compatible format |
| Software | Auto typesetting, supports PLT, DXF, AI formats |
Application Suitability
| Application | Material or Output |
|---|---|
| Packaging sample making | Corrugated board, greyboard, folding carton stock |
| Carton and corrugated cardboard cutting | V-groove slotting, creasing, full and half cutting |
| Leather goods and footwear | Genuine leather, synthetic PU/PVC, composite sheets |
| Fabric and textile processing | Multi-layer fabric, sponge composite leather, garment patterns |
| Automotive interiors | Carpet, floor mat, headliner fabric, acoustic insulation foam |
| Advertising signage | Printed vinyl, foam board, acrylic template contour cutting |
| Gasket and sealing pad fabrication | Rubber, silicon, carbon fiber, soft glass sheets |
Why "Standard Vacuum" Fails on Small Packaging Blanks
Vacuum table zoning must match the smallest part in the nest, not just the sheet size.
A buyer specifying a 1600×2500mm table often assumes the vacuum hold-down is uniform across the entire surface. When cutting small异形 carton blanks from corrugated stock, the suction force on a 50×50mm tab is a fraction of what holds a full sheet. The material lifts, the oscillating knife catches the edge, and you get ragged cuts and crushed flutes. This is a configuration issue, not a machine defect — but it only surfaces after the machine is on your floor [NEED_CITE: vacuum hold-down force distribution on zoned CNC tables].
Tool Head Selection Drives Edge Quality, Not Just Depth
Matching the tool head to the material determines whether you get a clean shear cut or a crushed, frayed edge. The RT-D2516/RT-S2516 platform supports oscillating knife, V-cutting knife, creasing wheel, drag knife, and punching tool heads on a single multifunctional carriage. For corrugated packaging samples, the V-cutting knife produces the slot for folding while the creasing wheel scores the fold line in one pass — eliminating the need for a secondary finishing step. A drag knife suits thin vinyl and sticker stock where an oscillating stroke would pull the material.
CCD Positioning on Printed Substrates at Production Speed
Contour cutting printed packaging prototypes or signage requires the camera to read registration marks before the knife engages. The small CCD camera mark point positioning and panoramic camera recognition options on this system address two different workflows: the small camera tracks discrete marks on individual sheets, while the panoramic option scans the full bed for roll-fed or gang-run layouts. Confirming which camera suits your substrate and mark size before the order prevents a machine that "works in the demo" but loses registration at 800mm/s translational velocity on your actual printed stock [NEED_CITE: CCD mark tracking accuracy on corrugated and coated substrates].
What the Specification Sheet Actually Means for Your Floor
The 7.5kW vacuum pump paired with a magnesium-aluminum alloy table with PVDF coating is a specific choice: the PVDF finish resists adhesive residue from sticker stock and corrugated dust buildup, maintaining suction over long production runs. The 9kW rated power covers the servo drives, spindle oscillation, and vacuum simultaneously — verify your workshop supply can sustain 380V±10% under load, as voltage sag below the tolerance band causes servo faults mid-cut. The repeated accuracy of ≤0.1mm across the 1600×2500mm working area relies on the ball screw and linear guide transmission; this tolerance holds when the machine sits on a level foundation free from forklift vibration. Servo motor selection between Delta and Panasonic affects response tuning and spare parts sourcing in your market, a decision best made with your local service network in mind.
The Cost of Skipping the Sample Cut
Ordering on working area alone and discovering the oscillating knife cannot cleanly shear your 3mm foam gasket at production speed is a preventable failure. The wrong tool head produces ragged edges on fabric or crushes the flute structure on single-face corrugated. Software that cannot import your existing PLT or DXF nesting files means re-drawing every pattern from scratch. These issues surface only when your material runs through the machine, which is why a sample cutting report on your actual stock at target speed is the only valid proof of configuration [NEED_CITE: material-specific tool head validation in CNC cutting procurement].
Sourcing From a Factory That Builds Both Knife and Laser
In-house design covering oscillating knife and creasing wheel tooling on one platform means the cutting method is matched to the fold line requirement, not forced into a single tool path. Tool head and table configuration is specified per your material type and daily volume, not pulled from a default list. CCD camera positioning is confirmed against your print mark size and substrate color before the order is locked. Software file format compatibility — PLT, DXF, AI — is verified with your nesting workflow during the pre-order stage. Voltage, plug type, and control panel language are documented on the electrical schematic before the machine enters production, avoiding the shipment of a 380V unit to a 220V workshop.
Documentation & Verification
- Machine specification sheet listing confirmed tool heads and vacuum zone layout
- Electrical schematic with voltage and frequency matched to your facility supply
- Tool head and table configuration list signed against your material samples
- Sample cutting report on your corrugated board and leather stock at production speed
- Software licence and file format compatibility note for PLT, DXF, AI imports
- Factory test record capturing repeated accuracy across the full 1600×2500mm bed
Installation, Commissioning & Support
- Level concrete floor required to maintain ≤0.1mm repeated accuracy across the 2500mm axis
- Dedicated 380V±10% circuit rated above 9kW to prevent servo faults under load
- Machine ships with table and gantry separated; overhead clearance of 1250mm needed for reassembly
- First-run parameter tuning for oscillation frequency and vacuum zone mapping on your material
- Touch screen control panel configured in your operator language before dispatch
- Spare parts list covering Swiss knife blades, creasing wheels, and vacuum seals included at delivery
Preparing Your Inquiry
To receive a configuration that matches your production, provide the material type and maximum thickness you cut daily, the smallest part dimension in your typical nest, and the file format your design team currently outputs. Confirm your workshop voltage and frequency, and whether you need flat table loading or auto-feeding for roll stock. If you run printed substrates, specify the mark type and color contrast so the correct CCD option is quoted.
Frequently Asked Questions
Q: How is cutting thickness verified per material, and what is the basis for the stated cutting speed range?
A: The 200-800mm/s cutting speed depends on material density and thickness. We run your actual stock through the machine before the order is confirmed, documenting the tool head, oscillation frequency, and achieved edge quality in a sample cutting report. This report becomes the configuration baseline, so the speed you see on your material is the speed you receive.
Q: How do I choose the correct tool head — oscillating knife vs V-cutting knife vs creasing wheel — for my material?
A: The oscillating knife shears through flexible and semi-rigid stock with a clean edge. The V-cutting knife removes a channel in corrugated board for folding without cutting through the liner. The creasing wheel scores fold lines without penetrating the surface. Your material type and fold requirement determine the combination, confirmed during the sample cutting stage.
Q: Can the CCD camera track printed marks at full production speed on my specific substrate?
A: The small CCD camera handles discrete registration marks on individual sheets, while the panoramic camera scans full-bed layouts for gang-run jobs. Tracking reliability depends on mark size, contrast against your substrate, and surface gloss. We test with your printed material to confirm the camera holds registration at the translational velocity you require.
Q: What voltage, plug type and control language are confirmed before shipment?
A: The standard configuration is 380V±10%, but the electrical schematic is confirmed against your facility supply before production. Plug type and touch screen control language — English, Russian, Italian, Chinese, or other options — are locked on the order documentation. This prevents receiving a machine that requires an on-site transformer or re-flashed control panel.
Q: How is vacuum table zoning configured for small parts to prevent material lift during cutting?
A: The 7.5kW vacuum pump feeds zones across the magnesium-aluminum alloy table. For nests containing small carton blanks or gasket pieces, specific zones are activated to concentrate suction under the part footprint. The zone layout is defined during the sample cutting test on your actual nest pattern, ensuring hold-down force matches your smallest component.


商品评价
Clear filtersThere are no reviews yet.