








Fast Shipping
Carrier information

20k products
Payment methods

24/7 Support
Unlimited help desk

2-day Delivery
Track or off orders
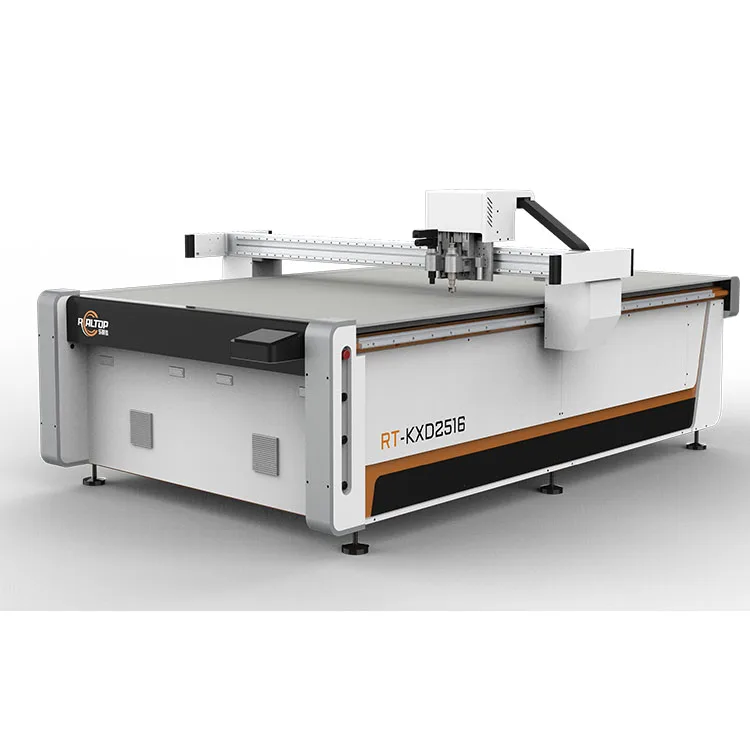
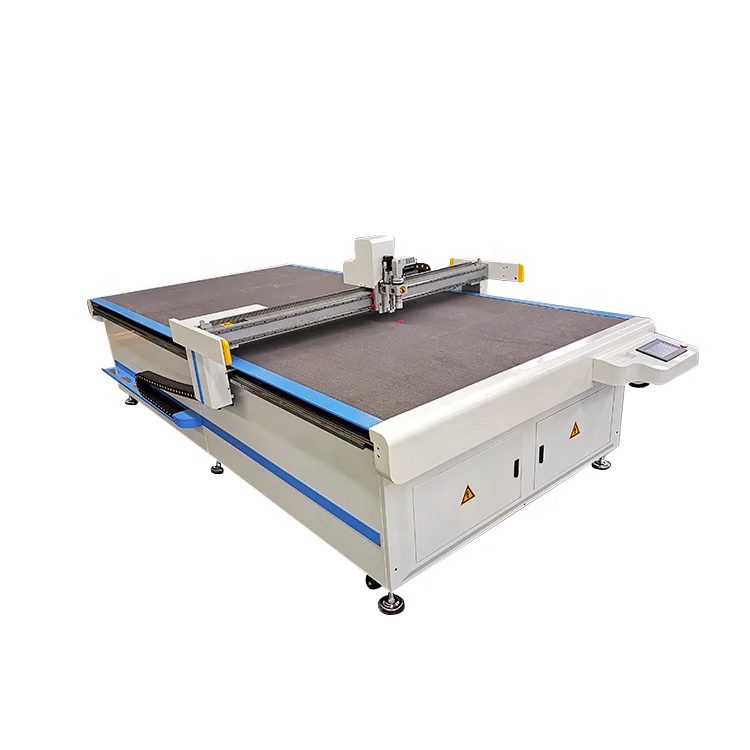
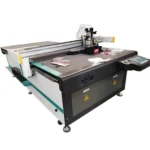
Configurable knife and creasing tool heads — The RT-D2516/RT-S2516 platform matches oscillating knife, drag knife, or creasing wheel configurations to the buyer’s actual board grade rather than defaulting to a single tool setup.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | RT-D2516/RT-S2516 |
| Product Type | CNC Oscillating Knife Cutting Table |
| Working Area | 1600 × 2500 mm |
| Machine Size | 3450 × 2300 × 1250 mm |
| Rated Power | 9 kW |
| Table Type | Flat working table with vacuum adsorption |
| Tool Head | Swiss imported knife with vibration full cutting, half cutting, and cursor location |
| Translational Velocity | 800–1200 mm/s |
| Cutting Speed | 200–800 mm/s (according to different cutting materials) |
| Repeated Accuracy | ≤0.1 mm |
| Transmission System | Digital servo motor, linear guide, synchronous belt, ball screw |
| Servo Motor | Delta |
| Guide Rail | Taiwan Hiwin |
| Instruction System | HP-GL compatible format |
| Vacuum Pump | 7.5 kW |
| Voltage | 380V ± 10% |
| Safety Device | Infrared sensors |
| Frame | Welded thick square seamless steel structure with high temperature treatment |
| Software | Professional carton cutting design software (language customizable) |
| Certification | CE (declaration where applicable) |
Application Suitability
| Application | Material or Output |
|---|---|
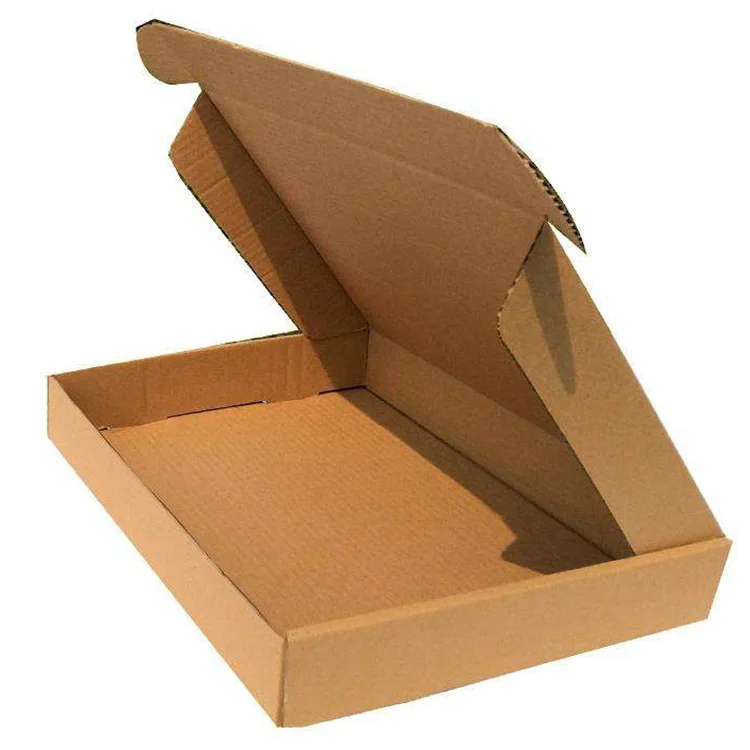
| Packaging carton sample making | Corrugated board (single and double wall), greyboard, folding carton stock |
| Paper box and gift box production | Cardboard, coated paper board, kraft paper laminates |
| Sticker and label contour cutting | Self-adhesive vinyl, PP/PVC sticker sheets |
| Billboard and business card cutting | Foam board, PVC sheet, thin composite panels |
| Gasket and seal fabrication | Rubber, silicone, soft composite sheets |
Why Tool Head Selection Matters More Than Working Area
A flatbed table specified only by its cutting envelope often fails when it meets the actual flute profile and density of the board running on the shop floor. The right CNC Oscillating Knife Cutting Table specifications must account for material thickness, edge quality requirements, and the creasing depth needed for clean fold lines.
The tool head, not the table size, determines whether the machine cuts your material or destroys it.
I once saw a packaging shop receive a machine quoted on working area alone. The board was high-density corrugated, and the oscillating knife was underpowered for the flute structure. Edges came out crushed, creasing lines were shallow, and the operator spent more time clearing debris than feeding sheets [NEED_CITE: oscillating knife torque requirements by corrugated flute type]. When the tool head does not match the board grade, throughput drops regardless of how fast the servo motors can travel.
Oscillating Knife and Creasing Wheel Configuration
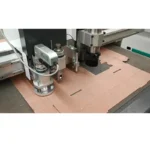
The Swiss imported knife head on the RT-D2516/RT-S2516 handles full cutting and half cutting within a single tool station. Full cutting separates the carton blank from the surrounding matrix, while half cutting scores the fold lines without penetrating the bottom liner. This dual function eliminates the need for a separate creasing station on most standard corrugated and greyboard jobs. The oscillating frequency and blade geometry are selected based on the board composition specified at inquiry.
Vacuum Adsorption and Small-Part Stability
The 7.5 kW vacuum pump drives the flat working table adsorption system. On large sheets, full-table vacuum holds the material flat during high-speed passes. When cutting small carton parts or narrow gasket strips, concentrated vacuum zones prevent the pieces from lifting off the table surface as the knife exits a cut path. This zoning approach reduces the vacuum pump load while maintaining holding force where it is needed most. Without adequate zoning, small parts shift mid-cut and produce dimensional errors that fail downstream assembly [NEED_CITE: vacuum adsorption zoning for flatbed digital cutters].
Reading the Specs That Affect Daily Production
Cutting speed on the RT-D2516/RT-S2516 ranges from 200 to 800 mm/s depending on the material being processed. Thinner sticker sheets and vinyl allow the upper range, while multi-layer corrugated or dense rubber gasket stock requires slower passes to maintain edge integrity. The Delta servo motors and Taiwan Hiwin linear guides maintain ≤0.1 mm repeatability across the full 1600 × 2500 mm working area, which keeps nested carton blanks within tolerance for automated folding and gluing equipment downstream. The HP-GL compatible instruction system accepts files from common packaging CAD software, reducing the gap between design and production. The 9 kW rated power covers the combined load of the servo drives, oscillating head, and vacuum pump running simultaneously. Frame rigidity from the welded steel structure with high temperature treatment prevents vibration from accumulating into positional drift during long production runs.
The Hidden Cost of Skipping Material Trials
Skipping a sample cut on the buyer’s own board stock is the fastest way to receive a machine that runs at a fraction of expected output. Tool head selection without a physical test leaves creasing depth to guesswork. Vacuum configuration without seeing the smallest part in the nesting layout results in lift and misregistration. Software file import without testing the buyer’s CAD export format causes delays on the first production day [NEED_CITE: packaging CAD file format compatibility with CNC cutting software]. These issues surface only after the machine is installed, when returning it is no longer practical.
Why Source This Configuration Here
The RT-D2516/RT-S2516 is designed and built in-house, covering both knife cutting and table engineering under one production line. Tool head and vacuum configurations are specified per material rather than sold as a fixed package. CCD camera positioning can be integrated for printed contour work where registration marks guide the cut path. Software compatibility is confirmed before the order ships, so the buyer’s existing nesting workflow connects directly to the machine controller. Voltage, plug type, and control language are documented and verified prior to dispatch. Sample cutting on the buyer’s own material runs at production speed before commitment, producing a written report that accompanies the quotation.
Documentation & Verification
- Machine specification sheet listing tool head options, vacuum pump rating, and voltage confirmation
- Electrical schematic showing 380V ± 10% wiring with plug type and control language noted
- Sample cutting report run on buyer’s board grade at production cutting speed
- Tool head and table configuration list matched to stated material type and thickness
- Software licence note confirming HP-GL format compatibility with buyer’s CAD workflow
- Factory test record with repeatability measurement across the full working area
Installation, Commissioning & Support
- Floor space allocation for 3450 × 2300 mm machine footprint plus material feed and offload clearance
- Dedicated 380V ± 10% circuit with rated capacity above 9 kW to accommodate vacuum pump startup surge
- Machine arrives with tool head pre-mounted; vacuum table leveling verified during commissioning
- Cutting speed and oscillating frequency calibrated on-site using buyer’s actual board stock
- Operator training covers carton software nesting workflow, tool change procedure, and vacuum zone setup
- Spare blade and consumable parts list provided with recommended replacement intervals
What to Include in Your Inquiry
Send the specific board grade, flute type, and thickness range your shop runs most frequently. Note the smallest and largest carton blank dimensions in your typical nesting layout. Confirm the local voltage standard and frequency, along with the control panel language requirement.
Frequently Asked Questions
Q: How do I confirm the correct tool head for my corrugated board type?
A: The tool head is selected based on your board flute profile, total thickness, and whether you need full cutting, creasing, or both. We run a sample cut on your actual board stock at production speed and document the blade geometry, oscillating frequency, and creasing depth that produced clean edges. This report is included with the quotation so the configuration is locked before production begins.
Q: What file formats does the carton cutting software accept?
A: The professional carton design software supports HP-GL compatible format, which covers output from most standard packaging CAD systems. Before the order is finalized, we confirm file format compatibility by importing a sample file from your existing design workflow. Language customization for the software interface is included with lifelong technical support.
Q: How does vacuum table zoning prevent small parts from lifting?
A: The flat working table uses a 7.5 kW vacuum pump with zone-specific adsorption. When cutting small carton parts or narrow gasket strips, vacuum concentrates in the active cutting area rather than across the entire table. This targeted holding force keeps lightweight pieces flat as the knife exits each cut path, reducing misregistration caused by material movement.
Q: What voltage and language options are confirmed before shipment?
A: The standard configuration runs on 380V ± 10%, but voltage and plug type are confirmed to match your facility’s electrical standard. Control panel language and software interface language are specified at the order stage and documented in the electrical schematic and software licence note provided before dispatch.
Q: Can CCD contour recognition be added for printed carton cutting?
A: CCD camera positioning is available for jobs where the cut path must follow printed registration marks on the board surface. We verify during the sample cut that the camera tracks your specific print marks at production speed. Contour recognition capability and limitations for your print contrast and mark size are documented in the sample cutting report.


商品评价
Clear filtersThere are no reviews yet.