



Fast Shipping
Carrier information

20k products
Payment methods

24/7 Support
Unlimited help desk

2-day Delivery
Track or off orders
Precision Tooling Match — the 1625 platform is engineered to pair specific knife, creasing and milling heads with your exact flute grade or foam density, avoiding the common trap of forcing one blade through materials it was never meant to cut.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | 1625 |
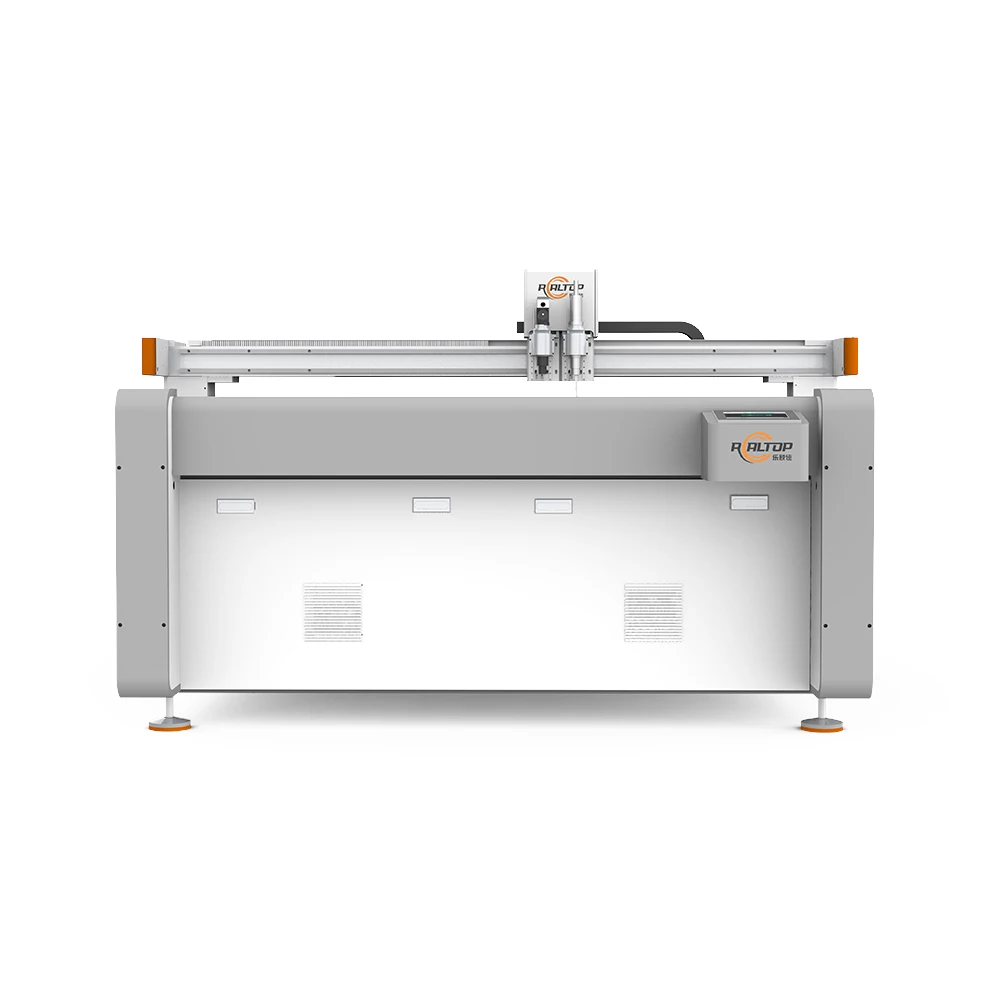
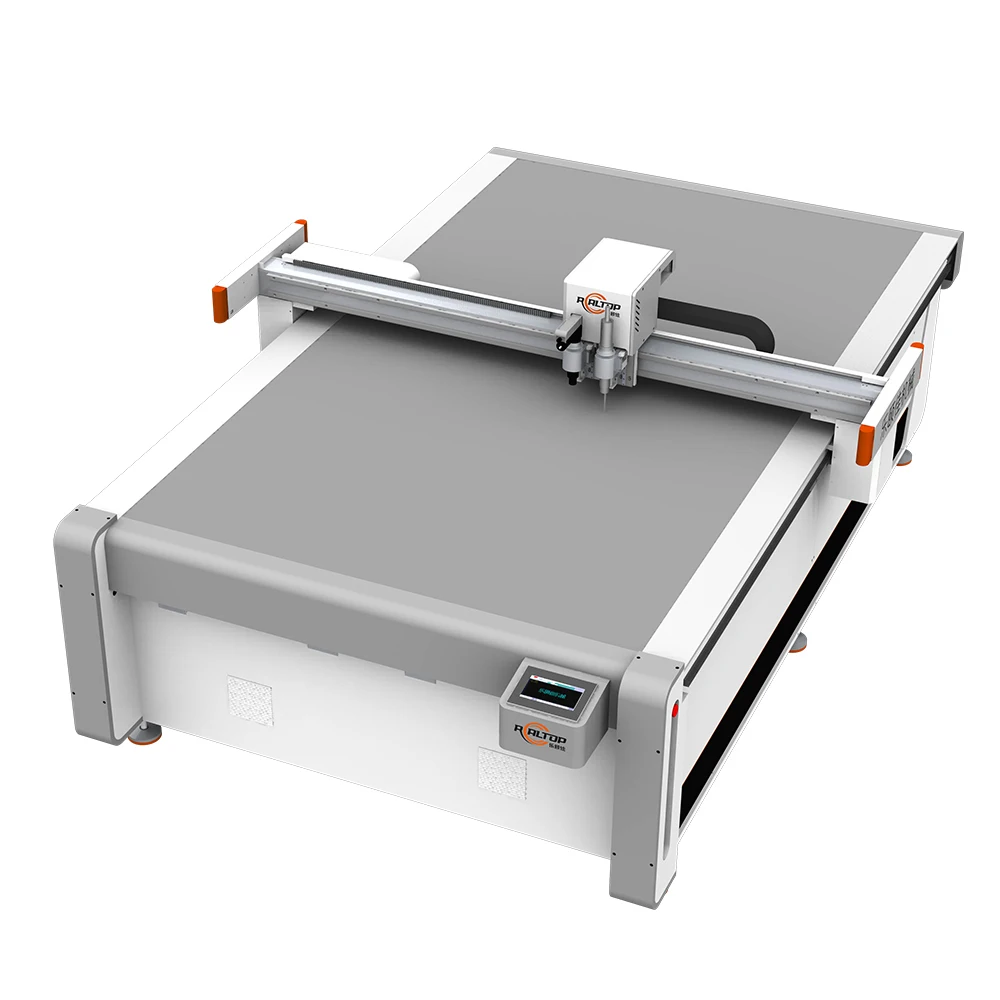
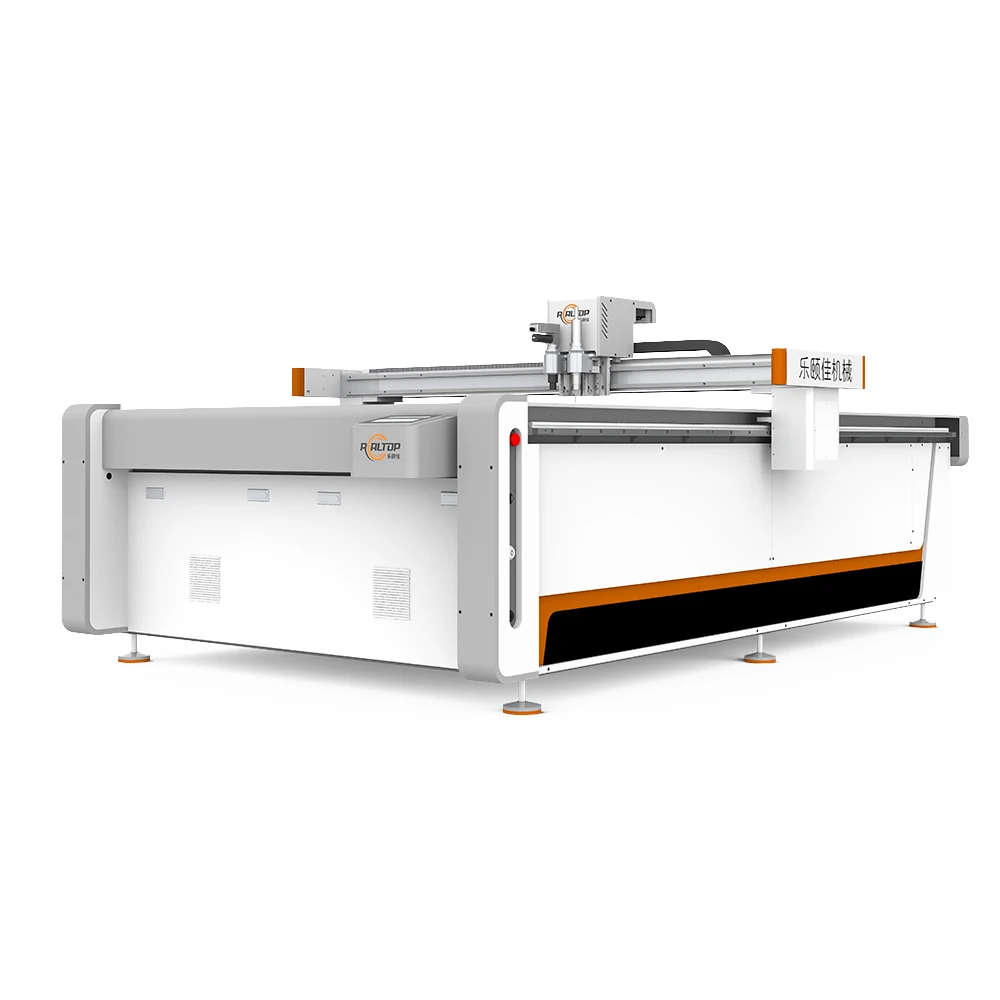
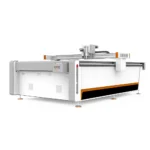
| Product Type | CNC Oscillating Knife Cutting Machine |
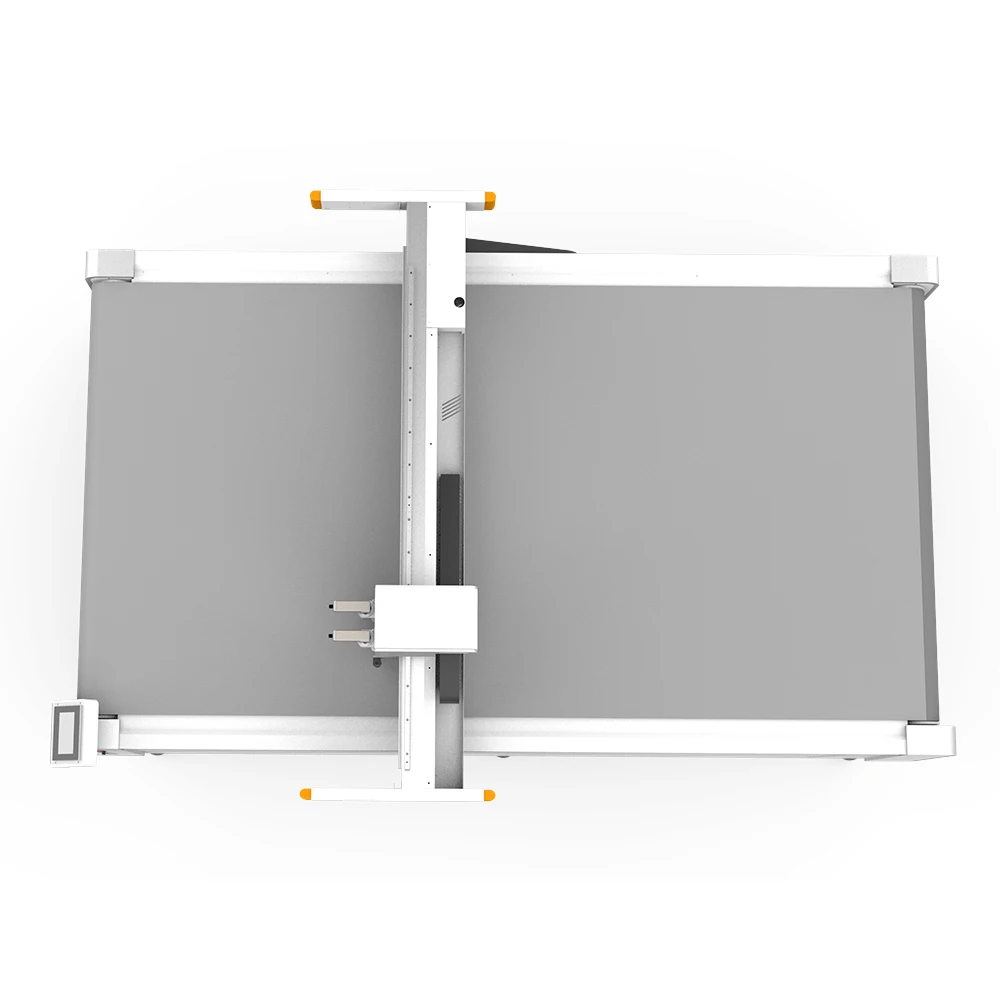
| Working Area | 1600 × 2500 mm |
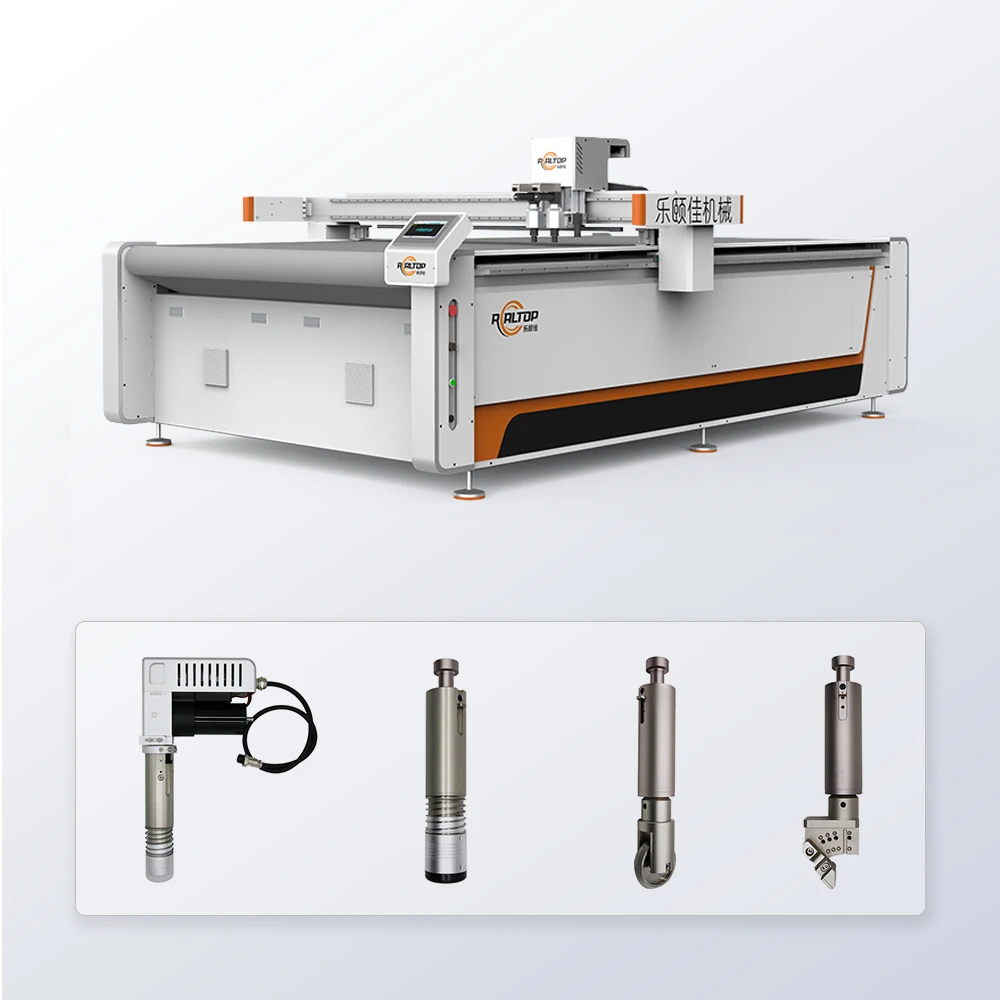
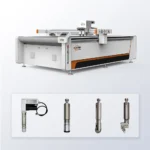
| Tool Head Options | Oscillating knife, Driven rotary knife, Creasing wheel, Kiss cutting tool, Pneumatic knife, Milling tool, V groove knife |
| Cutting Thickness | ≤ 40 mm (material dependent; verify with sample test) |
| Cutting Speed | 0–1500 mm/s |
| Cutting Accuracy | ±0.1 mm |
| Vacuum Table | Aluminum bellows vacuum table |
| Vacuum Pump Power | 9 kW |
| Control System | PLC control panel |
| Servo Motors | Panasonic, Delta or Dorna options |
| Profile Formats Supported | PLT, DXF, AI, PDF |
| Voltage Options | 110V, 220V, 380V |
| Control Language Options | English, Russian, Italian, Chinese (customizable) |
| Safety Features | Infrared sensor device and emergency stop device |
| Machine Size | 3300 × 2100 × 1350 mm |
| Standards | CE |
| Software | Dedicated packaging box structure design software |
Application Suitability
| Application | Material or Output |
|---|---|
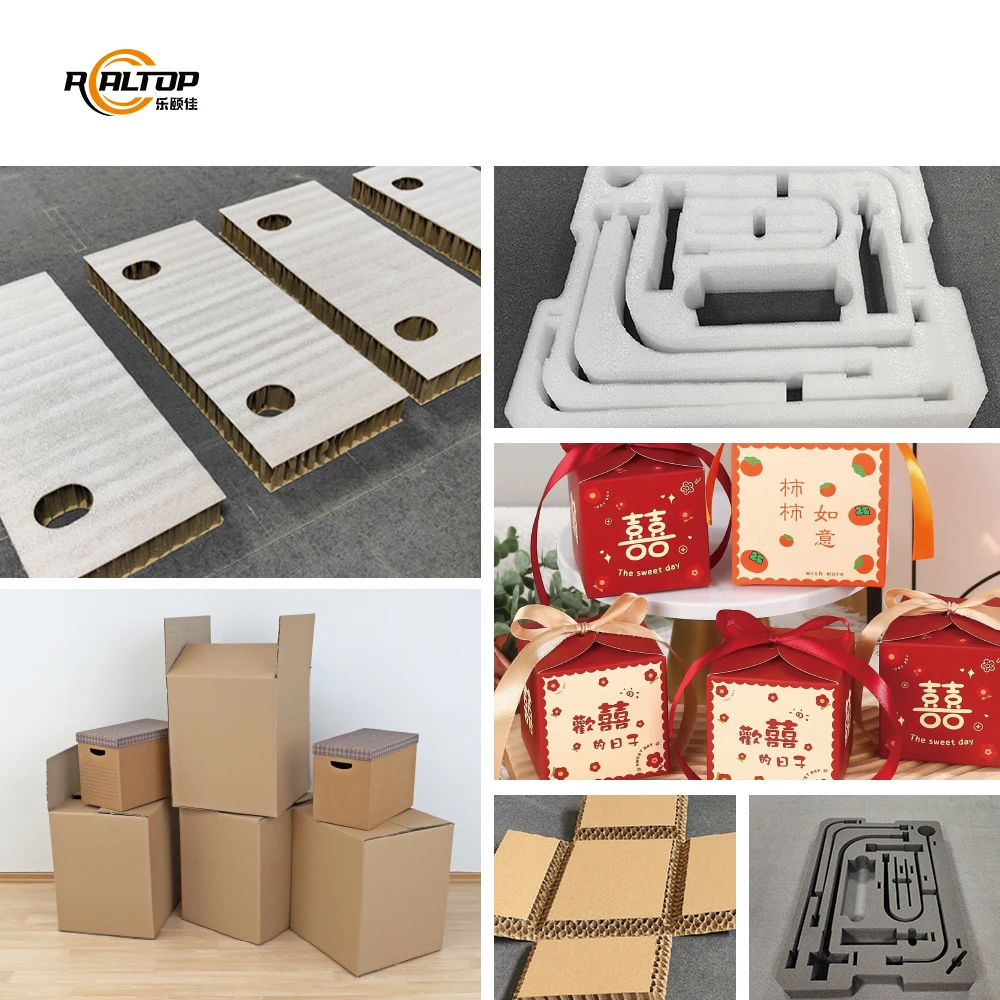
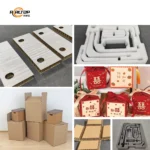
| Packaging sample making | E-flute, B-flute, BC-flute corrugated board |
| Carton prototype production | Greyboard, cardstock, art paper, specialty paper |
| Protective insert cutting | EVA, EPE, PU foam |
| Gasket and liner cutting | Rubber mats, PTFE, non-woven fabric |
| Display and signage blanks | PVC, PET, thin plastic sheets |
| Leather and composite trimming | Leather, synthetic leather, adhesive-backed materials |
When "Cutting Thickness" Specifications Hide the Real Problem
The ≤ 40 mm figure on the spec sheet is a starting point, not a guarantee — actual depth depends entirely on material density and the tool head you select.
A buyer once sent me a sample of high-moisture corrugated board destined for a packaging plant in East Africa. The fibers were soft, the flute walls compressed under standard oscillating knife pressure, and the edges came out ragged. Switching to a heavier pneumatic knife and adjusting the vacuum hold-down cleaned up the cut, but only after we had already tested three tool configurations. That is the reality behind the numbers: material condition, humidity and density all shift the practical limit [NEED_CITE:corrugated board moisture and machinability standards].
Tool Head Selection by Material and Flute Grade
The 1625 carries seven interchangeable tool heads on a single gantry. For short-run corrugated prototypes, the oscillating knife handles E-flute and B-flute with clean shear edges, while BC-flute and double-wall grades often demand the driven rotary knife to slice through thicker walls without crushing the flute structure.
Creasing wheels and V groove knives handle the fold lines that make a carton functional. When a packaging designer needs both a crease and a full cut on the same sheet, the machine swaps tools automatically within the same program cycle. The CNC oscillating knife cutting machine specifications only become meaningful once you map each tool head to the specific material in your production mix.
Vacuum Hold-Down and Small Part Stability
The aluminum bellows vacuum table and 9 kW pump provide full-surface suction across the 1600 × 2500 mm bed. The critical question for carton sample makers is zoning — if you are cutting a nest of small gusset panels or hinge tabs, insufficient zoning lets those pieces lift under the knife, producing miscuts and forcing a re-run [NEED_CITE:vacuum table zoning requirements for small die-cut parts].
Confirm the number of vacuum zones and whether the table can be masked to concentrate suction on the active cutting area before you sign off on the configuration.
Reading the Specifications Beyond the Brochure
The Panasonic, Delta or Dorna servo motors drive the gantry to ±0.1 mm positioning accuracy. In packaging sample work, that tolerance matters most on crease-to-cut registration — a half-millimetre drift between the fold line and the cut edge produces a box that does not close square.
Cutting speed reaches 0–1500 mm/s, though actual throughput depends on the complexity of the contour, the number of tool changes per sheet and the nesting layout the software generates. The PLC control panel supports PLT, DXF, AI and PDF import, but file format compatibility must be confirmed against your existing design workflow. If your structural designer works in a proprietary packaging CAD suite, verify that the exported DXF carries crease line attributes the machine recognizes [NEED_CITE:DXF crease layer conventions in packaging CAD].
The Cost of Skipping the Sample Cut
When a machine arrives configured for standard B-flute and your production runs include heavy BC-flute or dense EVA foam, the wrong tool head produces crushed edges, delaminated flute walls and rejected prototypes. Re-tooling after delivery means new blades, recalibration and lost production days. Every configuration decision — tool head, vacuum zone layout, knife oscillation frequency — should be locked in by a sample cutting report on your actual material, not assumed from a generic specification sheet.
Why This Platform Fits Packaging Short-Run Work
In-house design and production of both knife and creasing tooling means the 1625 can be specified for your exact material range rather than adapted from a generic cutting platform. Tool head and table configuration are matched per material and daily volume before the order is confirmed. Voltage, plug type and control panel language are documented in writing before shipment, avoiding the installation-day surprise of a 380V machine arriving at a 220V workshop. The dedicated packaging box structure design software carries licence and compatibility documentation, so your design files load without manual layer re-mapping [NEED_CITE:CE machinery directive documentation requirements].
Documentation & Verification
- Machine specification sheet with confirmed tool head and table layout
- Electrical schematic and voltage confirmation for your site supply
- Sample cutting report on your corrugated grade or foam density
- Factory test record before dispatch showing cut accuracy
- Software licence and file format compatibility note
- CE declaration where applicable
Installation, Commissioning & Support
- Floor space allocation for the 3300 × 2100 mm footprint plus operator access
- Dedicated circuit matching the confirmed 110V, 220V or 380V supply
- Gantry and vacuum table assembly on arrival with alignment verification
- First-run parameter tuning on your actual carton stock or foam
- Operator training on tool head changeover and PLC language settings
- Spare knife blades and creasing wheels matched to your material range
What to Send with Your Inquiry
Provide the corrugated flute grades, greyboard weights or foam densities you cut, along with typical sheet size and daily sample volume. State your local voltage and frequency, preferred control language and the CAD software your designers currently use. If you can ship a stack of your actual material, we will run a sample cut and return the report before any commercial commitment.
Frequently Asked Questions
Q: How do I verify the real cutting thickness for my corrugated board?
A: The ≤ 40 mm figure is a maximum under ideal conditions. Send a sample of your actual flute grade — including E-flute, B-flute or BC-flute — so a test cut confirms edge quality and practical depth before the configuration is finalized.
Q: Which tool head should I use for foam inserts and carton creases together?
A: The oscillating knife handles most foam densities cleanly, while the creasing wheel produces fold lines on board stock. The 1625 can hold both heads and swap within the same program cycle, but the exact combination depends on your material mix.
Q: Will small carton parts stay flat during cutting?
A: The aluminum bellows vacuum table and 9 kW pump provide strong hold-down, but small parts require adequate vacuum zoning. Confirm zone layout and masking capability during the configuration stage to prevent piece lift.
Q: Is the software compatible with my existing packaging design files?
A: The system imports PLT, DXF, AI and PDF formats. Share a sample file from your current design workflow so we can verify layer recognition, crease line attributes and nesting compatibility before shipment.
Q: How is voltage and language confirmed before the machine ships?
A: Your local voltage, frequency and plug type, along with the control panel language, are documented in the order specification sheet. This written confirmation ensures the electrical supply and interface match your workshop on arrival.


商品评价
Clear filtersThere are no reviews yet.