


Fast Shipping
Carrier information

20k products
Payment methods

24/7 Support
Unlimited help desk

2-day Delivery
Track or off orders
Tool-to-material matching — Every T-series plotter ships with a cutting tool and vacuum layout proven on the buyer’s actual stock, not a generic desktop demo.
Technical Specifications
| Parameter | Value |
|---|---|
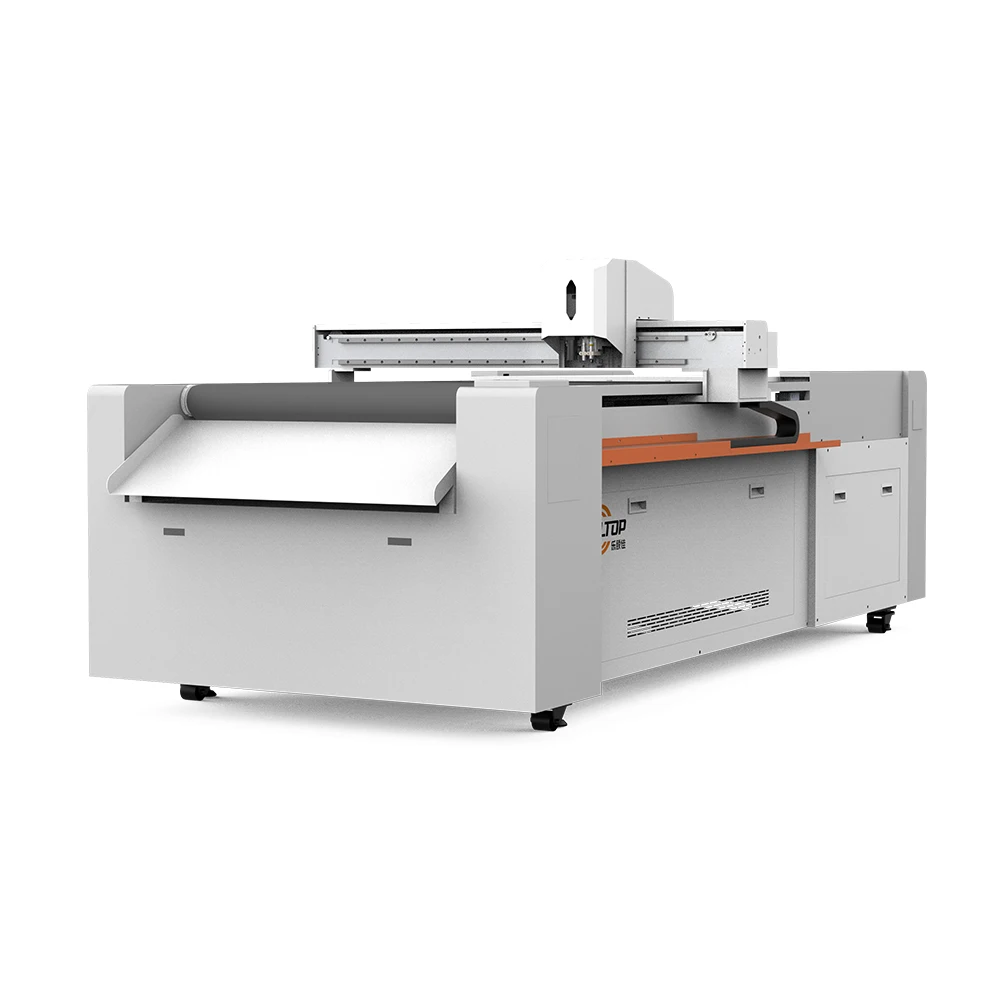
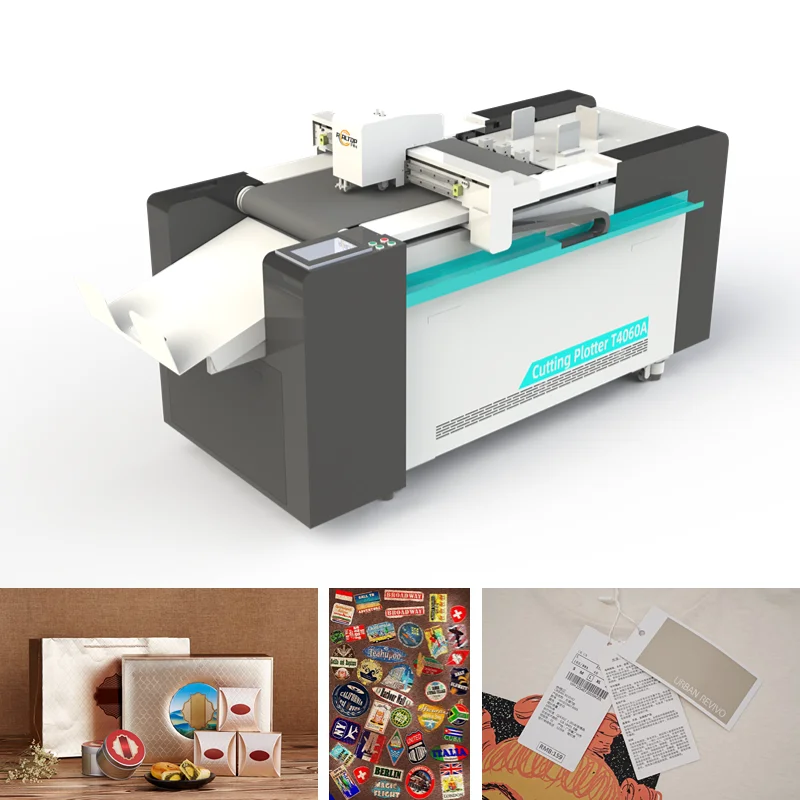
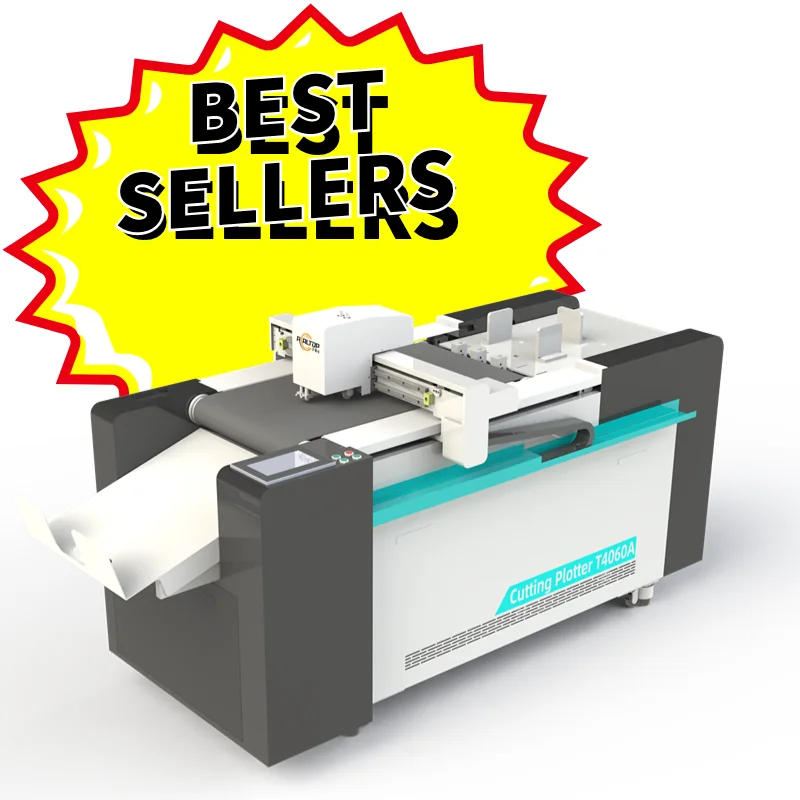
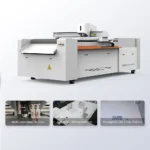
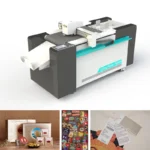
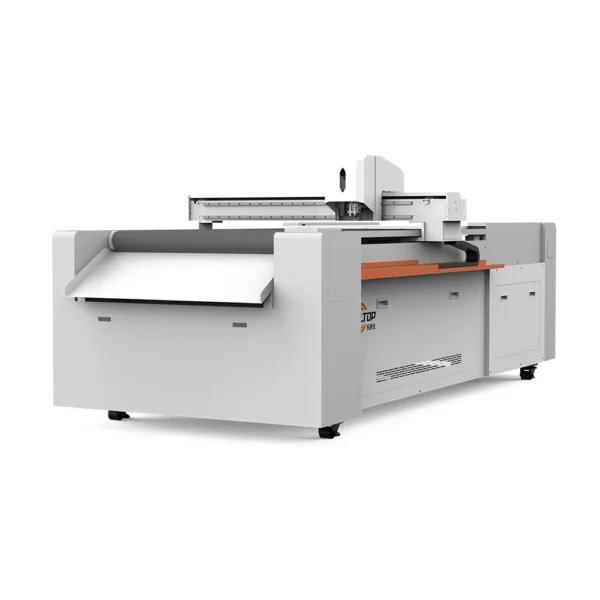
| Product Type | CNC Digital Cutting Plotter |
| Model | 4060 / 6080 / 0912 |
| Working Area | 400×600 mm / 600×800 mm / 900×1200 mm |
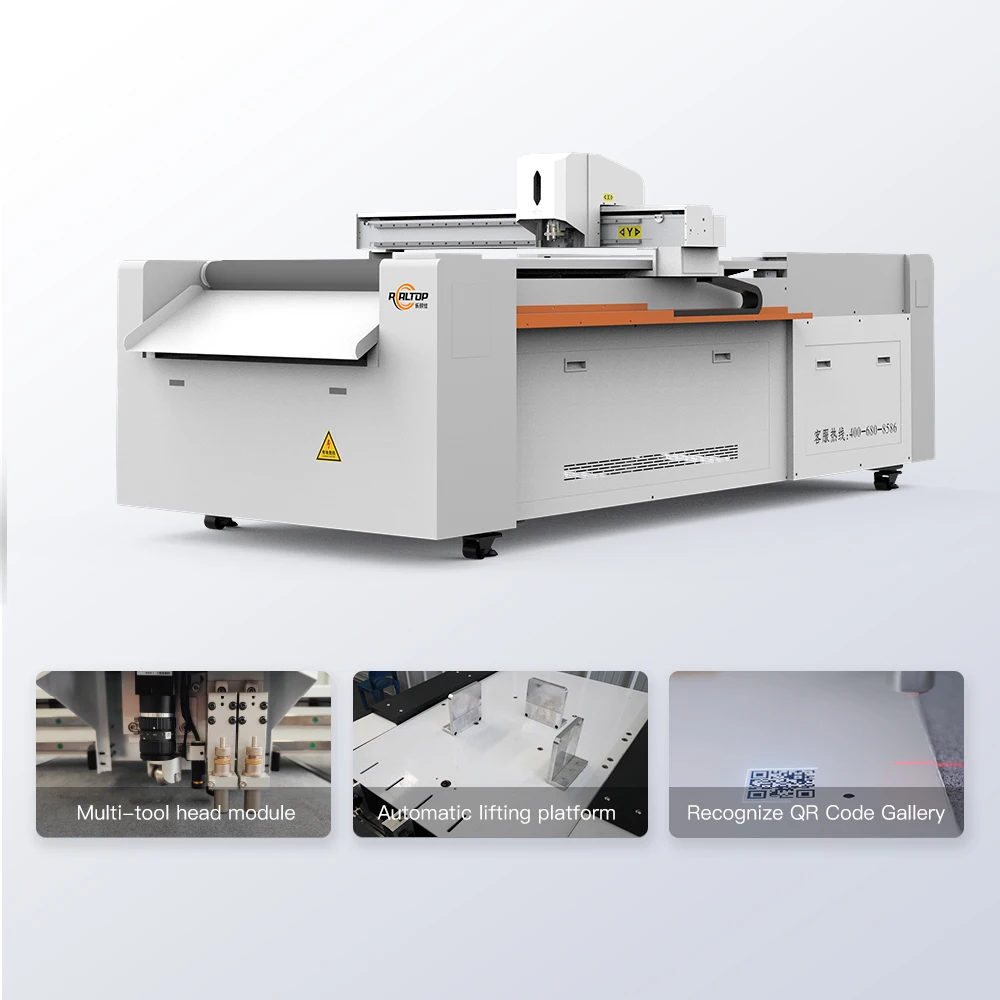
| Tool Head Options | Oscillating knife, Creasing wheel, Kiss cutting tool, Marking pen |
| Contour Recognition | CCD camera with auto-registration mark tracking |
| Cutting Speed Range | 0–1500 mm/s |
| Maximum Cutting Thickness | ≤ 20 mm (basis to be confirmed by material density) |
| Repeat Positioning Accuracy | ±0.1 mm |
| Vacuum Pump Rating | 2.5 kW / 3.2 kW |
| Voltage Options | 110 V / 220 V (frequency to be confirmed) |
| File Format Compatibility | PLT, DXF, AI, PDF |
| Safety Equipment | Infrared sensor barrier, emergency stop |
| Software Interface Languages | English, Russian, Italian, Chinese (customizable) |
| Control Interface | USB / direct drive / computer control |
| Certification | CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Packaging prototype sampling | Corrugated board, white cardstock, laminated gold-silver card |
| Short-run carton mock-ups | Folding box board, greyboard up to rated thickness |
| Self-adhesive label cutting | Vinyl, PVC sticker film, reflective sheeting |
| Signage and graphics | Foam board, magnetic sheet, window cling film |
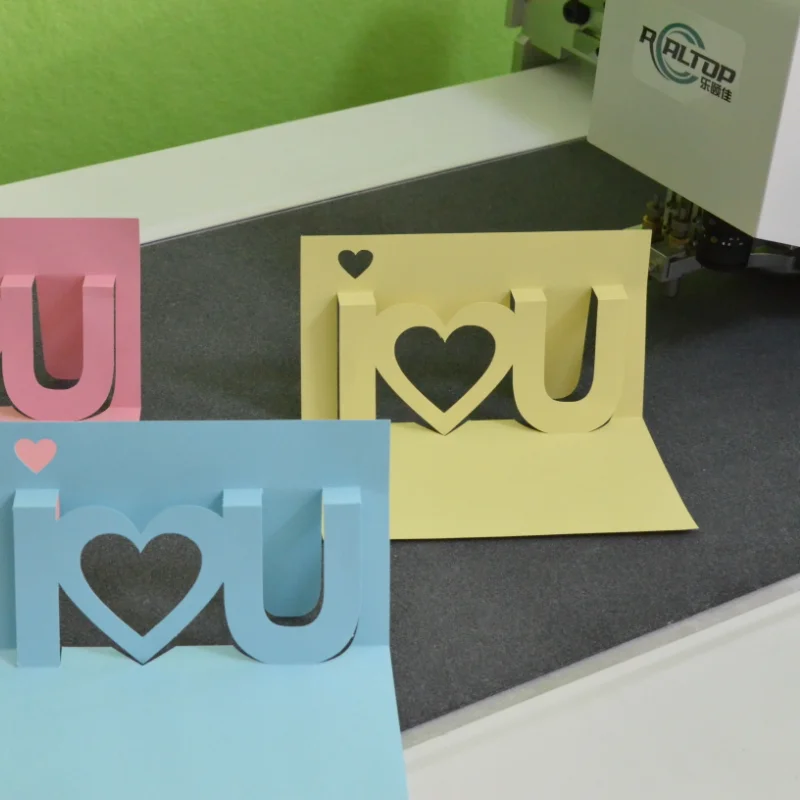
| Cultural craft production | Leather tags, photo backing paper, printed box stock |
| Light industrial gaskets | Electronic foam, thin rubber sheet, composite felt |
Why "Cutting Thickness" Without Material Density Is Meaningless
A 20 mm rating on soft foam tells you nothing about how the same blade handles 2 mm laminated gold-silver card. I spent three days in a Dubai carton plant re-tuning knife pressure and spindle speed after two thousand sheets of laminated stock were ruined — the machine had been specified on white card alone. When buyers ask for CNC oscillating knife cutting table specifications, the number that matters is what the blade actually does to their specific sheet [NEED_CITE: material density and tensile variation across packaging stock grades]. A machine set for standard corrugated will crush the coating off a foil-laminated box blank or leave ragged micro-tears on self-adhesive vinyl. The tool head, oscillation frequency and vacuum hold-down must all be confirmed against the buyer’s real production stock before any purchase order is signed.
Matching the Tool Head to the Substrate
An oscillating knife handles corrugated and foam cleanly because the vertical vibration slices through fibrous structure without dragging. A creasing wheel compresses rather than cuts, producing fold lines on carton without breaking the outer liner. Kiss cutting tools score the top layer of label stock while leaving the release liner intact. Each head mounts to the same T-series carriage, so one machine covers plot-and-cut workflows that would otherwise need separate stations. Selecting the correct CNC oscillating knife cutting table specifications starts with a physical sample of the heaviest and most abrasive material the shop will run.
What Repeat Positioning Accuracy Actually Controls on a Plotter
The ±0.1 mm repeat positioning figure governs how closely the blade follows a vector path on successive cuts. On intricate fonts, tight radii and interlocking puzzle pieces, any drift accumulates across the sheet and shows as misaligned crease lines or broken ligatures. This tolerance depends on the linear guide preload, belt tension and servo loop tuning leaving the factory [NEED_CITE: linear motion repeatability testing standards for CNC plotters]. A plotter that holds ±0.1 mm on a warm-up run but drifts after four hours of continuous cutting will produce scrap in a real short-run packaging shift.
Reading the Specification Sheet Against Real Production Conditions
The 0–1500 mm/s cutting speed range is a traverse maximum; actual profile speed drops on every direction change and tight corner. The 2.5 kW and 3.2 kW vacuum pump options determine how much suction reaches the table surface — undersized pumps let small vinyl decals lift off the bed mid-cut. File format support for PLT, DXF, AI and PDF removes the translation step that corrupts bezier curves, but the nesting software must also accept the buyer’s existing layout files. Voltage at 110 V or 220 V must match the workshop supply, including frequency, before the motor winding is built [NEED_CITE: industrial voltage and frequency compatibility for exported CNC equipment].
The Hidden Cost of a Generic Desktop Configuration
A plotter specified only by working area arrives with a single tool head, a full-sheet vacuum zone and a generic blade holder. Small sticker jobs lift at the edges because the vacuum cannot concentrate suction on a 30 mm part. Laminated card frays because the oscillation amplitude was never adjusted for coated stock. The software refuses to open the buyer’s nesting templates, forcing a manual redraw that doubles prepress time [NEED_CITE: typical workflow losses from software incompatibility in digital finishing]. These failures surface only after the machine is on the production floor and the return shipping cost exceeds the price difference of a correctly configured unit.
Why Buyers Source the T-series Through This Channel
In-house design covers both knife and laser cutting methods, so the buyer selects the process that fits the material instead of forcing one technology across every substrate. Tool head and vacuum table zoning are specified per material type and daily volume, not left to a default build. CCD camera positioning is tuned to the buyer’s print mark size and contrast before shipment. Software compatibility is confirmed by importing the buyer’s own nesting files during the sample stage. Voltage, plug type and control language are written into the production order so the machine arrives ready to power on.
Documentation & Verification
- Machine specification sheet listing confirmed tool head and vacuum pump pairing
- Electrical schematic with voltage and frequency locked to buyer’s workshop supply
- Sample cutting report produced on buyer-supplied material before order
- Software licence and file format compatibility note covering buyer’s nesting workflow
- Factory test record showing repeat positioning across a full sheet cycle
- Spare parts list matched to the configured tool heads and blade types
Installation, Commissioning & Support
- 900×1200 mm maximum footprint requires a level floor with anchor provisions for vacuum pump vibration
- Dedicated circuit rated for the selected 110 V or 220 V supply and vacuum pump draw
- Machine ships partially assembled; carriage rail alignment verified on site before first power-on
- Initial blade depth and oscillation frequency tuned to buyer’s material sample during commissioning
- Operator training covers tool head changeover, CCD mark teaching and emergency stop reset
- Wear parts kit includes oscillating blades, creasing wheel tips and vacuum table seal strips
Before You Send an Inquiry
Tell us the exact material type, thickness and maximum sheet size you intend to cut, along with your typical daily volume. Confirm your workshop voltage, frequency and preferred control language so the electrical build and software interface are locked before production. If you have existing nesting files or print-and-cut templates, share a sample set so we can verify CCD tracking and import compatibility before quoting.
Frequently Asked Questions
Q: How do I verify that the cutting thickness rating applies to my specific material?
A: Send a physical sample of your heaviest and most abrasive stock. We run a sample cutting report documenting blade type, oscillation frequency, cutting speed and edge quality achieved. The report confirms whether the ≤20 mm rating holds for your material density or whether a different tool head is needed.
Q: Which tool head should I choose between oscillating knife, drag knife and creasing wheel?
A: Oscillating knife suits fibrous and cellular materials like corrugated and foam. A creasing wheel compresses fold lines on carton without breaking the liner. Drag knife handles thin vinyl and sticker film. We recommend the combination based on your material list and send a sample cutting report before you commit.
Q: Will the CCD camera track my printed registration marks at full production speed?
A: The CCD auto-recognition system reads contrast between the mark and surrounding print. We test your actual printed sheet to confirm mark size, colour contrast and tracking reliability at your required cutting speed, and include the results in the pre-order sample report.
Q: Can I customise the voltage, plug type and software language before shipment?
A: Yes. Voltage is confirmed at 110 V or 220 V with your local frequency. Plug type and control panel language — English, Russian, Italian, Chinese or a custom option — are written into the production order so the machine arrives ready for immediate connection and operation.
Q: What does the sample cutting report cover and how do I submit my material?
A: Ship a flat sample of your production stock, at least A3 size. The report documents the tool head selected, cutting parameters used, edge and crease quality achieved, and any adjustments needed. This becomes the baseline configuration locked into your build order.


商品评价
Clear filtersThere are no reviews yet.