




Fast Shipping
Carrier information

20k products
Payment methods

24/7 Support
Unlimited help desk

2-day Delivery
Track or off orders
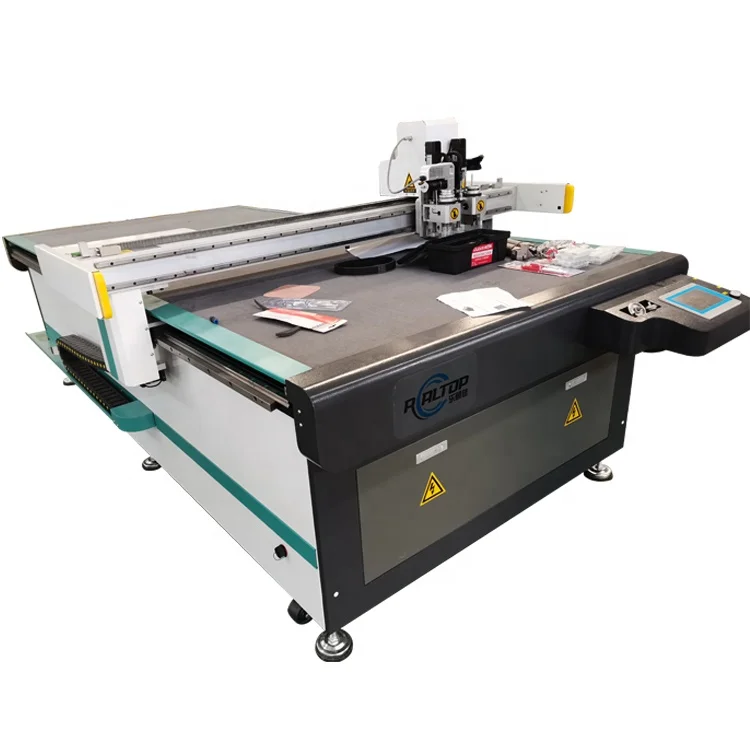
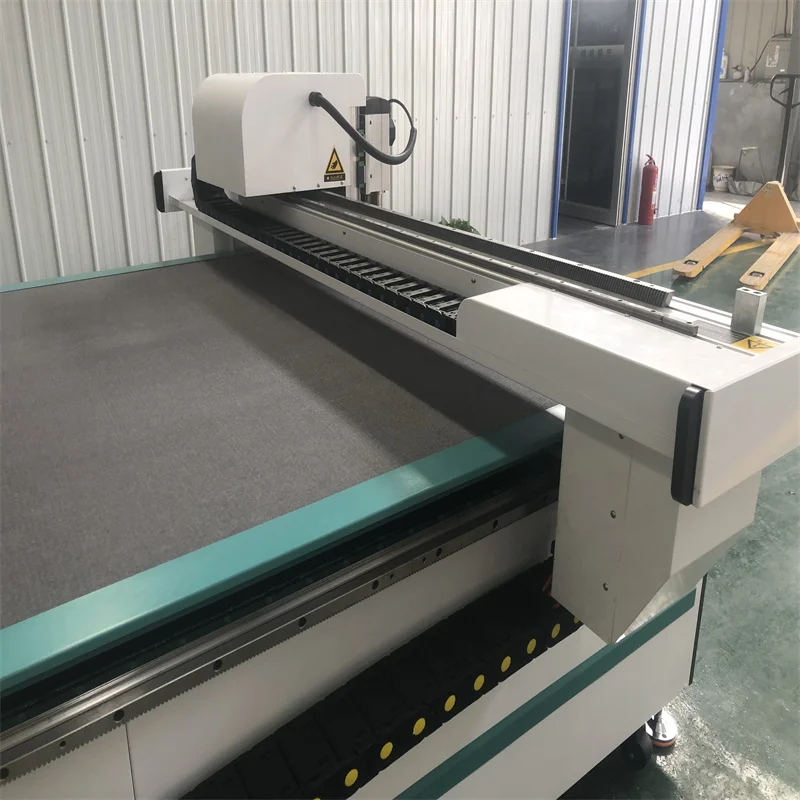
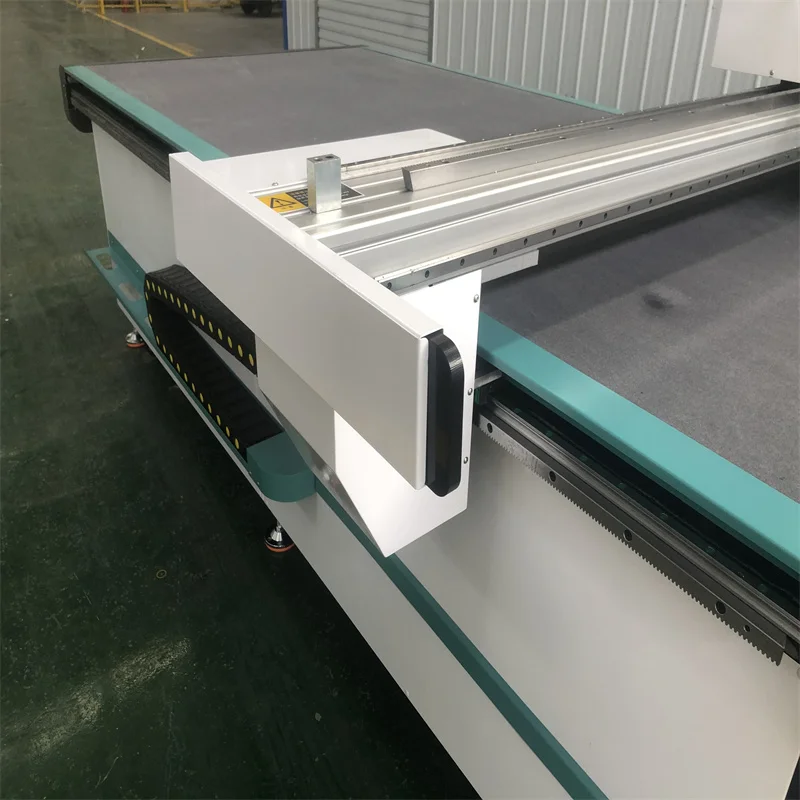
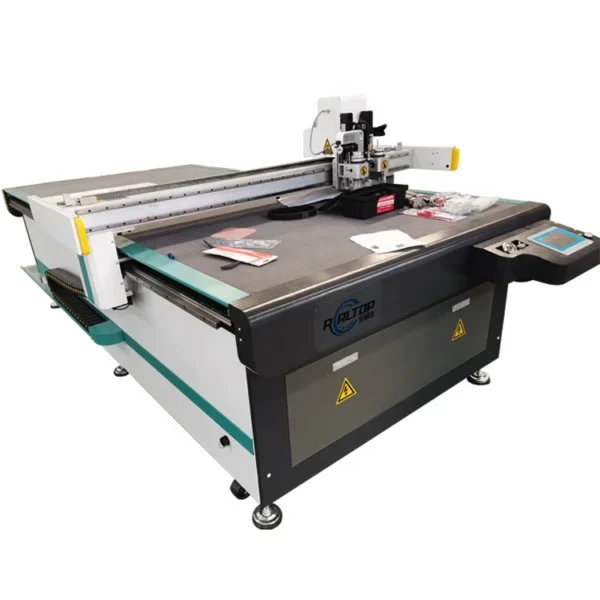
Swiss Knife and Vacuum Zoning — Tool heads and table zones configured after sample cutting on your actual corrugated board grade rather than sold on working area alone.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | CNC Corrugated Box Cutting Machine |
| Model | RT-D2516/RT-S2516 |
| Working Area | 1600 × 2500 mm |
| Machine Size | 3450 × 2300 × 1250 mm |
| Rated Power | 9 kW |
| Vacuum Pump | 7.5 kW |
| Working Table | Flat vacuum table with auto feeding |
| Multifunctional Head | Swiss imported knife — vibration full cutting, vibration half cutting, cursor location |
| Pneumatic Cutting Tool Max Thickness | 70 mm |
| Functions | Cutting, creasing and marking |
| Translational Velocity | 800–1200 mm/s |
| Cutting Speed | 200–800 mm/s (basis not stated in source — confirm with board grade and flute profile) |
| Repeated Accuracy | ≤0.1 mm |
| Transmission System | Digital servo motor, linear guide, synchronous belt, ball screw |
| Servo Motor | Japanese Yaskawa |
| Linear Rail | Taiwan Hiwin |
| Conveyor Belt | Germany imported |
| Instruction System | HP-GL compatible format |
| Safety Device | Infrared sensors |
| Voltage | 380V ± 10% |
| Standards | CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Carton sample making and short-run prototyping | Single, double and triple-wall corrugated board across common flute profiles |
| Corrugated box digital cutting | Custom flute formats without hard tooling commitment |
| Gift box and rigid packaging production | Grey board and composite board stock |
| Sticker and label contour cutting | Vinyl, adhesive-backed film and flexible sheet materials |
| Packaging die-line sampling | PVC, soft glass, silicon and rubber gasket sheets |
Why "Working Area" Is the Wrong Starting Point for CNC Corrugated Box Cutting Machine Specifications
Board grade and flute profile dictate the tool head, knife stroke and vacuum zone layout — not the table dimensions.
A machine specified purely on sheet size frequently arrives at a facility only to struggle with the actual material on the floor. I once configured an oscillating knife head for what the buyer described as standard single-wall corrugated, and the machine performed cleanly through sample runs at our Jinan workshop. When the same setup met their daily production stock — a heavier double-wall grade with high GSM liners — the knife crushed the flute peaks instead of shearing through them. The line sat idle for a full week while replacement tooling shipped. That gap between quoted specification and real material behaviour is where most packaging cutting projects stall. [NEED_CITE: corrugated flute profiles and crush resistance standards]
Tool Head Selection by Board Grade and Flute Type
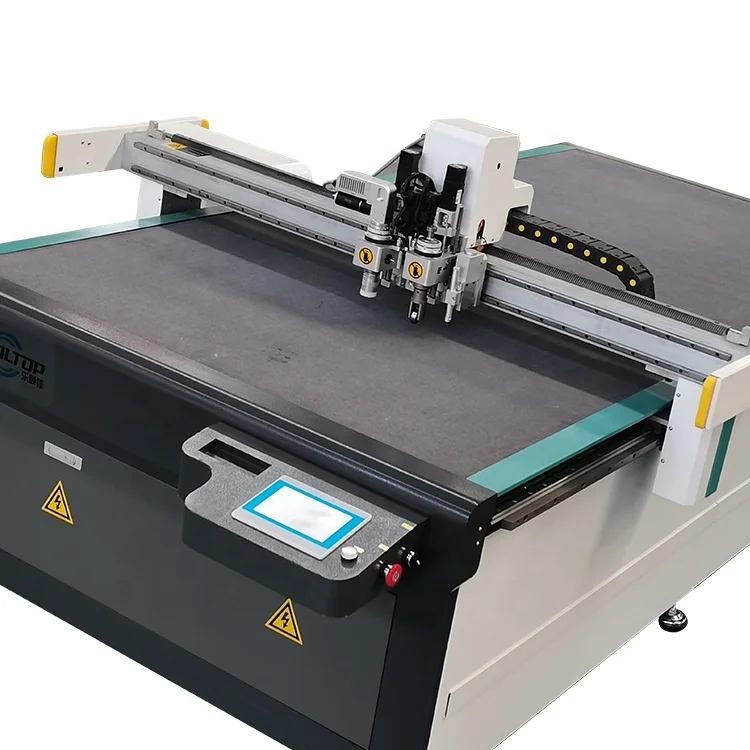
The Swiss imported oscillating knife on the RT-D2516/RT-S2516 performs both full cutting and half cutting in a single pass, which means crease lines and cut outlines register from the same tool station. For standard single-wall and E-flute stock, the vibration amplitude shears cleanly through the liner and medium without compressing the corrugation. Heavier double and triple-wall grades may require the pneumatic tool head — rated to 70 mm maximum thickness — to push through the combined board depth without stalling the stroke. This CNC corrugated box cutting machine configuration is confirmed only after a sample cutting run on the buyer’s own board, not assumed from a catalogue chart.
Vacuum Table Zoning for Small Carton Blanks
A 7.5 kW vacuum pump pulls air through the flat table surface to pin the board during high-speed travel. The problem arises when the blank being cut is much smaller than the full 1600 × 2500 mm bed: unsealed zones leak suction and the blank lifts under knife drag. Zoning the table into independently valved sections directs vacuum only to the area beneath the active cut, holding narrow carton sleeves and small insert blanks flat at translational velocities up to 1200 mm/s. [NEED_CITE: vacuum hold-down principles for flatbed digital cutting]
Reading the Specs That Actually Affect Cut Quality
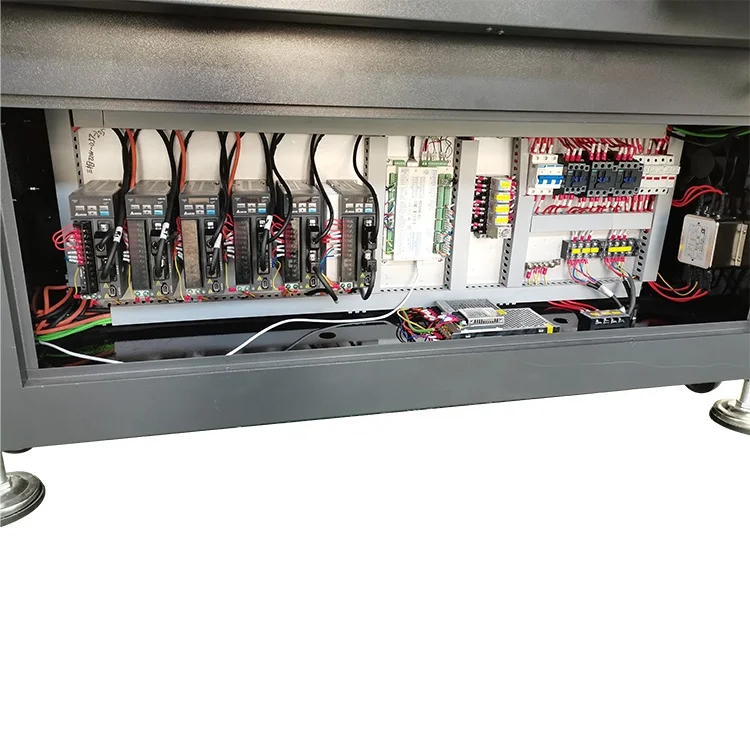
Repeated accuracy of ≤0.1 mm across the working area depends on the combination of Taiwan Hiwin linear rails and Japanese Yaskawa servos driving the gantry through ball screws and synchronous belts. In packaging sample making, that tolerance keeps crease lines aligned with cut edges so folding cartons close squarely. The HP-GL compatible instruction system accepts files from mainstream packaging CAD packages, avoiding a situation where the buyer’s designer exports a die-line only to find the controller cannot parse it. Auto feeding with the Germany-imported conveyor belt moves successive sheets onto the table for uninterrupted runs, and the infrared sensor array stops travel if an operator crosses the safety perimeter during production.
The Cost of Skipping a Sample Cutting Run
When a buyer commits to a tool head and vacuum layout without testing on their actual board, the consequences show up on the first production day. Ragged cut edges force secondary trimming. Crushed flute peaks weaken the box compression strength and cause customer rejections. Insufficient vacuum zoning on small blanks means re-cutting lifted sheets. Each of these outcomes adds downtime that a sample report would have prevented before the machine left the factory. [NEED_CITE: edge quality requirements in corrugated packaging converting]
Why Source This CNC Corrugated Box Cutting Machine from Realtop
The design team and core factory in Jinan cover both knife and laser cutting platforms, so the cutting method is matched to the material rather than forced onto one machine type. Tool head and table configuration is specified per board grade, flute profile and production volume after physical sample testing. Software compatibility with the buyer’s existing CAD or nesting workflow is confirmed before order. Voltage, plug type and control language are documented and verified before shipment. In-house production means configuration changes happen on the factory floor, not through a third-party integrator.
Documentation & Verification
- Machine specification sheet listing confirmed tool head and vacuum zone layout
- Electrical schematic with voltage and frequency matched to your facility supply
- Sample cutting report run on your corrugated board grade and flute type
- Software licence and HP-GL file format compatibility confirmation note
- Factory test record with dimensional accuracy verification before dispatch
- Spare parts list covering knives, creasing wheels and vacuum seals
Installation, Commissioning & Support
- Floor space planning around the 3450 × 2300 × 1250 mm machine footprint plus material staging area
- Dedicated 380V ± 10% circuit sized for the combined 9 kW machine and 7.5 kW vacuum pump load
- Gantry and vacuum table assembly on-site with level verification across the 1600 × 2500 mm bed
- First-run parameter tuning — knife stroke, oscillation frequency and vacuum zone mapping — on your board stock
- Operator training covering tool head changeover between cutting, creasing and marking functions
- Scheduled maintenance intervals for Hiwin rail lubrication and conveyor belt tension checks
What We Need to Configure Your Machine
Send us the specific corrugated board grades and flute types you run daily, along with typical blank dimensions and your target daily sample volume. Confirm the voltage and frequency at your facility, the control language your operators require, and whether your existing design workflow exports in HP-GL or a format we need to validate. If you can ship a stack of your actual production board to our workshop, we will run a sample cutting and return the finished blanks with a configuration report before you commit to an order.
Frequently Asked Questions
Q: What board thickness and flute type can this table cut, and what determines the stated speed range?
A: The RT-D2516/RT-S2516 handles single through triple-wall corrugated board using the oscillating knife for standard flutes and the pneumatic tool for stock up to 70 mm thick. The 200–800 mm/s cutting speed depends on board density and flute profile — the only reliable way to confirm throughput for your material is a sample cutting run before order.
Q: Which tool head suits corrugated board — oscillating knife, drag knife or creasing wheel?
A: The Swiss oscillating knife handles full cutting and half cutting for crease-and-cut in one pass on most flute profiles. A drag knife suits thin card and sticker stock. The creasing wheel scores fold lines on heavy grey board. We recommend the combination after testing your actual material.
Q: Is CCD camera contour recognition available for printed carton registration?
A: CCD camera positioning can be specified as an option for tracking printed registration marks on pre-printed corrugated sheets. The camera must be validated against your specific print contrast and mark size at production speed before the configuration is locked in.
Q: How does vacuum zoning prevent small carton blanks from lifting?
A: The 7.5 kW vacuum pump feeds independently valved zones across the flat table. For blanks smaller than the full 1600 × 2500 mm bed, only the active zone is opened, concentrating suction beneath the cut area and preventing lift at translational speeds up to 1200 mm/s.
Q: What electrical and language details are confirmed before shipment?
A: Voltage, plug type and control panel language are documented in the electrical schematic before production begins. The standard supply is 380V ± 10%, and alternative voltages are configured to match your facility. A written confirmation sheet is signed off before the machine crates close.


商品评价
Clear filtersThere are no reviews yet.