

Fast Shipping
Carrier information

20k products
Payment methods

24/7 Support
Unlimited help desk

2-day Delivery
Track or off orders
Tool Head and Table Configuration — matching oscillating knife, drag knife or creasing wheel to material thickness and edge quality requirements before the machine is built, not after it arrives.
Technical Specifications
| Parameter | Value |
|---|---|
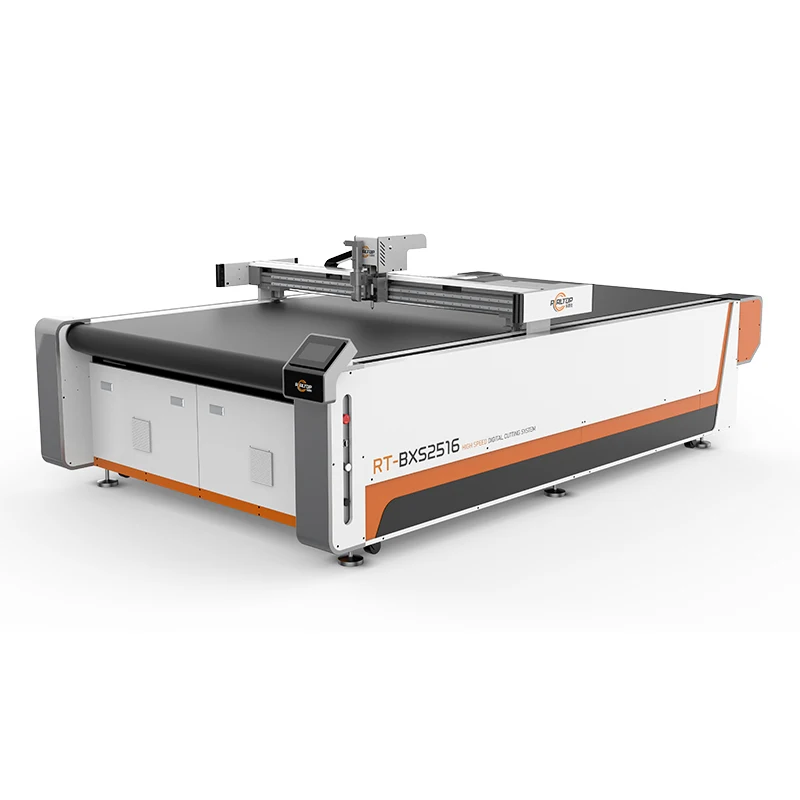
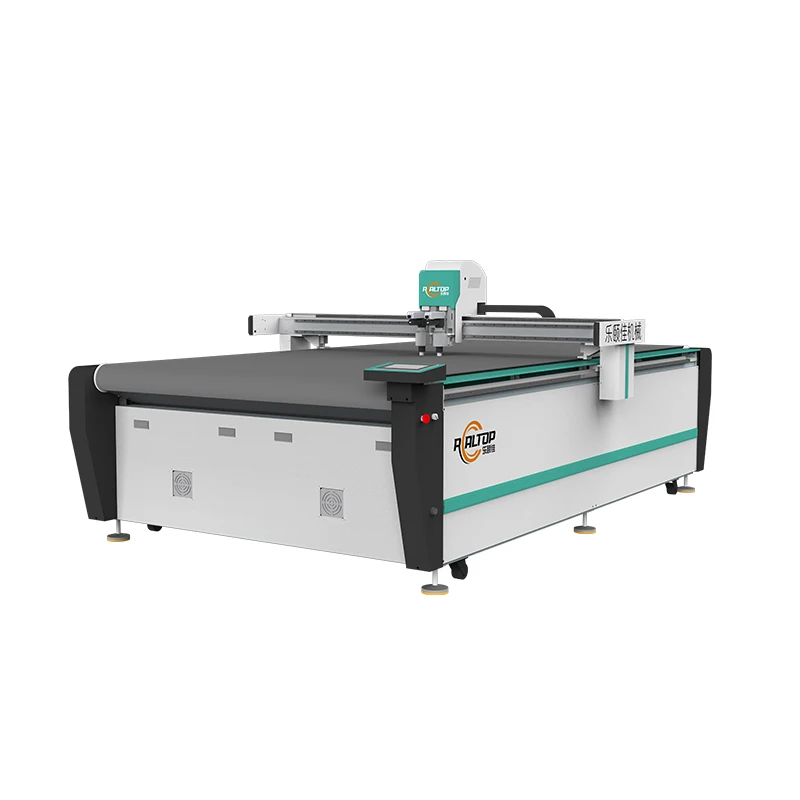
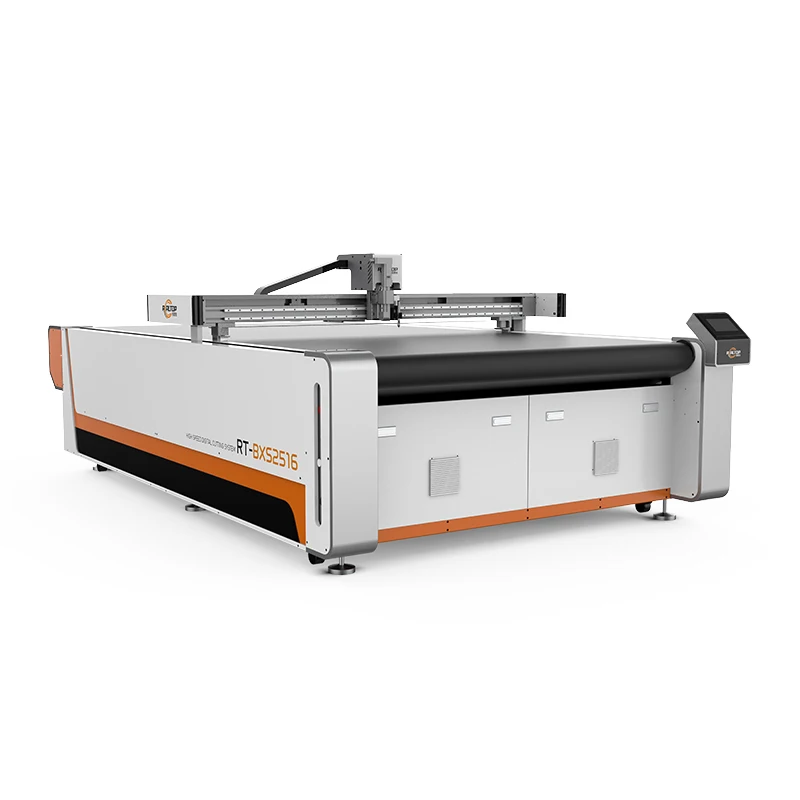
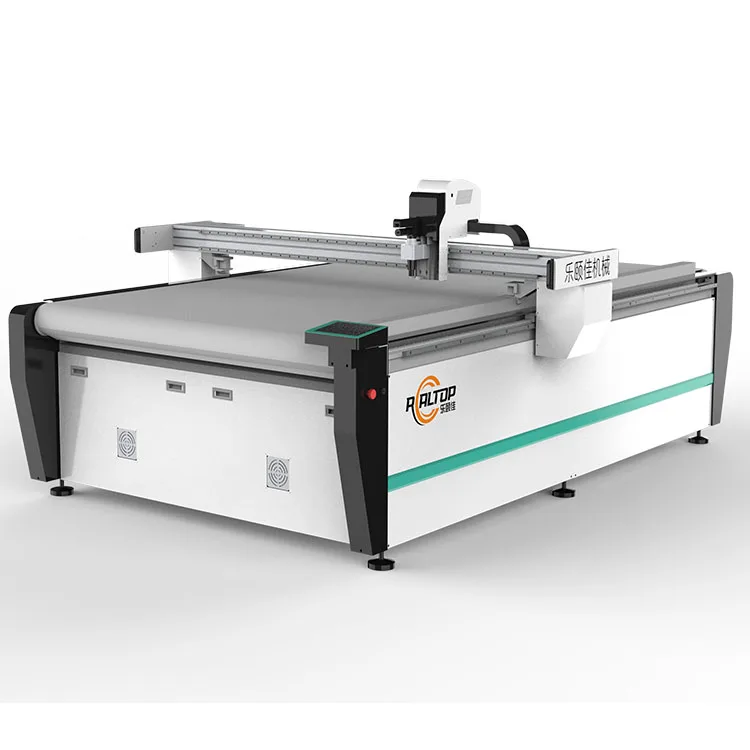
| Model | RT-D2516 / RT-S2516 |
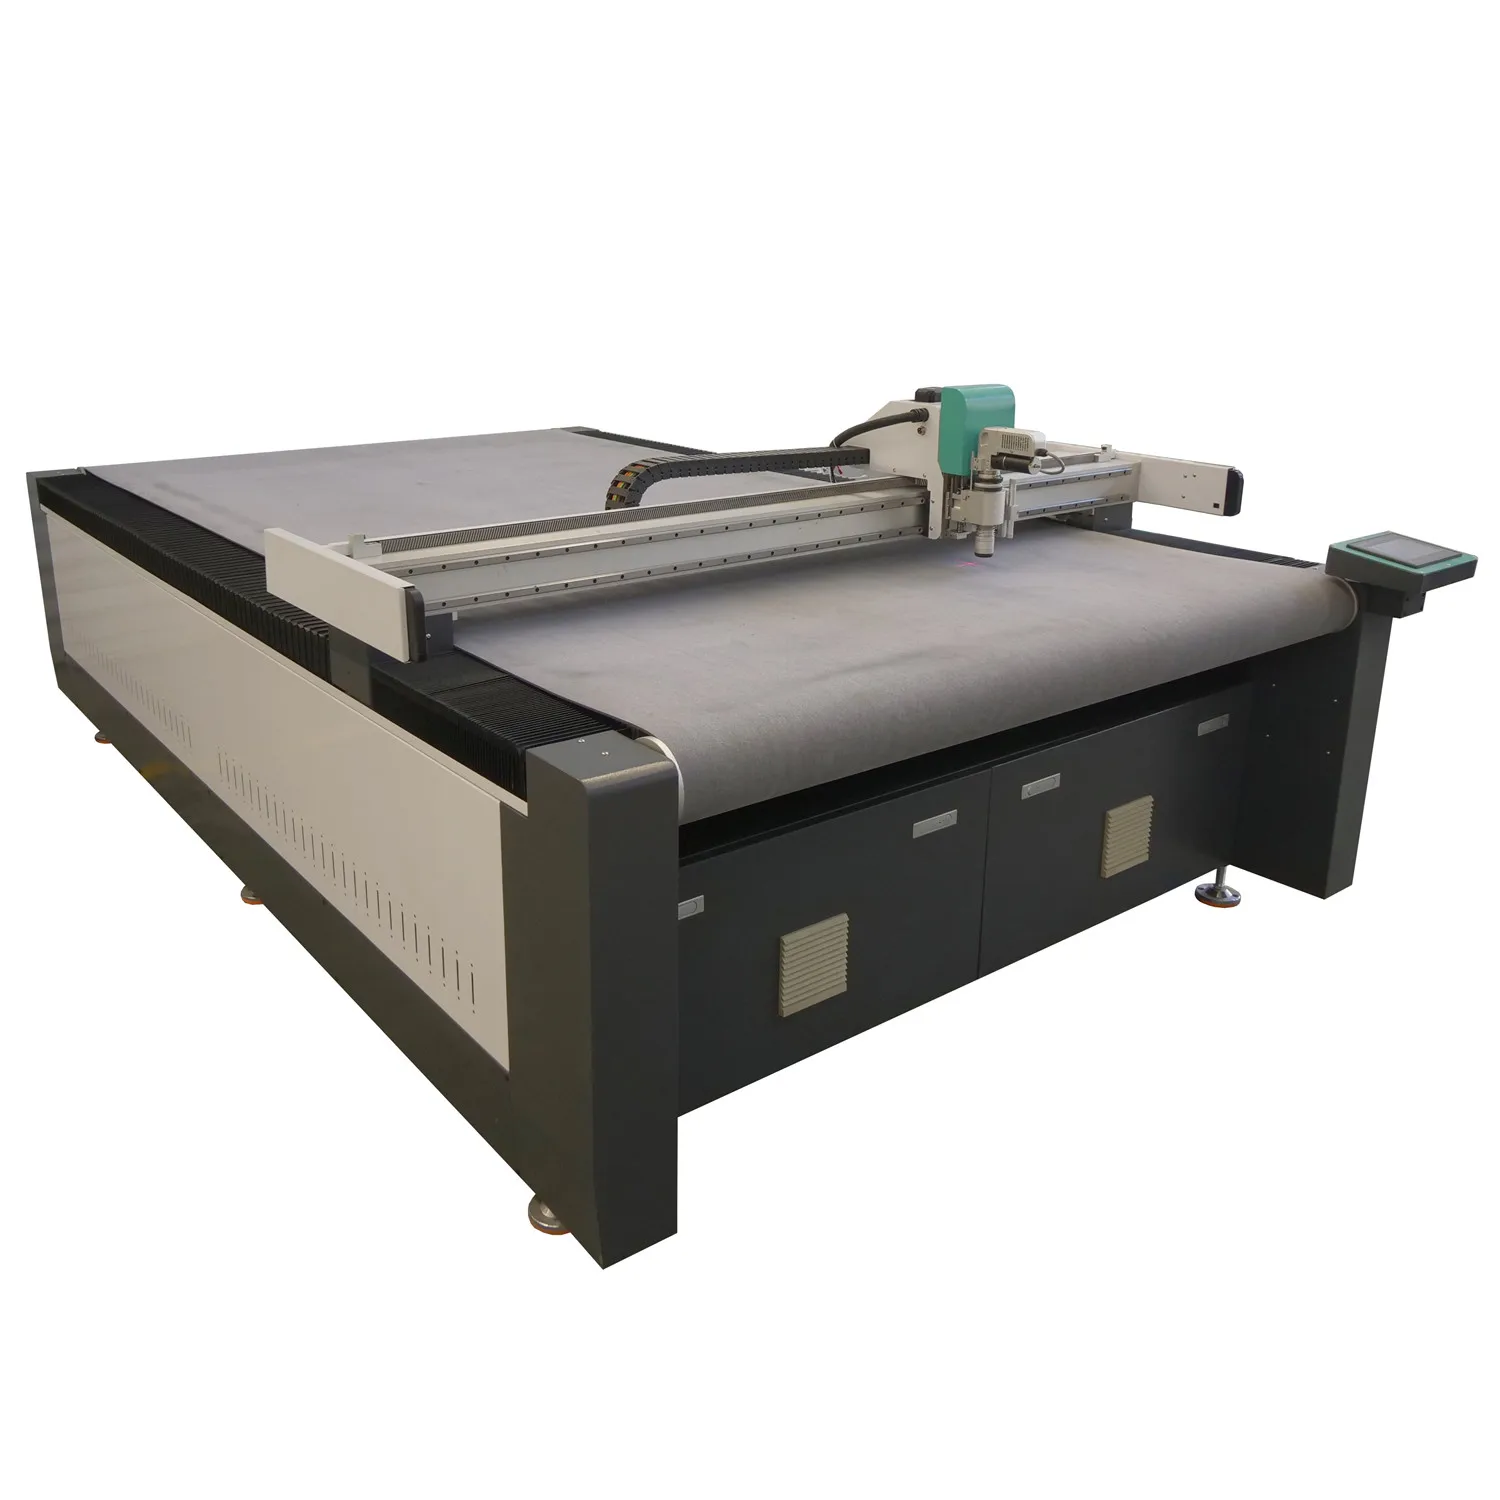
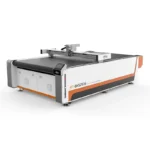
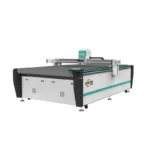
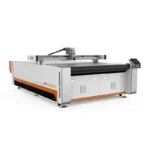
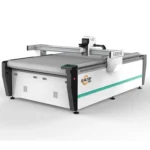
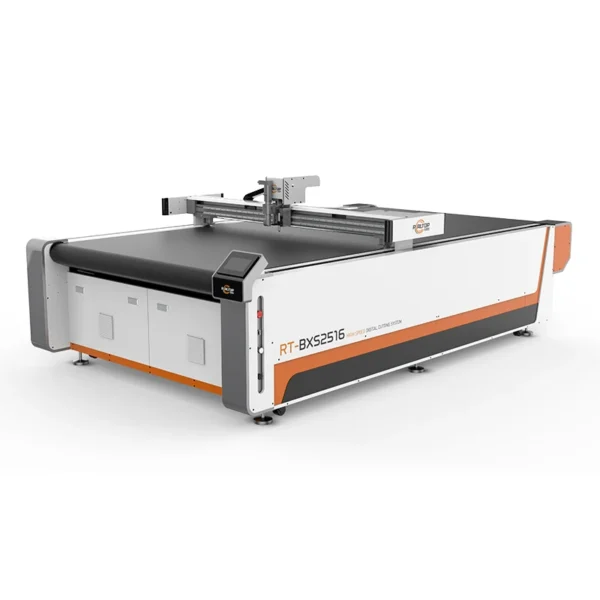
| Product Type | CNC Oscillating Knife Cutting Machine |
| Working Area | 1600 × 2500 mm |
| Machine Size | 3450 × 2300 × 1250 mm |
| Rated Power | 9 kW |
| Vacuum Pump | 7.5 kW |
| Voltage | 380 V ± 10 % |
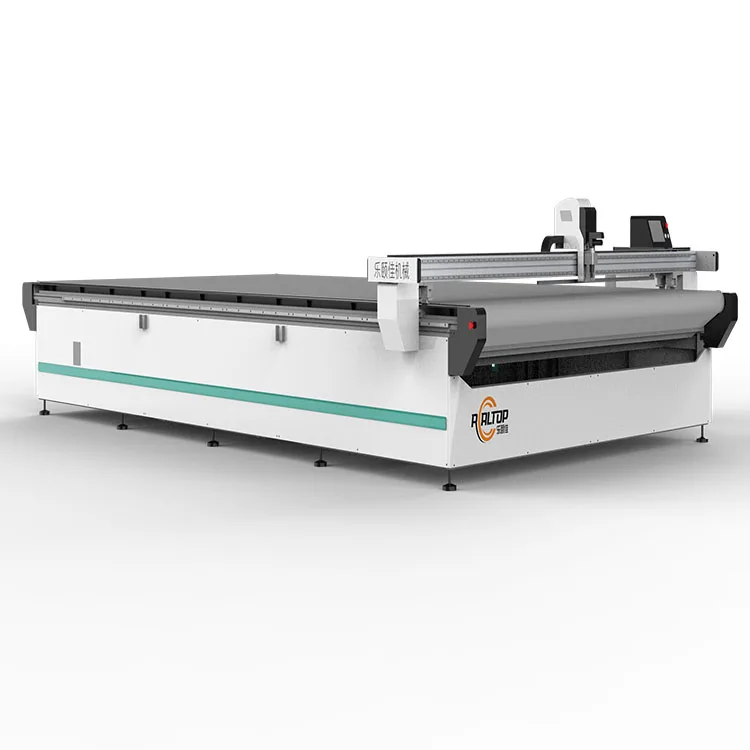
| Table Type | Flatbed (RT-D2516) / Auto-feeding conveyor (RT-S2516) |
| Translational Velocity | 800–2000 mm/s |
| Cutting Speed | 200–800 mm/s (varies by material type and thickness) |
| Max Cutting Thickness | ≤ 100 mm (varies with material) |
| Repeated Accuracy | ≤ 0.1 mm |
| Transmission System | Digital servo motor, linear guide, synchronous belt, ball screw |
| Servo Motor | Delta (Panasonic optional) |
| Guide Rail | Taiwan Hiwin |
| Conveyor Belt | Germany imported (RT-S2516) |
| Tool Head Options | Oscillating knife, pneumatic knife, high-power vibrating knife, circular knife, V-cutting knife, drag knife, creasing wheel, dotted line knife, punching, brush |
| Visual Positioning Options | Small CCD camera mark-point, panoramic camera recognition, projection positioning |
| Instruction Format | HP-GL compatible |
| Software File Formats | PLT, DXF, AI |
| Control Panel | Touch screen, multi-language (English, Russian, Italian, Chinese; others customizable) |
| Frame Construction | Thick-walled seamless steel, high-temperature tempering, CNC machining center finished |
| Vacuum Table Surface | Magnesium-aluminum alloy, fluorocarbon PVDF powder spraying, anodic oxidation, hard oxidation |
| Safety Devices | Infrared sensors, anti-collision, emergency stop |
Application Suitability
| Application | Material or Output |
|---|---|
| Garment and clothing production | Single-layer and multi-layer woven fabric, knit textile, technical cloth |
| Footwear and leather goods | Natural leather, PU synthetic, sponge composite leather |
| Automotive interiors | PU foam, EVA, composite leather panels, headliner fabric |
| Carpets and floor mats | Tufted carpet, rubber-backed mat, non-woven floor covering |
| Packaging sample making | Corrugated cardboard, folding carton stock, adhesive film |
| Sealing pads and gaskets | Non-asbestos fiber sheet, rubber, PTFE, graphite composite |
| Sports and outdoor products | Neoprene, nylon laminate, mesh textile |
| Graphic advertising and printing | Vinyl, banner PVC, heat-transfer film, sticker stock |
| Composite materials | Carbon fiber prepreg, fiberglass cloth, aramid laminate |
Why the Right Knife Type Matters More Than Working Area Alone
Buyers frequently specify a CNC oscillating knife cutting machine based on table size, only to discover at commissioning that the installed tool head cannot hold a clean edge on their actual material or that cutting speed must be reduced to avoid ragged cuts.
The knife must be matched to the material before the purchase order, not swapped after delivery.
I spent years on the assembly floor in Jinan before moving to technical sales. One year we configured a vibrating knife unit for an automotive interior customer based on sample parts they sent, which were single-layer PU. When the machine arrived, their real production involved multi-layer composite leather well over the thickness we had validated. Their daily throughput ended up at roughly half the expected volume. That job changed how I approach every quotation — I now insist on receiving the buyer’s actual production material for a trial cut before any specification is finalized [NEED_CITE: material thickness and tool head compatibility in oscillating knife cutting].
Multi-Tool Head Selection by Material
The head carriage on the RT-D2516 and RT-S2516 accepts oscillating, pneumatic, drag, circular and V-cutting knives along with creasing wheels and punch tools. A garment shop cutting single-layer silk needs a high-frequency oscillating knife for clean edges without fraying, while a gasket producer working non-asbestos fiber sheet benefits from a drag knife that scores and separates without crushing the material. Selecting the correct tool is part of the CNC oscillating knife cutting machine specifications discussion at the inquiry stage, not an afterthought.
Vacuum Table Zoning for Small-Part Stability
The magnesium-aluminum alloy table surface carries PVDF coating and hard anodization to resist wear from abrasive composites. More importantly, the table is divided into independently controlled vacuum zones. When cutting small gasket pieces or shoe upper components, only the active zone under the material needs suction, preventing lift at high translational speeds. A poorly zoned table causes parts to shift mid-cut, producing scrap and forcing operators to slow the machine down [NEED_CITE: vacuum zoning requirements for small-part oscillating knife cutting].
Reading the Specs That Actually Affect Your Output
The 9 kW rated power covers servo drives, spindle and control; the 7.5 kW vacuum pump is a separate circuit that must be accounted for in your facility electrical plan. Hiwin linear guides paired with Delta or Panasonic servos deliver the ≤ 0.1 mm repeatability that pattern nesting software relies on for tight piece spacing. Cutting speed is listed at 200–800 mm/s — the lower end applies to dense composites like carbon fiber prepreg, while woven fabric on the auto-feeding RT-S2516 can approach the upper range. Translational velocity of up to 2000 mm/s governs non-cutting moves between cut paths and directly affects cycle time on complex nests. The HP-GL compatible instruction system accepts PLT, DXF and AI files, so your existing nesting workflow does not need replacement.
What Happens When Configuration Is Skipped
Choosing the wrong knife for a compressible foam produces crushed edges that fail dimensional inspection. A vacuum table with a single zone leaves small sticker or gasket parts lifting at the trailing edge. Specifying CCD camera positioning when your workflow actually uses projection-guided manual layup means you paid for hardware that never runs. Each of these errors is preventable, yet they appear regularly when a machine is ordered on working area and price alone [NEED_CITE: common configuration errors in CNC knife cutting procurement].
Why Buyers Come Back for a Second Machine
Every RT-D2516 and RT-S2516 is configured from the tool head outward — the buyer’s material dictates which knife, which positioning system and which vacuum zone layout ships with the machine. In-house design and production cover both knife and laser cutting technology, so if a material responds better to CO2 laser sealing than knife cutting, the conversation happens before the order is placed. Sample cutting on the buyer’s own material is completed and documented before commitment. Software file compatibility is verified against the buyer’s nesting files during the quotation phase. Voltage, plug type and control language are confirmed line-by-line before production begins [NEED_CITE: pre-shipment specification verification practices for industrial cutting equipment].
Documentation & Verification
- Machine specification sheet listing every tool head and positioning option included in your build
- Electrical schematic confirming 380 V ± 10 % wiring, breaker ratings and vacuum pump circuit
- Sample cutting report on your material showing achieved edge quality and cutting speed
- Tool head and vacuum table zone configuration list matched to your material type
- Operation and maintenance manual with spare parts list and recommended consumable intervals
- Software license and file format compatibility note for PLT, DXF and AI workflows
Installation, Commissioning & Support
- Foundation must be level within tolerance across the 3450 × 2300 mm footprint to maintain frame flatness
- Dedicated 380 V circuit sized for combined 9 kW machine and 7.5 kW vacuum pump loads
- Machine ships as single frame; Hiwin guides and servo motors are pre-aligned at factory
- First-power commissioning includes vacuum zone calibration and cutting speed validation on your material
- Touch screen control configured in your operator language before the unit leaves Jinan
- Spare oscillating knife blades, drag knife tips and vacuum seals included in initial shipment
Before You Request a Quote
To configure the right machine for your line, we need your material type, single-sheet dimensions, maximum thickness and whether you cut single-layer or multi-layer stacks. Tell us your daily volume target and whether your workflow uses printed registration marks or projection-guided layup. Share your local voltage and frequency standard plus preferred control panel language so the electrical and software package is locked before production.
Frequently Asked Questions
Q: How do I choose between an oscillating knife and a drag knife for my material?
A: Oscillating knives cut through compressible and layered materials like foam, fabric and composite leather with a high-frequency vertical stroke that prevents edge crushing. Drag knives are better suited for thin, non-compressible sheets such as vinyl, sticker film and gasket fiber where a pulled blade produces a clean score. We run trial cuts on your actual material to confirm which tool delivers the required edge quality before finalizing the tool head list.
Q: Is CCD camera positioning or projection positioning better for my workflow?
A: CCD camera positioning reads printed registration marks and adjusts the cut path automatically, which suits high-volume contour cutting of pre-printed fabric or signage. Projection positioning displays the cut layout onto the material surface for manual alignment, fitting short-run sample making and nesting on unprinted stock. Both options are available on the RT-D2516 and RT-S2516 and can be evaluated during the sample cutting stage.
Q: Will small parts stay flat on the vacuum table during high-speed cutting?
A: The magnesium-aluminum alloy table is divided into independent vacuum zones. Only the zone under the active cutting area needs to be engaged, concentrating suction on the workpiece and preventing small gaskets, shoe components or sticker parts from lifting at translational speeds up to 2000 mm/s. Zone layout is specified during the quotation to match your typical part size range.
Q: What electrical and language details must I confirm before the machine ships?
A: The standard supply is 380 V ± 10 %, and the combined machine and vacuum pump load requires a dedicated circuit. Plug type, cable entry direction and control panel language — available options include English, Russian, Italian and Chinese with custom languages on request — must all be confirmed at order so the electrical schematic and software package match your facility and operators.
Q: What is the difference between the RT-D2516 flatbed and the RT-S2516 auto-feeding model?
A: The RT-D2516 uses a flat vacuum table where the operator loads and unloads material manually, suited for rigid or semi-rigid sheets and short production runs. The RT-S2516 adds a German-imported conveyor belt feeding system that advances roll or long-sheet material automatically, reducing handling time for high-volume fabric and textile cutting. Both models share the same 1600 × 2500 mm working area and tool head options.


商品评价
Clear filtersThere are no reviews yet.