
Fast Shipping
Carrier information

20k products
Payment methods

24/7 Support
Unlimited help desk

2-day Delivery
Track or off orders
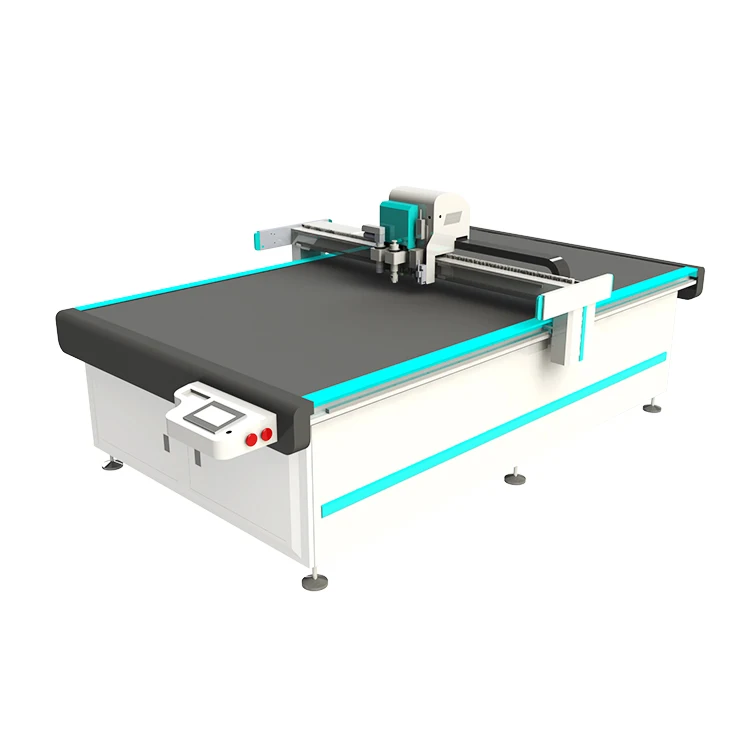
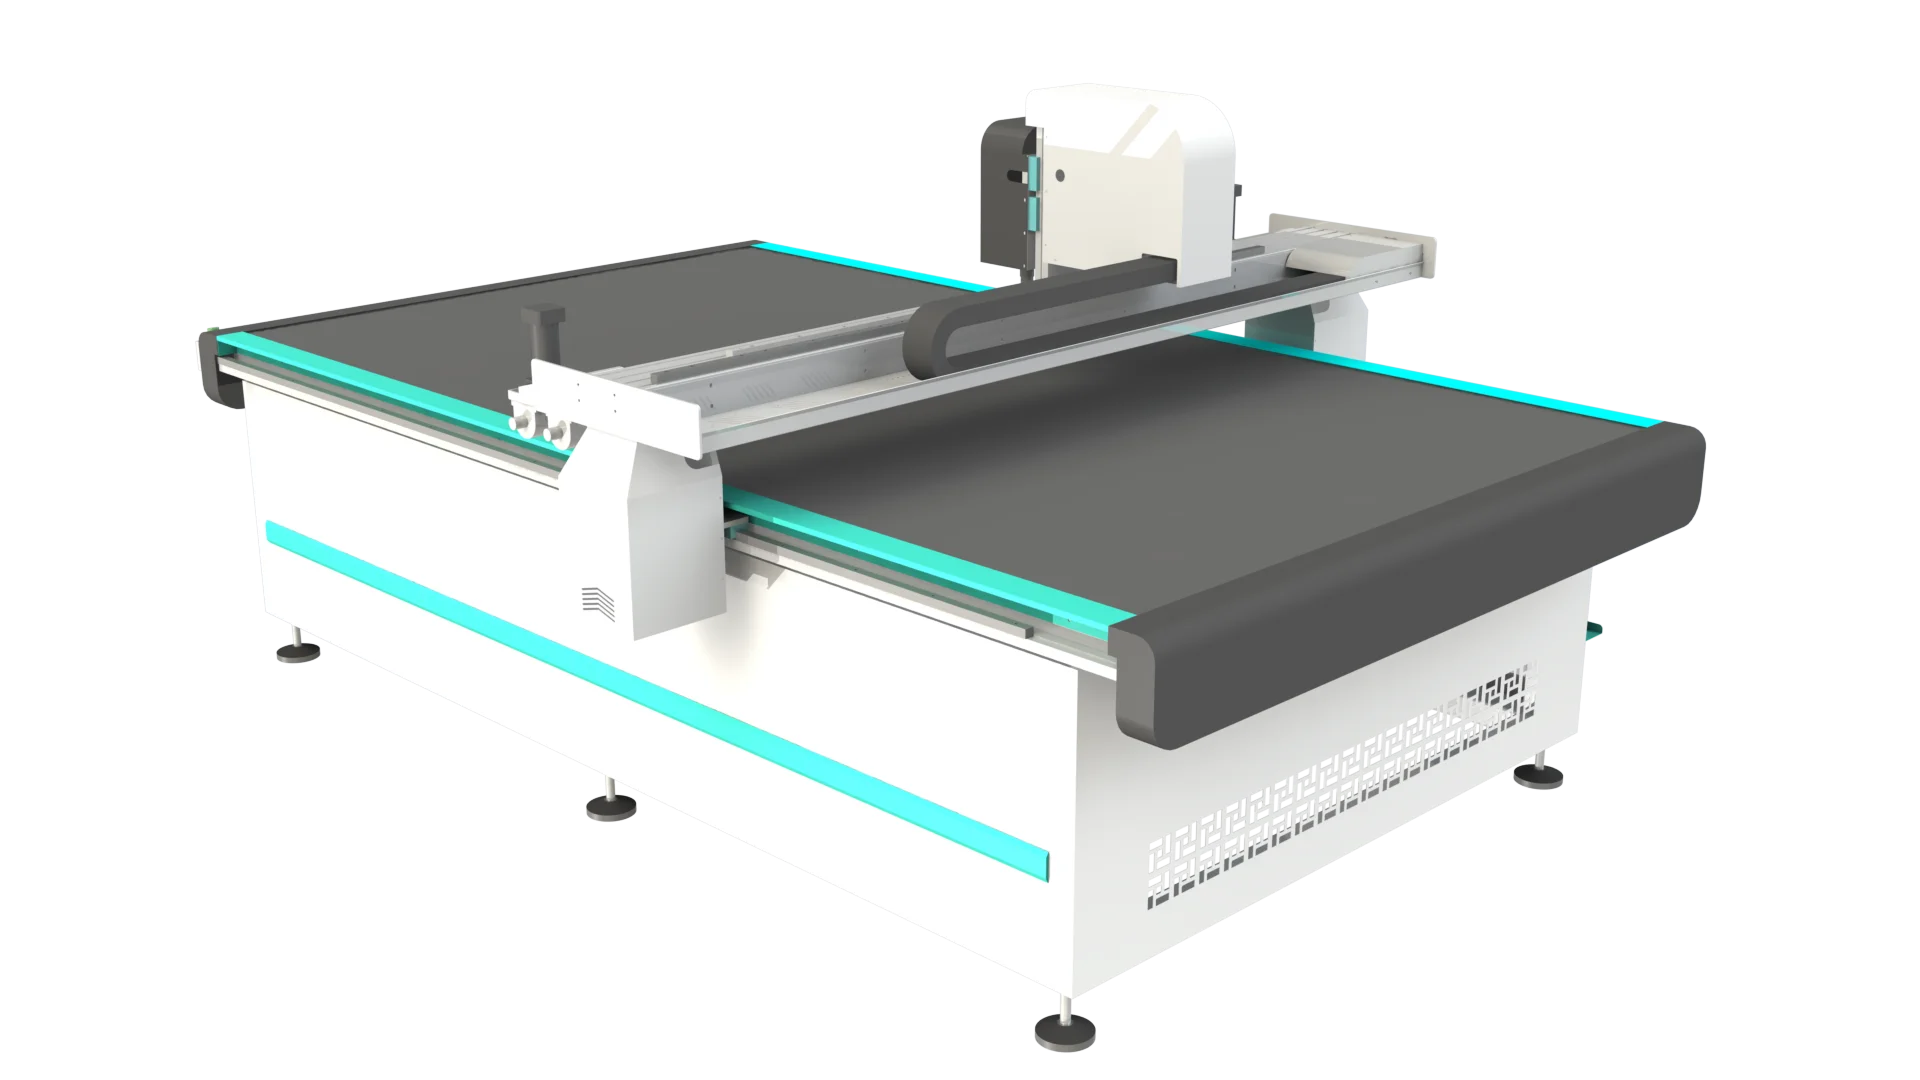
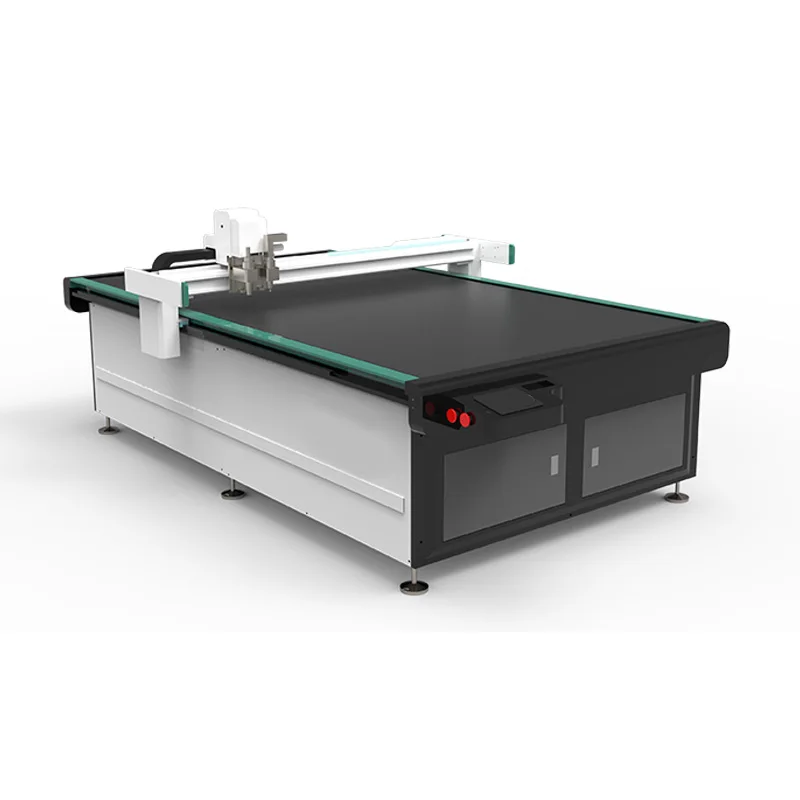
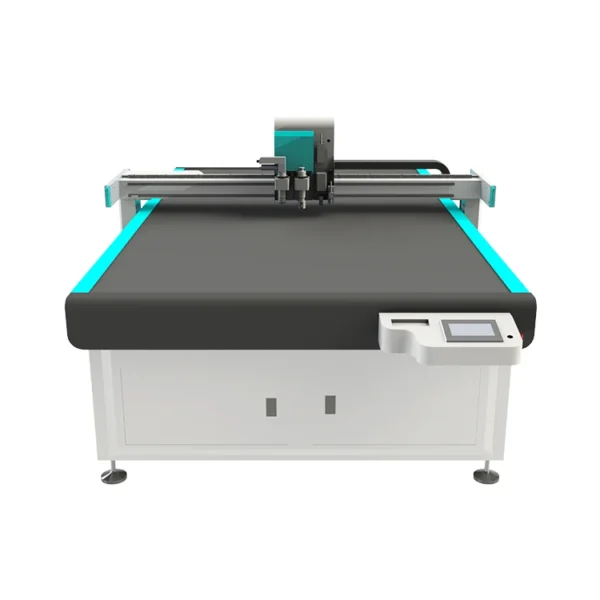
In-house knife and laser design — Tool head, vacuum zone and voltage configured per material and production volume before the RT-D2516/RT-S2516 CNC Oscillating Knife Cutting Machine is scheduled for build.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | CNC Oscillating Knife Cutting Machine |
| Model | RT-D2516/RT-S2516 |
| Working Area | 1600×2500mm |
| Overall Dimensions (L×W×H) | 3450×2300×1250mm |
| Rated Power | 11 kW |
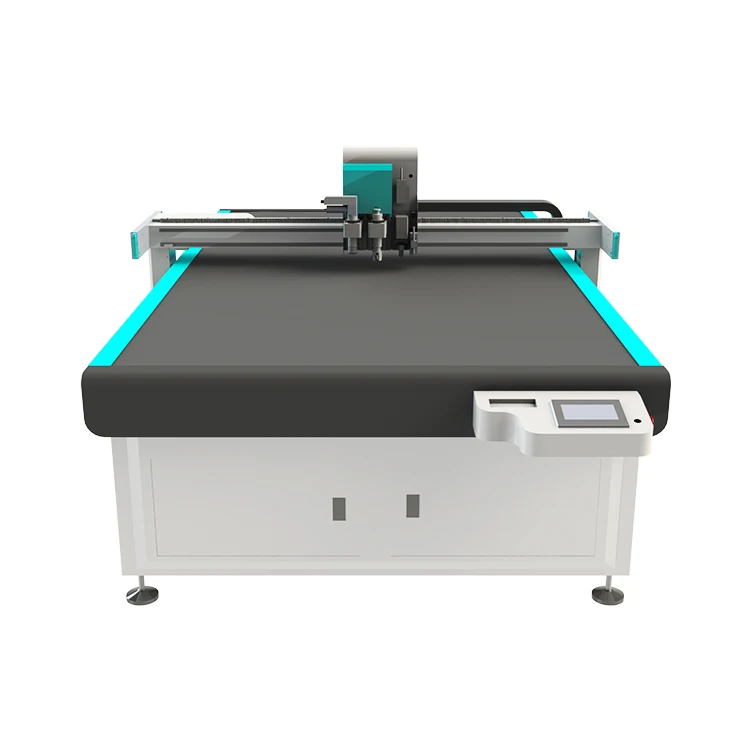
| Table Type | Flat working table with vacuum and conveyor belt |
| Tool Head | Swiss imported knife with vibration full cutting, half cutting and cursor location |
| Safety Device | Infrared sensors |
| Translational Velocity | 800–1200 mm/s |
| Cutting Speed | 200–800 mm/s (according to different cutting materials) |
| Repeated Accuracy | ≤0.1 mm |
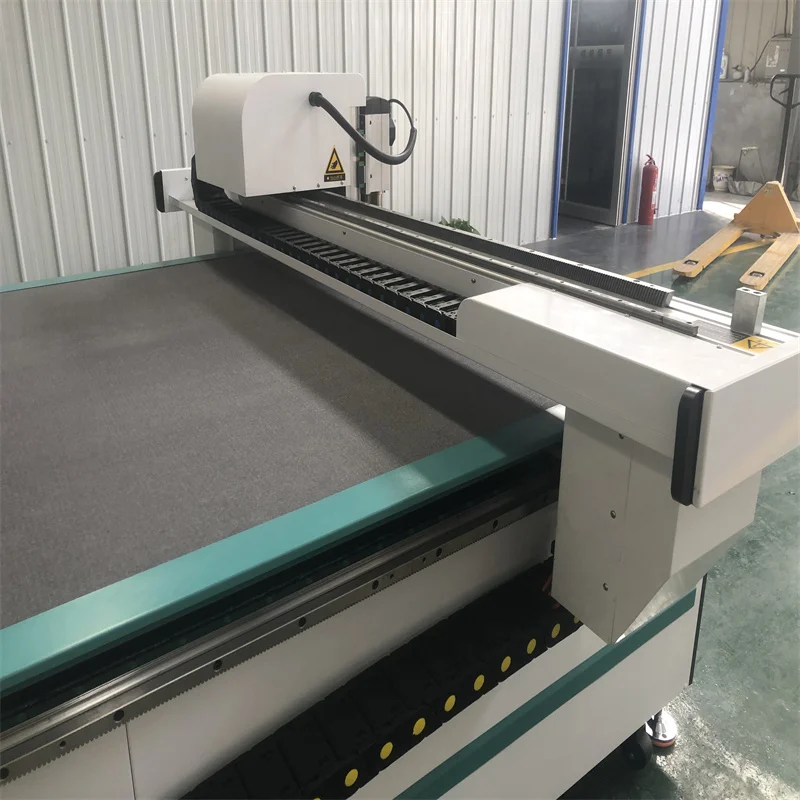
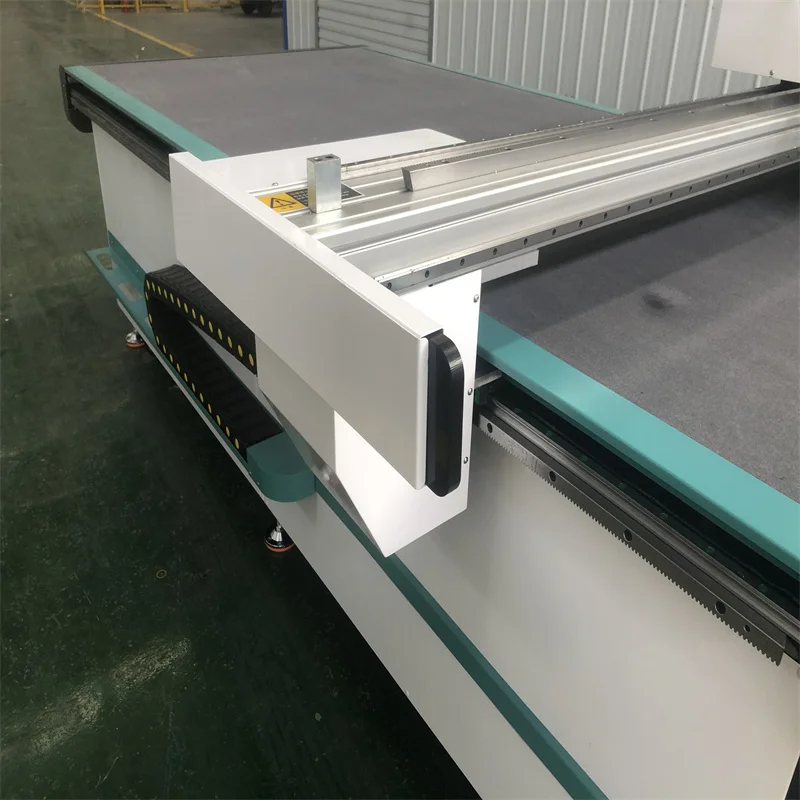
| Transmission System | Digital servo motor, linear guide, synchronous belt, ball screw |
| Instruction System | HP-GL compatible format |
| Voltage | 380V±10% |
| Servo Motor | Japanese Yaskawa |
| Linear Guide | Taiwan Hiwin rail |
| Vacuum Pump | 7.5 kW |
| Conveyor Belt | Germany imported |
| Feeding | Auto feeding system |
| Certification | CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Packaging and carton sample making | Corrugated board, folding carton stock, greyboard for die-free prototyping |
| Leather and footwear production | Natural and synthetic hides, composite leather, sponge-backed materials |
| Garment and textile cutting | Flexible fabrics, multi-layer cloth stacks on conveyor-fed table |
| Gasket and foam fabrication | PVC, soft glass, silicon, rubber and sponge composite sheets |
| Automotive interior trimming | Soft trim composites and flexible panel materials |
Why Voltage and Frequency Must Be Confirmed Before the Order
The electrical specification is set at the factory, not adapted on the shop floor.
I once watched a brand-new oscillating knife table sit idle for over three weeks in a South American carton plant because the machine left the factory wired for 380V/50Hz while the facility ran on 220V/60Hz. A step-up transformer had to be sourced locally, and every servo parameter on the Yaskawa drives needed recalibration once power was finally applied. The delay cost the plant an entire sampling cycle [NEED_CITE: voltage and frequency standards by export market]. When buyers focus only on the working area and overlook the supply voltage, the CNC Oscillating Knife Cutting Machine specifications on paper mean very little at installation. Matching the RT-D2516/RT-S2516 to the local grid is the first step in the quotation, not the last.
Oscillating, Drag and Creasing Tool Options by Material
The multifunctional head on the RT-D2516/RT-S2516 carries a Swiss imported blade that performs vibration full cutting, half cutting and cursor location without a tool change. For corrugated board sample making, the oscillating action shears through flute walls cleanly, whereas a static drag knife would crush the medium and leave a ragged edge. When the same table is asked to score greyboard fold lines, a creasing wheel attachment replaces the knife path and presses a precise groove without cutting through the sheet. This head-swapping flexibility lets packaging sample makers move from a B-flute carton blank to a vinyl sticker contour on the same CNC Oscillating Knife Cutting Machine within minutes.
Vacuum Zoning and the Small-Part Lift Problem
The 7.5 kW vacuum pump pulls air through the flat table in configurable zones, and the Germany-imported conveyor belt feeds sheet stock forward automatically. A full sheet of corrugated board covers most zones and holds itself flat under the knife head even at 1200 mm/s translational velocity. The challenge appears once nesting software arranges dozens of small carton blanks across the bed: uncovered zones leak vacuum, and the remaining suction may not resist the air shear generated by a fast-moving tool head [NEED_CITE: vacuum hold-down principles for flatbed digital cutters]. Zone layout must therefore be matched to the typical nesting pattern, not just the sheet outline, before the table ships.
Reading the Specs That Matter on the Floor
The ≤0.1 mm repeatability figure comes from Yaskawa digital servo motors driving Taiwan Hiwin linear rails, a combination that keeps the knife tip on the programmed contour pass after pass. On printed packaging blanks, that positional stability is what allows a CCD camera system to track registration marks at production speed and correct the cut path in real time. The HP-GL compatible instruction system accepts files directly from common packaging CAD suites, so sample makers do not need to re-draw carton geometry in a proprietary editor. Cutting speed is listed as 200–800 mm/s depending on material density and thickness, a realistic spread that accounts for the difference between slicing thin vinyl and working through a double-wall corrugated sheet. Translational velocity — the speed of the gantry between cut points — reaches 800–1200 mm/s, which shortens non-cutting moves across a 1600×2500mm bed without forcing the knife through a curve faster than the material allows.
The Cost of a Mismatched Configuration
A buyer who selects the table on working area alone may find the oscillating knife stalls on a 15 mm foam gasket because the vacuum zone was specified for full-sheet carton stock rather than small nested parts. Ragged edges on corrugated flutes or crushed foam cores are usually the result of the wrong tool head, not a defective machine [NEED_CITE: tool head selection for material thickness and density]. When the conveyor belt runs but the vacuum cannot hold the trailing edge of a short sheet, the material shifts mid-cut and the entire blank is scrapped. These failures show up during the first production week, long after the installation technician has left the building.
Why Source the RT-D2516/RT-S2516 Here
In-house design and production cover both knife and laser cutting technologies, so a buyer can match the cutting method to the material rather than force one method across every substrate. Tool head and table configuration are specified per material and daily volume, with the oscillating knife, drag knife and creasing wheel options assigned on the same order. CCD camera positioning is available for printed contour work, and software compatibility with the buyer’s existing file format is confirmed before the deposit is paid. Voltage, plug type and control language are locked in during the specification review, eliminating the on-site rework scenario described earlier. Sample cutting on the buyer’s own material is offered before commitment, providing physical evidence of edge quality and cycle time.
Documentation & Verification
- Machine specification sheet listing confirmed tool head and vacuum zone configuration
- Electrical schematic with voltage, frequency and plug type validated for destination market
- Sample cutting report on buyer-supplied corrugated or flexible material showing edge quality
- Factory test record covering repeatability, vacuum hold and conveyor feed accuracy before dispatch
- Operation and maintenance manual with HP-GL file import workflow and nesting guidance
- Spare parts list identifying Swiss blade consumables, vacuum cups and belt wear components
Installation, Commissioning & Support
- Floor space of at least 3450×2300mm plus clearance for the 7.5 kW vacuum pump and material staging
- Dedicated 380V±10% circuit rated for the 11 kW total load with correct breaker sizing
- Table and gantry arrive assembled; vacuum pump and conveyor belt are connected on site
- Servo parameter tuning and vacuum zone mapping performed against the buyer’s primary material
- Operator training covers HP-GL import, tool head changeover and infrared sensor safety routines
- First-set spare blades and vacuum cups shipped inside the crate to cover initial production weeks
Before You Request a Quotation
Send the material type, maximum thickness and typical sheet dimensions so the correct oscillating knife frequency and vacuum zone count can be selected. Confirm the local supply voltage and frequency, the plug standard and the preferred control interface language before the build begins. If your workflow relies on a specific packaging CAD output, provide a sample file so HP-GL compatibility and nesting behavior can be verified on the RT-D2516/RT-S2516 before shipping.
Frequently Asked Questions
Q: How do I choose between an oscillating knife, drag knife and creasing wheel for my materials?
A: Oscillating knives cut thick corrugated board and foam by vibrating the blade, which prevents crushing. Drag knives suit thin vinyl and adhesive films where a pulled blade produces a clean contour. Creasing wheels press fold lines into carton stock without cutting through. The tool head assignment is matched to your primary material during the configuration review and can be swapped as production needs change.
Q: Can the CCD camera track registration marks on printed carton blanks at full speed?
A: The camera reads standard printed marks and feeds positional corrections to the servo drives so the cut path aligns with the printed graphic. Tracking stability depends on mark contrast, lighting and the translational velocity setting. A sample run on your actual printed sheet confirms that the system holds registration within tolerance at your target speed.
Q: Why does vacuum zoning matter when cutting small packaging parts?
A: When a nested sheet leaves large areas of the table uncovered, those open zones leak vacuum and reduce suction where it is needed. Configuring zone valves to match your typical nesting layout keeps hold-down pressure on small carton blanks even during fast gantry moves, preventing material shift and scrap.
Q: Will the machine accept files from my existing packaging CAD software?
A: The HP-GL compatible instruction system imports geometry from most packaging CAD suites used for sample making and short-run carton production. Before the order is finalized, you provide a sample file and we verify import accuracy, layer mapping and nesting behavior on the control software so there are no surprises at commissioning.
Q: What happens if my workshop voltage differs from the standard 380V±10% specification?
A: Voltage, frequency and plug type are confirmed during the specification review and the electrical cabinet is wound accordingly at the factory. If your facility runs on a different supply, we adjust the transformer ratio, breaker rating and servo parameters before the machine ships, avoiding on-site electrical rework and commissioning delays.


商品评价
Clear filtersThere are no reviews yet.