


Fast Shipping
Carrier information

20k products
Payment methods

24/7 Support
Unlimited help desk

2-day Delivery
Track or off orders
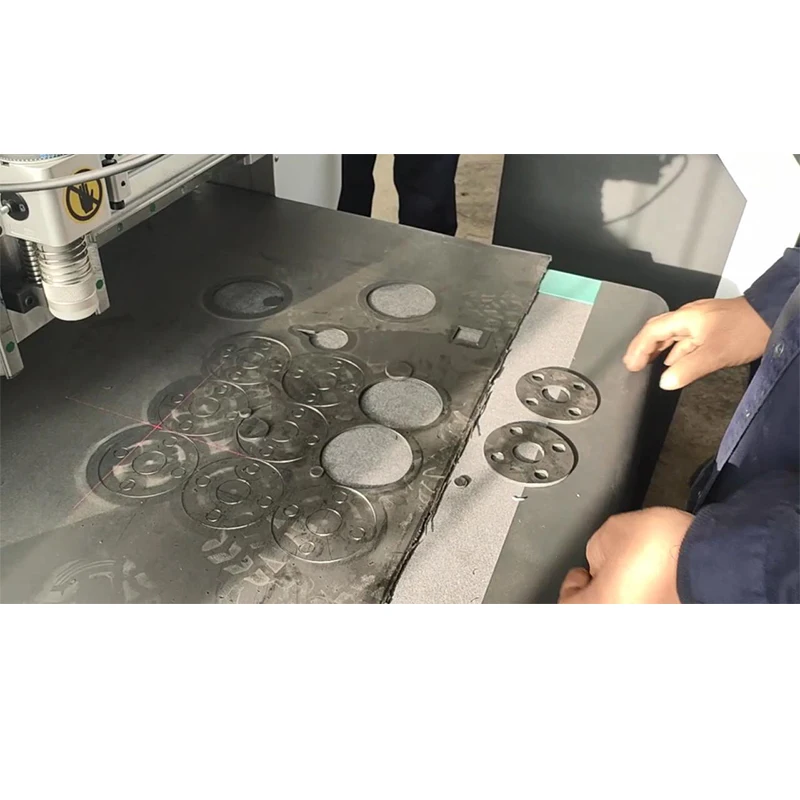
Precision tool matching — Every oscillating knife and drag knife tool head is tested on your specific gasket material before the configuration is locked in.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | RT-D2516/RT-S2516 |
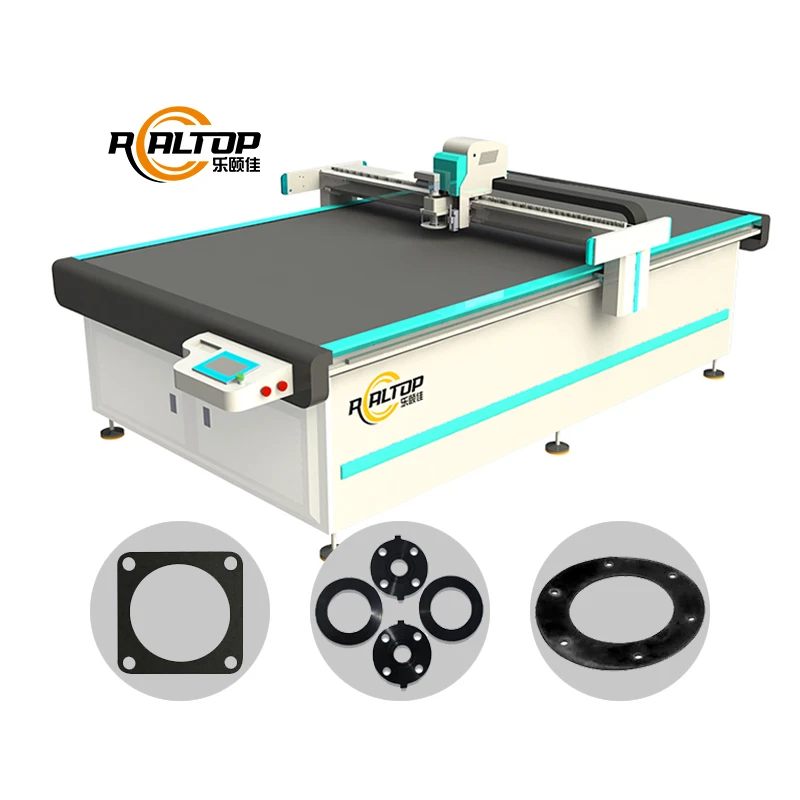
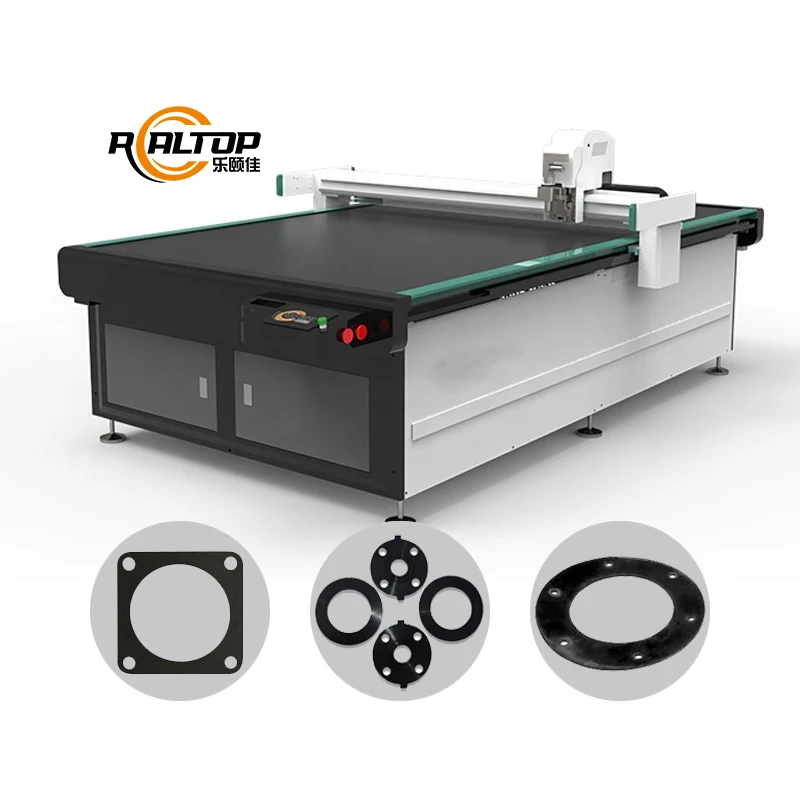
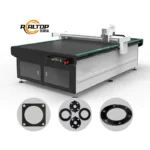
| Product Type | CNC Oscillating Knife Cutting Machine |
| Working Area | 1600 × 2500 mm |
| Machine Size | 3450 × 2300 × 1250 mm |
| Rated Power | 9 kW |
| Table Type | Magnesium-aluminum alloy vacuum adsorption, PVDF powder coated, anodic oxidized |
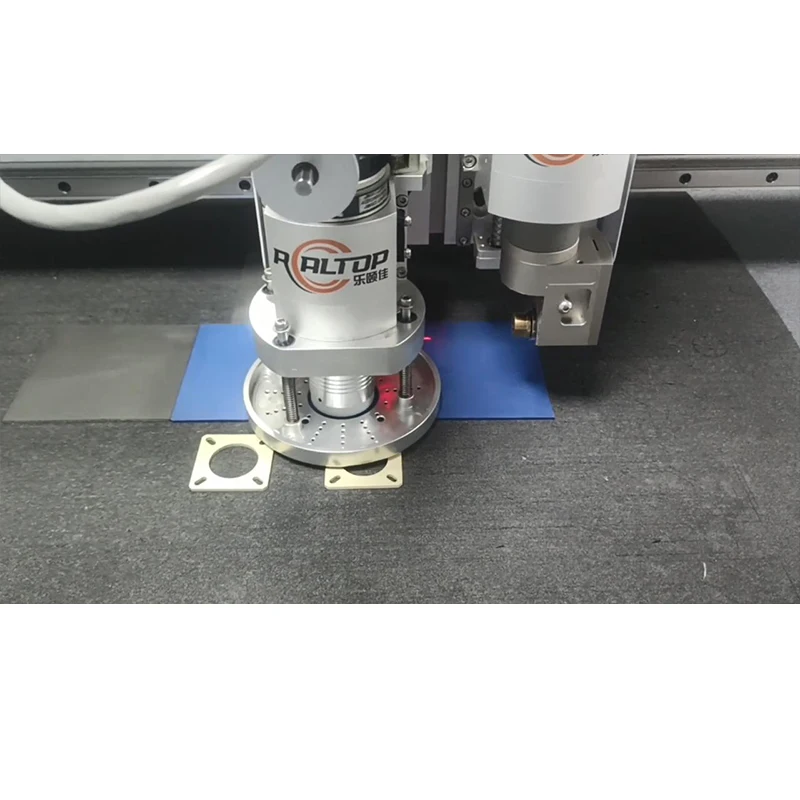
| Multifunctional Head | Swiss imported knife with vibration full cutting, vibration half cutting and cursor location |
| Tool Head Options | Oscillating knife, pneumatic knife, high-power vibrating knife, circular knife, V cutting knife, drag knife, creasing wheel, dotted line knife, punching, brush |
| Visual Positioning | Small CCD camera mark point positioning, panoramic camera recognition, projection positioning |
| Translational Velocity | 800–1200 mm/s |
| Cutting Thickness | 20–80 mm (basis not stated in source — confirm material type and density) |
| Repeated Accuracy | ≤0.1 mm |
| Transmission System | Digital servo motor, linear guide, synchronous belt, ball screw |
| Instruction System | HP-GL compatible format |
| Voltage | 380V ± 10% |
| Servo Motor Brand | Delta (Panasonic optional) |
| Vacuum Pump | 7.5 kW, integrated aviation aluminum shell with built-in silencer sponge |
| Conveyor Belt | Germany imported (source value — verify against manufacturer catalog) |
| Linear Rail | Taiwan Hiwin |
| Safety Device | Infrared induction blocking, anti-collision on both sides of beam, emergency stop button |
| Other Functions | Full size cutting, kiss cutting, slot milling, punching, inkjet, drawing marking |
| Language Options | English, Russian, Italian, Chinese (special languages customizable) |
| Standards | CE declaration where applicable (source value — verify against manufacturer catalog) |
Application Suitability
| Application | Material or Output |
|---|---|
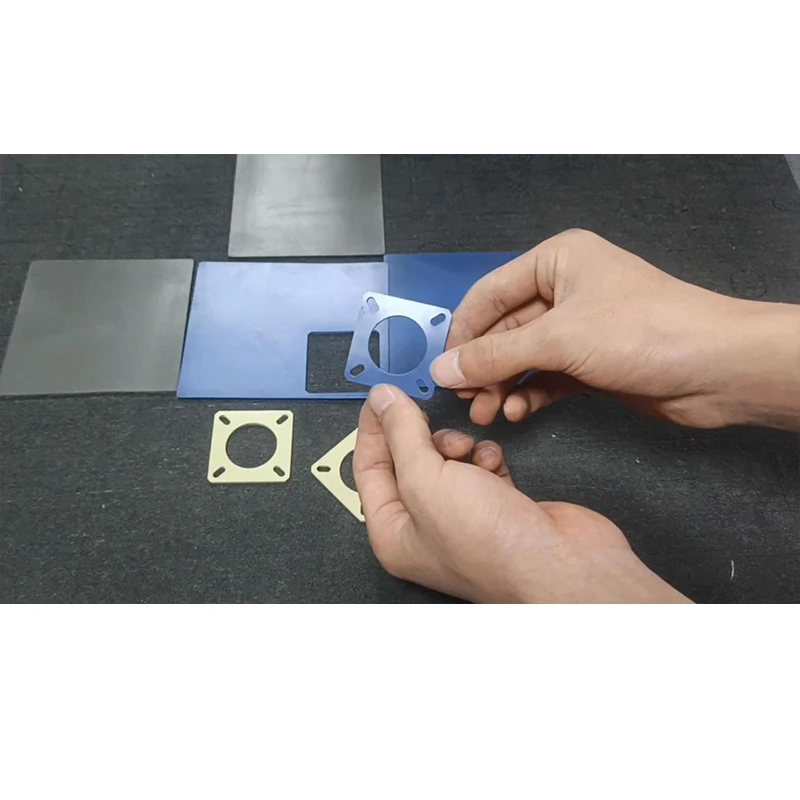
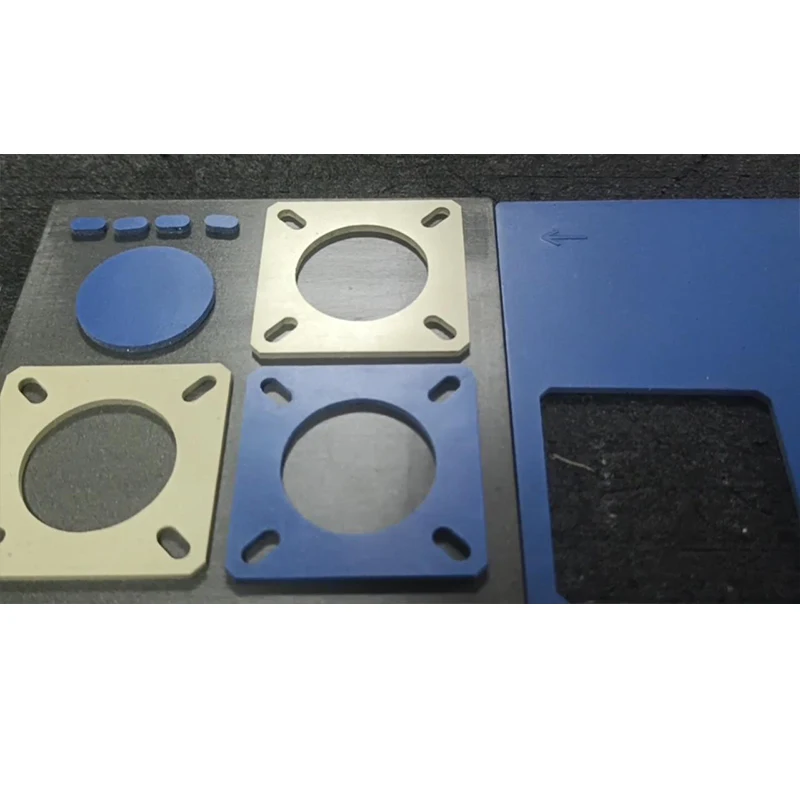
| Gasket and sealing pad production | Rubber, PTFE, silicone, non-asbestos fiber, cork-rubber composite sheets |
| Automotive interior components | PU foam, EVA, sponge composite leather, XPE for dash panels and door trims |
| Packaging and carton sample making | Corrugated cardboard, plastic box stock, sticker film with creasing and kiss-cut |
| Industrial composite fabrication | Fiberglass, PVC foam board, PE and PP sheet stock |
| Footwear and leather goods | Shoe material, luggage material, non-woven fabric, carpet |
Why "20–80 mm Cutting Thickness" Means Almost Nothing Without Your Material
The number on the spec sheet is a range, not a promise — what matters is whether the tool head and downward pressure can actually shear your specific gasket compound cleanly.
I once watched a line stall for two days because the buyer assumed any CNC oscillating knife cutting machine specifications listing 80 mm depth would handle steel-reinforced composite gasket material. The knife simply could not penetrate the wire mesh layer, and the edge on the softer surrounding matrix tore instead of shearing. The cutting thickness figure printed in a brochure reflects a test on one reference material at one density. Your PTFE sheet at 3 mm behaves entirely differently from your 15 mm cork-rubber compound, and neither matches the foam sample the factory used to derive that range. This is why requesting a sample cut on your actual stock is not optional — it is the only way to confirm the CNC oscillating knife cutting machine specifications translate to your production floor [NEED_CITE: gasket material density and compressibility standards for sealing applications].
Tool Head Selection Is Where Gasket Quality Is Won or Lost
The RT-D2516/RT-S2516 carries up to ten interchangeable tool heads, but picking the correct one for gasket and flexible material cutting is not a checkbox exercise. An oscillating knife shears cleanly through compressed non-asbestos fiber and rubber up to moderate thicknesses, while a pneumatic knife delivers the downward force needed for dense cork composites. Drag knives score and kiss-cut thin PTFE and sticker films without dragging the substrate. A high-power vibrating knife handles thicker foam and sponge layers where a standard oscillating blade would stall mid-stroke. The right pairing eliminates ragged edges and delamination at the cut line.
Vacuum Zoning Determines Whether Small Gaskets Stay Flat
The magnesium-aluminum alloy vacuum table on this platform uses PVDF powder coating and anodic oxidation to maintain flatness under repeated loading. But flatness alone does not hold a 30 mm diameter O-ring blank in place while the knife traverses at 1200 mm/s. The table must be zoned so that suction concentrates under small parts rather than bleeding across the full 1600 × 2500 mm surface. When zones are correctly mapped to your typical nest layout, small gasket blanks remain pinned through the final cut. Without that zoning, lightweight PTFE and thin rubber sheets lift at the trailing edge and produce an angled, out-of-tolerance cut [NEED_CITE: vacuum hold-down principles for flatbed digital cutting of flexible materials].
What the Drive System Means for Gasket Dimensional Tolerance
The ≤0.1 mm repeated positioning accuracy comes from the combination of Delta digital servo motors, Taiwan Hiwin linear rails, and ball screw transmission. For gasket producers, this matters because sealing performance depends on bolt-hole patterns and flange contours holding within tight bands across long production runs. A synchronous belt drive alone can introduce cumulative positional drift over a 2500 mm stroke; the ball screw and linear guide combination resists that drift. The HP-GL compatible instruction system accepts nesting files directly from most CAD outputs used in gasket design, reducing translation errors between your design office and the machine controller.
The Hidden Cost of Skipping Material-Specific Configuration
Buyers who specify a flatbed cutting table by working area alone, without confirming tool head pressure and vacuum zone layout against their material, discover the problem only after the machine arrives. Ragged edges on rubber gaskets mean every piece needs manual trimming. Crushed foam on automotive interior blanks means the composite delaminates before it reaches the assembly line. A CCD camera promised for contour recognition may fail to track printed registration marks if the print contrast on your specific gasket sheet stock is below the sensor threshold. These are not warranty claims — they are specification mismatches that delay production startup [NEED_CITE: common flatbed cutting machine commissioning delays due to material mismatch].
Why Source This Platform Through Realtop
In-house design covers both the knife cutting head mechanics and the vacuum table engineering, so the tool head and hold-down system are matched to your material as one package rather than sourced separately. Sample cutting on your own gasket stock is completed before the order is finalized, with a written report documenting edge quality, cutting speed, and dimensional accuracy on your exact material. Voltage, plug type, and control language are confirmed against your facility requirements before production begins, not assumed from a default build. The CCD camera positioning system is calibrated to your print mark specification so contour accuracy is verified before shipment. Software compatibility with your existing nesting workflow and file format is validated during the pre-order stage.
Documentation & Verification
- Machine specification sheet listing the exact tool head and vacuum zone configuration confirmed for your material
- Electrical schematic and voltage confirmation matched to your facility power supply before production
- Sample cutting report on your gasket material with edge quality photos and dimensional measurements
- Factory test record documenting repeated accuracy and cutting performance before dispatch
- Software licence and file format compatibility note confirming HP-GL and your nesting workflow integration
- Spare parts list covering knives, vacuum seals, and wear items specific to your tool head configuration
Installation, Commissioning & Support
- The 9 kW rated power and 7.5 kW vacuum pump require a dedicated 380V ± 10% circuit with appropriate breaker rating
- Machine footprint of 3450 × 2300 mm needs level concrete flooring with clearance for beam travel and material loading
- Fully assembled delivery means the unit is positioned and powered on-site without major mechanical assembly
- First-run commissioning includes tool head pressure calibration and vacuum zone mapping to your gasket nest layout
- Operator training covers tool changeover procedures across all configured heads and CCD camera mark registration
- Daily maintenance focuses on knife blade inspection, vacuum filter cleaning, and linear rail lubrication per the Hiwin schedule
What We Need to Move Your Inquiry Forward
Send your gasket material type, thickness range, and typical sheet dimensions so the correct tool head and vacuum zoning layout can be specified. Confirm your local voltage and frequency, and let us know the control language your operators require. If you run an existing nesting software, share the file format so we verify compatibility with the HP-GL instruction system before quotation. Providing a sample of your actual gasket stock allows us to run a cutting test and return a report with edge quality and dimensional data tied to your material.
Frequently Asked Questions
Q: Which tool head cuts clean edges on PTFE versus rubber gasket material?
A: PTFE is dense and tends to deform under lateral blade pressure, so a drag knife or a high-frequency oscillating knife at shallow penetration typically produces the cleanest edge. Rubber, especially softer compounds, responds better to a standard oscillating knife that shears rather than drags. The RT-D2516/RT-S2516 supports both, and the correct choice is confirmed by a sample cut on your specific compound and thickness.
Q: Why does the 20–80 mm cutting thickness range depend on material density?
A: The range reflects tests on reference materials at specific densities. A 60 mm thick low-density EVA foam cuts easily with a high-power vibrating knife, but a 10 mm steel-reinforced composite gasket may exceed the downward force any knife head on this platform can deliver. Always verify the cutting depth capability against your material’s actual density and tensile structure through a sample cutting report before committing to a configuration.
Q: How is voltage and control language confirmed before shipment?
A: The standard build runs on 380V ± 10% with Delta servo motors. If your facility operates on a different voltage or frequency, the transformer and motor specification must be adjusted during production, not after arrival. Control language — available in English, Russian, Italian, Chinese, or by custom request — is loaded onto the controller before the machine leaves the factory. Both items are locked in at the specification confirmation stage of your order.
Q: Can the CCD camera track printed marks on my gasket material at production speed?
A: The system offers small CCD mark point positioning and panoramic camera recognition. Tracking reliability at the 800–1200 mm/s translational velocity range depends on print contrast, mark size, and surface reflectivity of your specific gasket sheet. Dark marks on light stock track reliably; low-contrast or metallic-surface materials may require adjusted lighting or reduced speed. This is validated during the sample cutting stage using your printed material.
Q: What does the sample cutting process involve and how does it affect configuration?
A: You send a representative sample of your gasket material, including any printed registration marks if contour cutting is required. The factory runs test cuts using multiple tool heads and documents edge quality, cutting speed, and dimensional accuracy. The results determine which tool heads are included in your final configuration, how vacuum zones are mapped, and whether any standard specifications need adjustment before your machine enters production.


商品评价
Clear filtersThere are no reviews yet.