



Fast Shipping
Carrier information

20k products
Payment methods

24/7 Support
Unlimited help desk

2-day Delivery
Track or off orders
Custom Tool Head Matching — Each oscillating, driven rotary, creasing or kiss cutting tool is selected after sample runs on the buyer’s actual fabric, foam or board stock, not assigned by catalogue default.
Technical Specifications
| Parameter | Value |
|---|---|
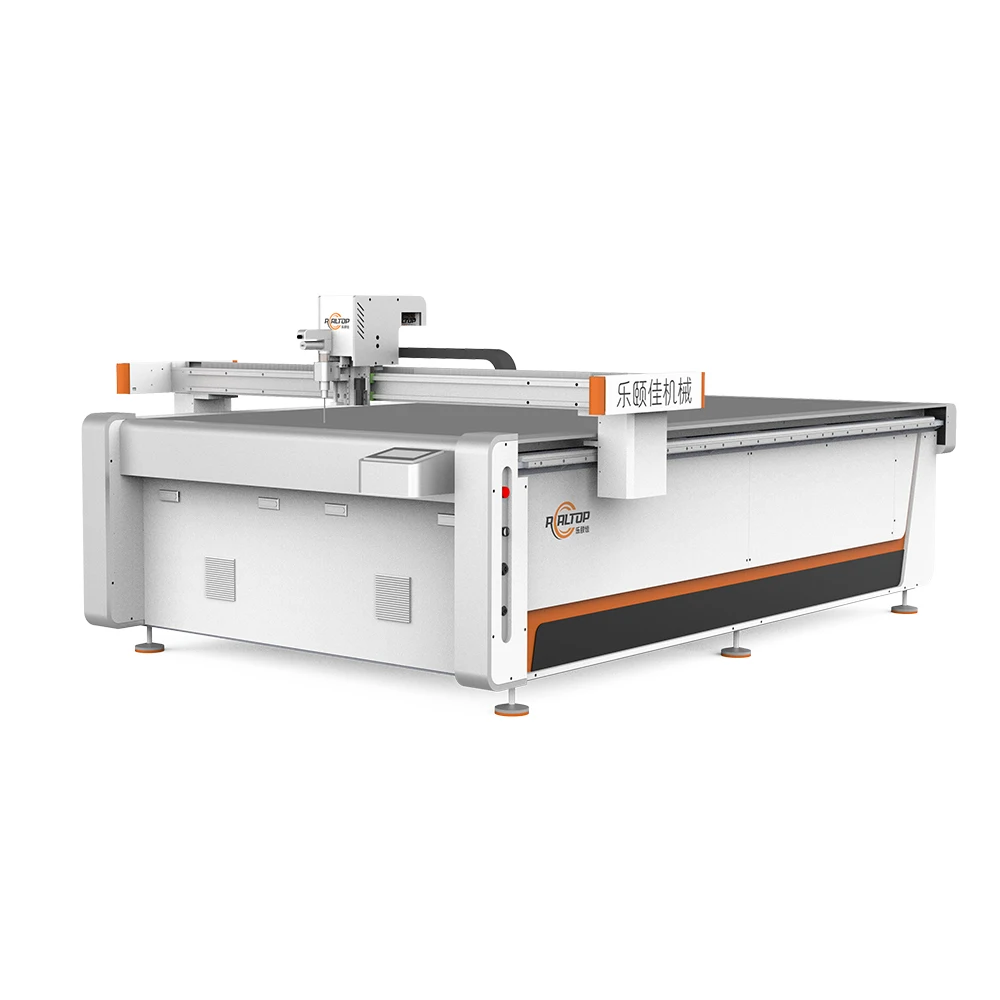
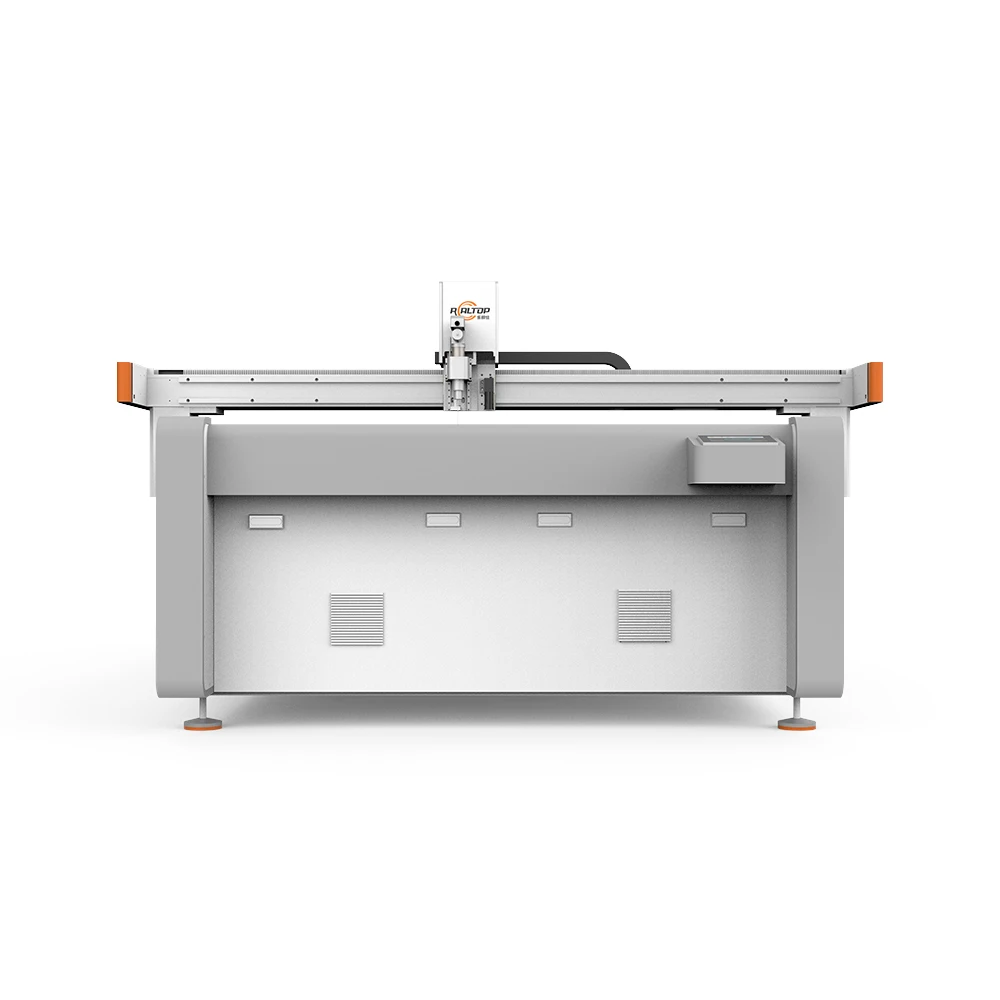
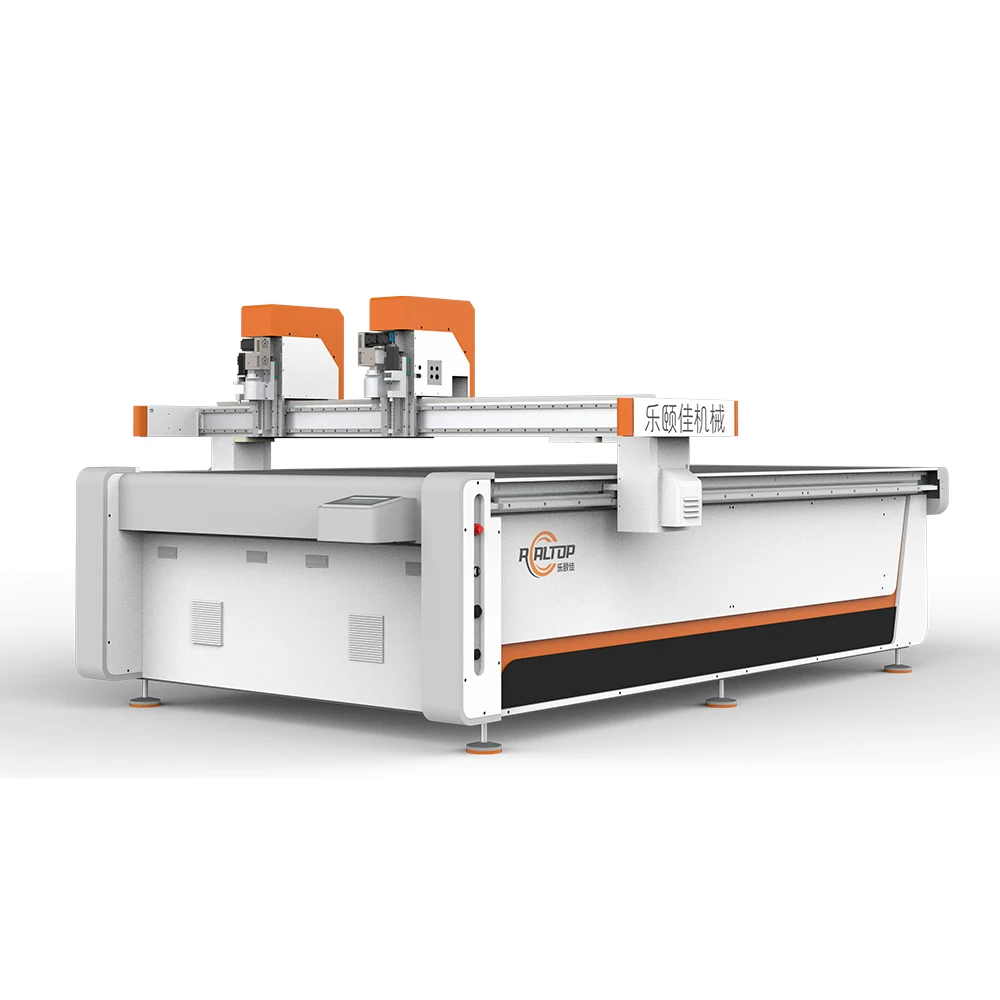
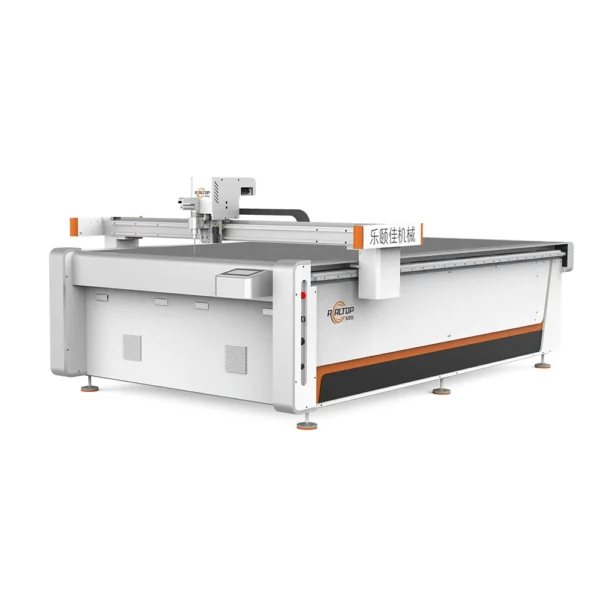
| Product Type | CNC Oscillating Knife Cutting Machine |
| Model | 1625 |
| Working Area | 1600 × 2500 mm |
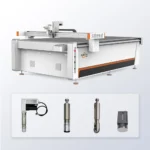
| Tool Head Options | Oscillating knife, Driven rotary knife, Creasing wheel, Kiss cutting tool, Pneumatic knife, Milling tool, V groove knife |
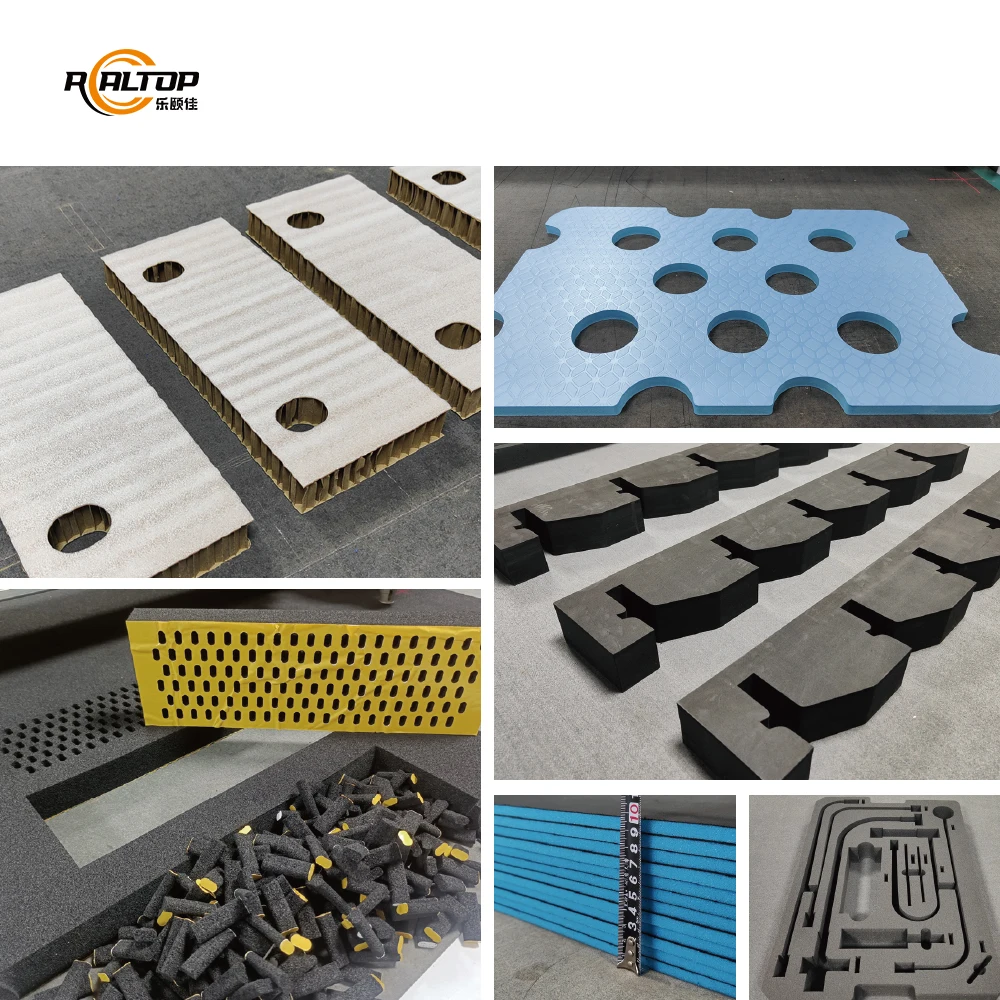
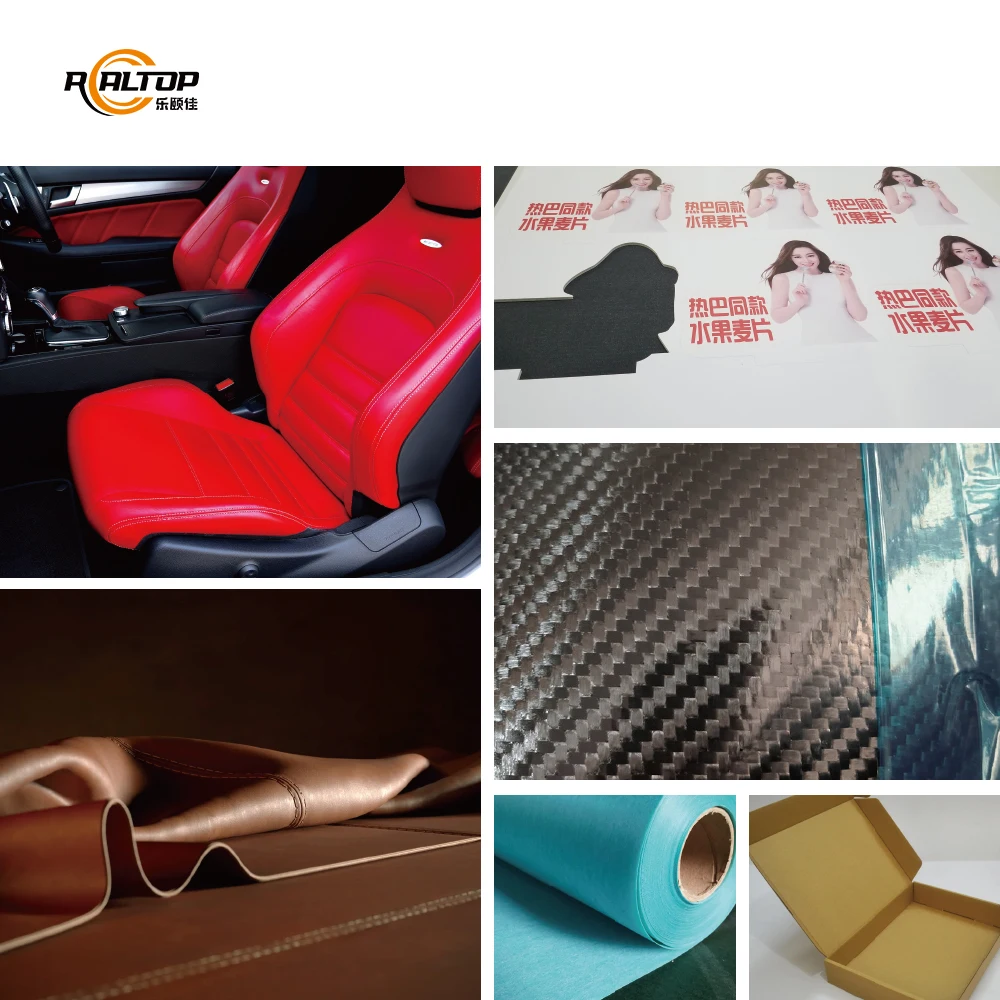
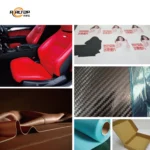
| Applicable Materials | Fabric, Cardboard, Carton, Mats, PVC, EVA, Leather, Acrylic, Foam, PTFE, Rubber |
| Cutting Speed | 0–2000 mm/s |
| Cutting Thickness | ≤ 30 mm (basis not stated in source — confirm material type and density) |
| Cutting Accuracy | ±0.1 mm |
| Vacuum Pump | 9 kW |
| Vacuum Table | Aluminum bellows vacuum table |
| Control System | PLC control panel |
| Software | Dedicated packaging box structure design software |
| Servo Motors | Panasonic, Delta, Dorna (multiple options) |
| Profile Formats | PLT, DXF, AI, PDF |
| Voltage Options | 110V, 220V, 380V |
| Safety Devices | Infrared sensor device and emergency stop device |
| Machine Size | 3300 × 2100 × 1350 mm |
| Language Options | English, Russian, Italian, Chinese (special languages customizable) |
Application Suitability
| Application | Material or Output |
|---|---|
| Packaging and carton sample making | Corrugated cardboard, grey board, folding carton stock with creasing and kiss cutting |
| Automotive interior trimming | Acoustic felt, damping pads, seat foam, sealing strips, headliner fabrics |
| Gasket and seal production | Rubber, PTFE, EVA foam sheets cut to precise tolerance |
| Textile and leather cutting | Upholstery fabric, garment layers, synthetic leather for footwear and bags |
| Composite and foam fabrication | PVC foam core, EVA mats, insulation foam panels up to stated thickness capacity |
Why the Wrong Tool Head Wastes More Material Than You Expect
A CNC oscillating knife cutting machine tool head selection mistake rarely shows up on the first straight cut — it reveals itself on the third curve, when compressed foam springs back or a corrugated flute crushes instead of shearing.
The blade angle, oscillation frequency and stroke length must match material density and recovery behaviour, not just thickness.
I once watched a line of automotive seat packaging inner pads come off the table with ragged edges because the oscillation amplitude was set for low-density EPE while the stock was high-density memory foam. The blade could not penetrate cleanly, and the entire batch of inserts had to be scrapped. Before any production run starts, three test cuts on the buyer’s actual material remain the only reliable way to confirm the tool head and parameter match. [NEED_CITE: material compression recovery behaviour during oscillating knife cutting]
Matching Tool Geometry to Material Behaviour
The 1625 platform supports interchangeable heads — oscillating knife, driven rotary, pneumatic knife, creasing wheel, kiss cutting tool, milling and V groove knife — because no single blade geometry cuts foam, corrugated board and PTFE with equal edge quality. Oscillating action suits compressible stock like sponge and acoustic felt where drag knives would drag and tear. Driven rotary tools handle dense woven textiles at production speed without fraying. Creasing wheels and kiss cutting tools serve packaging sample iteration where the board must fold cleanly without through-cutting. CNC knife cutting table vacuum zoning pairs with these heads to hold small gasket or label parts flat so the blade does not push them off position during contour cuts.
Holding the Workpiece Without Crushing It
The aluminum bellows vacuum table provides full-surface adsorption across the 1600 × 2500 mm working area with enough flatness tolerance to keep thin films and thin foam from buckling under the cutting head. The 9 kW vacuum pump delivers the suction required for heavy corrugated sheets and dense composite panels. Zoned vacuum control matters most when the nesting layout mixes large panel outlines with small offcut parts — insufficient hold on small pieces causes lift, blade deflection and scrapped sections. [NEED_CITE: vacuum hold-down requirements for CNC flatbed cutting of flexible materials]
Reading the Specification Sheet Against Your Production Reality
Cutting speed reaches 0–2000 mm/s, but usable speed on any given material depends on thickness, density and contour complexity — a tight corner on 20 mm EVA foam demands a slower feed than a straight rip on 2 mm cardboard. The ±0.1 mm cutting accuracy specification governs repeatability across long production runs, which matters for packaging die-lines and gasket profiles that must stack or mate precisely. The dedicated packaging box structure design software imports PLT, DXF, AI and PDF formats, so sample makers can iterate structural designs without re-drawing files in a separate CAD package. Servo motor selection from Panasonic, Delta or Dorna lets buyers align drive components with their existing maintenance inventory and local service support.
The Hidden Cost of Skipping Configuration Verification
When a machine arrives with a generic tool head and the buyer’s material is outside the default range, production stalls while replacement blades and holders are sourced — sometimes across borders. Voltage mismatches surface later, when a 380V motor is connected to a 220V supply without prior confirmation, damaging the drive on first start-up. Software incompatibility appears when the buyer’s nesting workflow outputs a file format the dedicated software cannot import, forcing manual re-drawing of every die-line. [NEED_CITE: industrial machine electrical specification verification before export shipment]
Why Buyers Source This Configuration Here
In-house design covers both knife and laser cutting processes, so the buyer can choose the method that suits the material rather than being pushed toward whichever technology the supplier happens to stock. Every tool head, blade type and vacuum zone configuration is documented against the buyer’s specific material before order confirmation. Sample cutting on the buyer’s own stock — with a written report on edge quality and thickness performance — runs before any commitment is made. Voltage, plug type and control panel language are confirmed and locked before the machine leaves the factory. The design team handles custom language additions for the PLC interface when standard English, Russian, Italian or Chinese does not cover the operator’s requirements.
Documentation & Verification
- Machine specification sheet listing confirmed tool head, blade angle and vacuum table zone layout for your material
- Electrical schematic and voltage confirmation document matching your facility supply before dispatch
- Sample cutting report on your actual fabric, foam or board stock with edge quality photographs
- Tool head and table configuration list detailing every interchangeable component shipped with the machine
- Software licence documentation with file format compatibility note for your nesting workflow
- Factory test record showing cutting accuracy verification on your specified material profile
Installation, Commissioning & Support
- Foundation must be level and rigid to support the 3300 × 2100 × 1350 mm machine footprint without flexing the aluminum bellows vacuum table
- Dedicated electrical circuit matching confirmed voltage (110V, 220V or 380V) with correct plug type and phase configuration
- Machine ships partially assembled; table frame and gantry require on-site alignment and belt tensioning
- First-run commissioning includes parameter tuning for your specific material thickness and contour complexity
- Operator training covers PLC control panel navigation, tool head changeover and software file import in the confirmed language
- Spare parts list includes oscillating blades, rotary knives, creasing wheels and vacuum table seals sized for your configuration
Before You Request a Quotation
Send the material type, thickness range, sheet dimensions and daily cutting volume so the correct tool head and vacuum table zoning can be specified from the start. Confirm your local voltage, frequency, plug standard and preferred control panel language to avoid electrical mismatches at delivery. If you have an existing nesting workflow, share a sample output file so software compatibility is verified before order placement rather than on the factory floor.
Frequently Asked Questions
Q: How is the correct tool head and blade type chosen for my specific material and thickness?
A: The tool head — oscillating knife, driven rotary, creasing wheel or another option — is selected based on your material’s density, recovery behaviour and edge quality requirement. Sample cuts on your actual stock confirm the match before the order is finalised, so the blade angle and oscillation parameters are documented rather than guessed.
Q: Can the vacuum table zoning be configured for small parts that tend to lift during cutting?
A: Yes. The aluminum bellows vacuum table on the 1625 supports zoned suction so small gasket pieces or packaging offcuts receive concentrated hold-down force. Zone layout is planned around your typical nesting pattern and confirmed during the sample cutting stage.
Q: What file formats does the software import, and is my existing nesting workflow compatible?
A: The dedicated packaging box structure design software imports PLT, DXF, AI and PDF profiles. Before order, you share a sample file from your nesting workflow and the software team confirms compatibility or identifies any conversion steps needed.
Q: How are voltage, plug type and control panel language confirmed before shipment?
A: An electrical schematic and voltage confirmation document is prepared with your facility specifications and signed off before production. Control panel language — from the standard English, Russian, Italian and Chinese options or a custom addition — is locked at the same stage.
Q: Can I send my material for sample cutting to verify edge quality and thickness capacity before ordering?
A: Yes. You send a representative sample of your fabric, foam, board or composite stock, and test cuts are run with the proposed tool head configuration. A written sample cutting report with edge quality photographs is returned to you before any purchase commitment is required.


商品评价
Clear filtersThere are no reviews yet.