







Fast Shipping
Carrier information

20k products
Payment methods

24/7 Support
Unlimited help desk

2-day Delivery
Track or off orders
Tool head selection per material — oscillating knife, creasing wheel and V-groove configured against your actual corrugated flute or foam sample before the order is locked in.
Technical Specifications
| Parameter | Value |
|---|---|
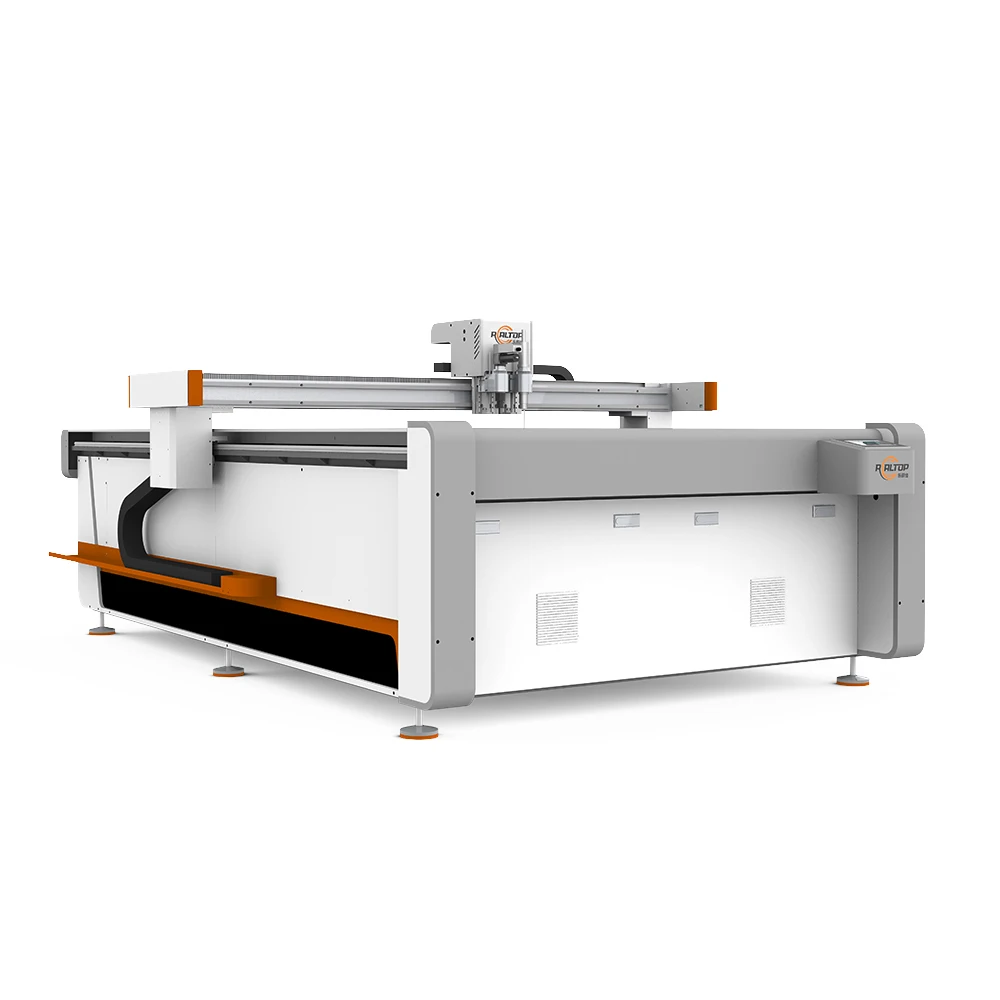
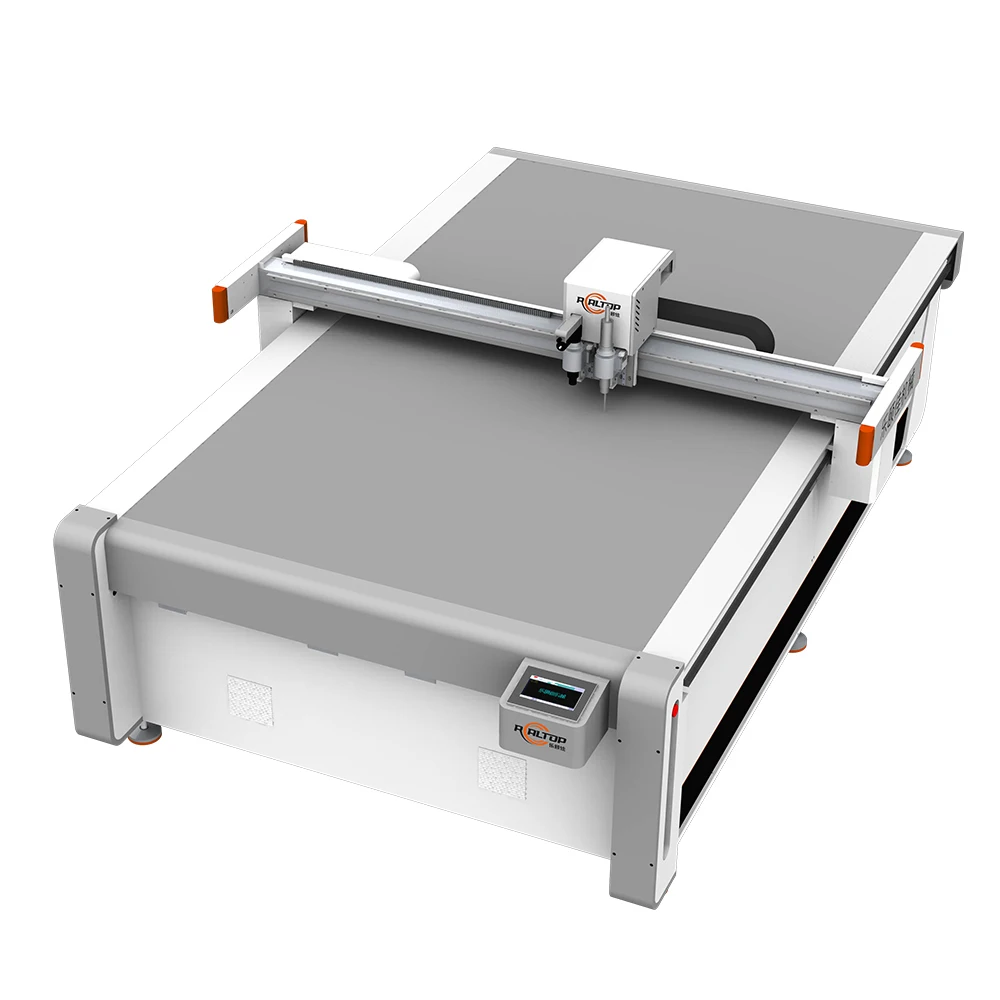
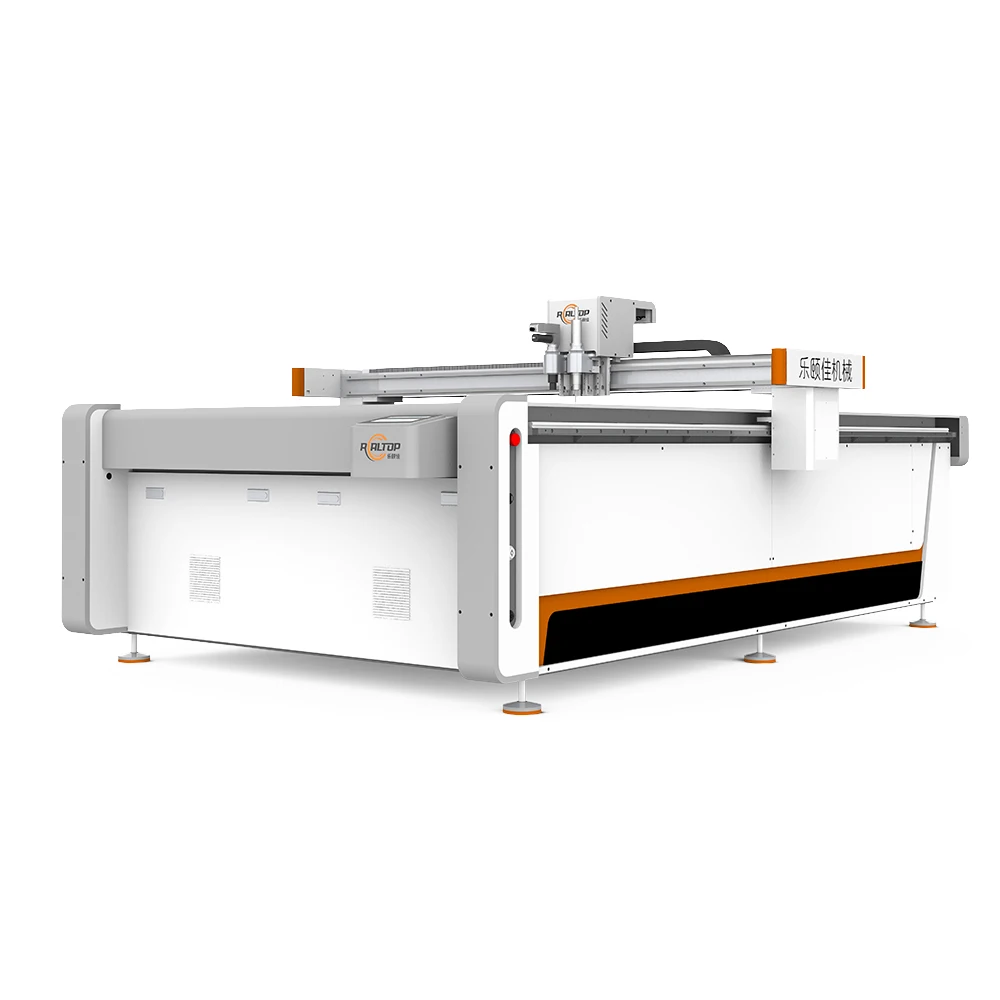
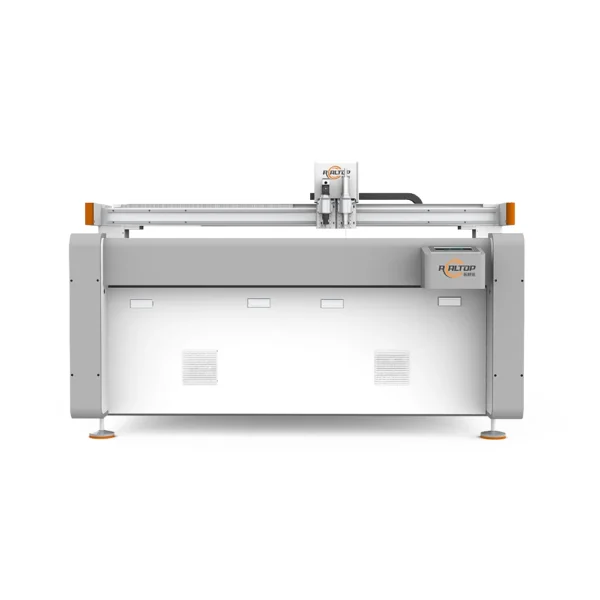
| Product Type | CNC Flatbed Oscillating Knife Cutting Machine |
| Model | 1625(std.) |
| Working Area | 1600 × 2500 mm |
| Tool Head Options | Oscillating knife, Driven rotary knife, Creasing wheel, Kiss cutting tool, Pneumatic knife, Milling tool, V-groove knife |
| Cutting Thickness | Up to 40 mm |
| Cutting Speed | 0–1500 mm/s |
| Cutting Accuracy | ±0.1 mm |
| Vacuum Table | Aluminum bellows vacuum table |
| Vacuum Pump Power | 9 kW |
| Servo Motor Options | Panasonic, Delta, Dorna |
| Control System | PLC control panel with dedicated packaging box structure design software |
| File Format Compatibility | PLT, DXF, AI, PDF |
| Voltage Options | 110V, 220V, 380V |
| Software Language Options | English, Russian, Italian, Chinese, customizable |
| Safety Devices | Infrared sensor, emergency stop |
| Machine Dimensions | 3300 × 2100 × 1350 mm |
| Certification | CE |
Application Suitability
| Application | Material or Output |
|---|---|
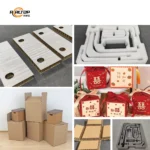
| Packaging sample making | E-flute, B-flute, BC-flute corrugated board without die molds |
| Corrugated carton short-run production | Greyboard, art paper, single and double-wall corrugated |
| Foam insert fabrication | EVA, EPE, PU protective packaging inserts |
| Gasket and seal cutting | Rubber, PTFE, non-woven fabric |
| Thin plastic sheet processing | PVC, PET, acrylic, synthetic leather |
Why "Working Area 1600×2500" Is Not Enough to Specify a CNC Oscillating Knife Cutting Machine
A flatbed size tells you nothing about whether the tool head can actually cut your flute without crushing the core.
I have walked into packaging workshops where the machine sat idle because the oscillating knife frequency was wrong for the flute pitch, leaving ragged edges on B-flute and collapsed walls on BC-flute. The buyer chose on table size alone and skipped the tool head conversation entirely. A machine that cuts greyboard cleanly at 2 mm may smear and drag through 12 mm EVA foam if the knife stroke and amplitude are not matched to the material density [NEED_CITE: oscillating knife frequency and stroke amplitude matching for corrugated and foam substrates]. Voltage mismatch after arrival is the second silent killer — a 380V unit shipped to a 220V single-phase workshop sits in the corner until an electrician rewires the whole panel.
Tool Head Configuration by Flute Type and Foam Density
Corrugated board demands a different knife profile and oscillation rate than foam or rubber. The 1625 platform offers oscillating knife, driven rotary knife, creasing wheel, kiss cutting, pneumatic knife, milling and V-groove heads, each selected after a sample run on the buyer’s own material. A CNC Oscillating Knife Cutting Machine configured for E-flute carton sample making will use a different blade geometry and stroke setting than one set up for 30 mm EVA insert cutting. Switching between materials in a mixed-production environment means specifying quick-change tool mounts and saving blade profiles in the PLC software so operators do not re-calibrate from scratch each shift.
Vacuum Zoning for Small Packaging Parts
The aluminum bellows vacuum table paired with the 9 kW pump is designed to hold small, lightweight carton sample pieces flat during cutting. Without adequate zoned suction, a 50 mm gusset or a narrow crease line lifts off the table mid-cut, producing dimensional error and wasting material [NEED_CITE: vacuum hold-down requirements for small-format dieless cutting]. The table zoning must be confirmed against the buyer’s typical part nesting layout before the machine leaves the factory, not discovered on the first production day.
Reading the Specification Sheet Beyond the Headline Numbers
The ±0.1 mm cutting accuracy is achievable when the servo system, vacuum hold-down and material flatness all work together. Servo options across Panasonic, Delta and Dorna let the buyer match motion control to their maintenance ecosystem — choosing a servo brand already supported locally reduces downtime when a drive fails. The PLC control panel with dedicated packaging box structure design software means the machine is not running generic nesting software forced into a packaging workflow; it is built for box structures from the ground up. File compatibility with PLT, DXF, AI and PDF covers most packaging CAD exports, but the exact file version and nesting behavior must be verified against the buyer’s existing design software before the purchase order is signed [NEED_CITE: CAD file version compatibility between packaging design software and CNC cutting controllers]. Cutting speed up to 1500 mm/s is the traverse rate on straight runs; actual throughput on a nested sheet depends on corner count, tool changes between cutting and creasing, and material thickness.
The Cost of Skipping the Sample Cut
When a buyer confirms an order based on a brochure cutting thickness figure and the material is slightly denser or more abrasive than the test standard, the blade wears prematurely and edge quality degrades across the production run. I have seen a workshop cutting KT-board laminate on a head specified for corrugated flute — the result was delamination, edge burrs, and throughput dropping to roughly half the expected rate [NEED_CITE: material density and abrasiveness impact on oscillating knife blade life]. That machine was not defective; it was specified wrong. The fix was a different tool head and a revised vacuum zone map, both of which could have been caught with a sample cut before shipment.
Why Source This Machine From the Jinan Factory
The design team covers both knife cutting and laser cutting technologies under one roof, so the cutting method is matched to the material rather than forcing every job through one process. Tool head and table configuration is specified per material and production volume with a written configuration list before production starts. CCD camera positioning is available for printed contour work on packaging prototypes that require optical registration. Software compatibility is confirmed against the buyer’s file format and nesting workflow before the order is finalized, not after the machine arrives. Sample cutting on the buyer’s own corrugated board, foam or composite material is conducted and documented before commitment, with a cutting report included in the shipping documentation.
Documentation & Verification
- Machine specification sheet with confirmed tool head and vacuum zone map
- Electrical schematic with voltage and plug type matched to destination
- Tool head and table configuration list signed off before production
- Sample cutting report on buyer-supplied corrugated or foam material
- Software licence and file format compatibility note for packaging CAD
- Spare parts list with blade, creasing wheel and vacuum cup part numbers
Installation, Commissioning & Support
- Floor space of 3300 × 2100 mm with clearance for material loading on three sides
- Dedicated circuit matching confirmed voltage (110V, 220V or 380V) with correct breaker rating for the 9 kW pump
- Machine arrives assembled; leveling and vacuum seal check performed on-site
- PLC parameter tuning and tool head calibration during first-run commissioning
- Operator training on packaging structure software and tool change procedure
- Consumable blade and creasing wheel stock recommended for first three months
What to Prepare Before Requesting a Quote
Send the actual material you intend to cut — corrugated flute type and thickness, foam density, or composite layup — along with a typical DXF or AI packaging structure file. Specify your workshop voltage and phase, the control language your operators need, and your daily volume so the tool head and vacuum zoning can be sized correctly. If you already run packaging CAD software, confirm the file version so compatibility is verified before the order is placed.
Frequently Asked Questions
Q: Which tool head should I use for my specific corrugated flute type and thickness?
A: E-flute, B-flute and BC-flute each require a different oscillating knife blade geometry and stroke setting. The correct head is determined by a sample cut on your actual board, not by a generic thickness chart. We test your material before confirming the tool head configuration.
Q: How does vacuum table zoning prevent small packaging parts from lifting?
A: The aluminum bellows table is divided into zones so suction concentrates where small parts are nested. A 9 kW pump provides the airflow, but the zone map must match your typical nesting layout. We confirm the zoning against your part mix before shipment.
Q: Can the software import my existing DXF or AI packaging structure files?
A: The PLC control software accepts PLT, DXF, AI and PDF formats, but file version and layer structure vary between CAD platforms. We run your actual files through the software before the order is finalized to confirm clean import and correct crease-cut separation.
Q: What cutting speed should I expect on multi-ply BC-flute board?
A: The 1500 mm/s figure is the maximum traverse rate on straight cuts. Real throughput on BC-flute depends on corner density, tool changes between cutting and creasing passes, and the number of nested parts per sheet. A sample run on your board gives a realistic cycle time.
Q: How do I verify cutting accuracy on my material before committing?
A: We cut your supplied material on the 1625 and measure dimensional deviation against your drawing tolerances. The sample cutting report documents accuracy, edge quality and tool head settings, so you review actual results before the purchase order is signed.


商品评价
Clear filtersThere are no reviews yet.